Understanding the working principle and features of pneumatic conveying equipment is crucial for industries dealing with sintered dust materials. This equipment is designed to efficiently transport fine powders and dust-like substances, ensuring reliable and safe material handling in various industrial applications.
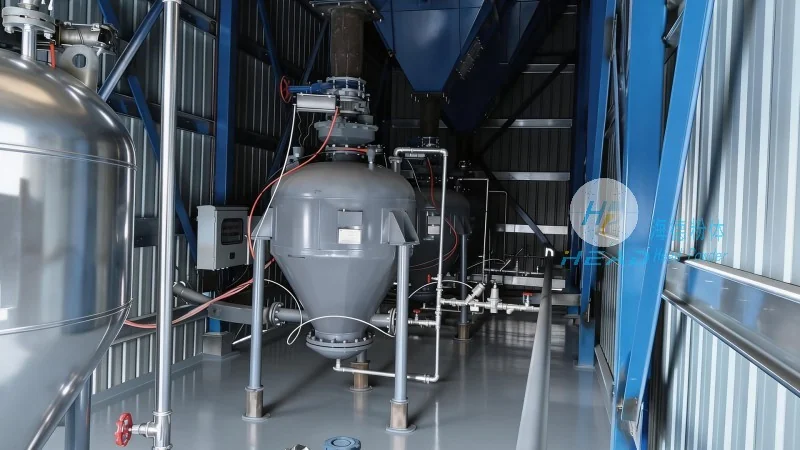
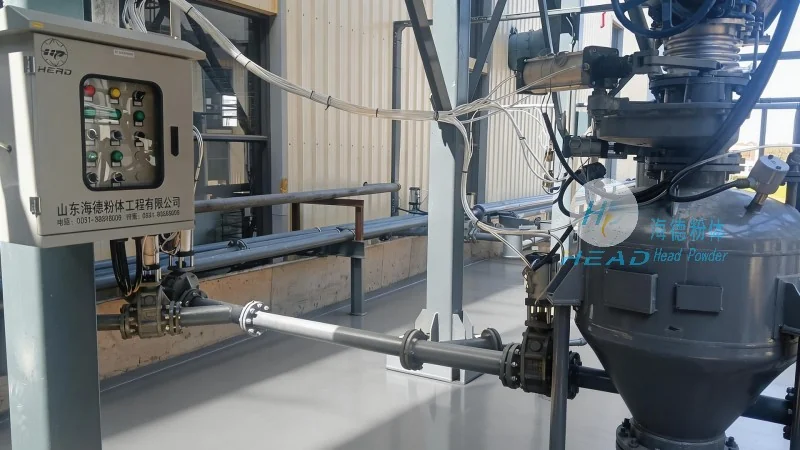
The core of pneumatic conveying for sintered dust materials involves the use of air or gas as the transport medium. The system typically operates by creating a pressure differential or using vacuum to move the material through a pipeline. There are two main types of pneumatic conveying: pressure and vacuum systems. In pressure systems, compressed air is used to push the material forward, while vacuum systems use suction to draw the material into the pipeline. For sintered dust, which often has fine particles and can be prone to clogging, specialized designs such as dilute phase or dense phase conveying are employed to ensure smooth and efficient transport. The process begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. The air flow, controlled by a blower or compressor, carries the dust particles through the pipeline to the destination point, such as a storage silo or processing unit. The design of the conveying line, including the diameter, length, and bends, is critical to maintaining the air velocity necessary to prevent particle deposition and ensure consistent flow.
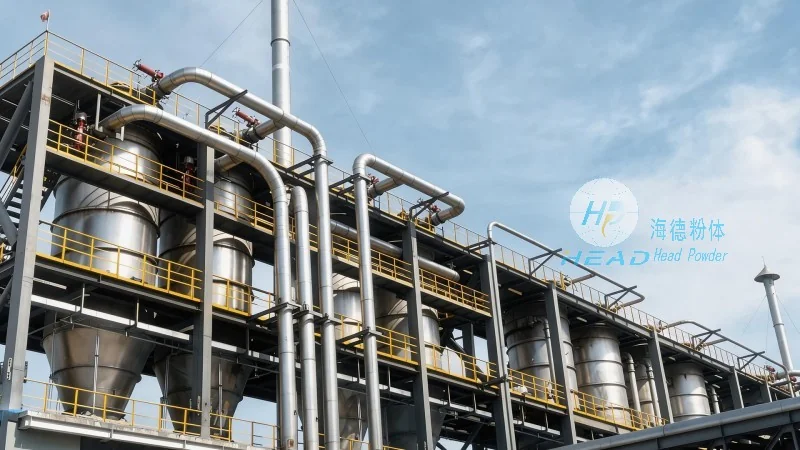
Several key features make pneumatic conveying equipment suitable for handling sintered dust materials. First, the equipment offers a dust-free and enclosed transport process, which is essential for maintaining environmental standards and worker safety. Unlike mechanical conveying methods, such as belt or screw conveyors, pneumatic systems prevent dust emissions, reducing the risk of contamination and health hazards. Second, the flexibility of the system allows for easy integration into existing industrial setups. The conveying lines can be configured in various shapes and lengths to accommodate different plant layouts, making it adaptable to diverse production environments. Third, the equipment provides high efficiency in material transport, with minimal downtime due to maintenance. The use of air as the transport medium reduces the need for mechanical parts that are prone to wear and tear, resulting in lower operational costs and longer equipment lifespan. Additionally, the system can handle a wide range of particle sizes and moisture content, making it versatile for different types of sintered dust. The control systems, often equipped with sensors and automation, allow for precise regulation of air flow and material feed, ensuring consistent performance and preventing overloading or underloading of the conveying line. Another important feature is the ability to transport materials over long distances without the need for intermediate storage or transfer points, which simplifies the overall material handling process and improves operational efficiency.
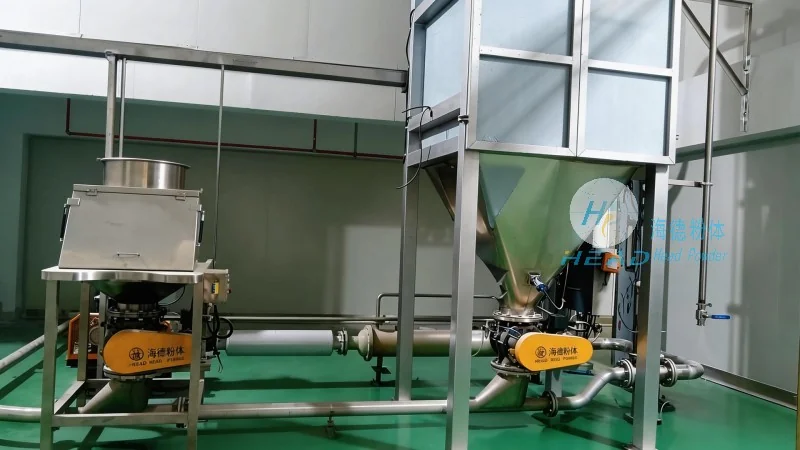
Pneumatic conveying equipment for sintered dust materials finds extensive applications in various industries, including steel production, cement manufacturing, and chemical processing. In steel plants, for example, sintered dust is a byproduct of the sintering process and needs to be transported to storage or further processing units. The use of pneumatic conveyors ensures that this fine material is handled safely and efficiently, without the risk of dust dispersion. In cement plants, the conveying of raw materials and finished products is critical, and pneumatic systems provide a reliable solution for transporting cement powders and other dust-like substances. The benefits of using such equipment extend beyond just material transport; they also contribute to improved workplace safety and compliance with environmental regulations. By eliminating the need for manual handling of dust-laden materials, the equipment reduces the risk of respiratory illnesses and other health issues among workers. Furthermore, the enclosed nature of the system helps in maintaining the quality of the sintered dust, as it is protected from contamination and moisture during transport. The overall operational efficiency of the system leads to cost savings in terms of reduced maintenance, lower energy consumption, and increased production throughput. As industries continue to prioritize sustainability and efficiency, the use of advanced pneumatic conveying equipment becomes increasingly important for handling sintered dust materials effectively.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top