Vitrified microspheres, also known as expanded glass microspheres, are a lightweight, inorganic filler widely used in construction, insulation, and other industrial applications. The efficient and reliable transport of these materials is crucial for maintaining production efficiency and ensuring product quality. Pneumatic conveying systems have emerged as a preferred solution for handling vitrified microspheres due to their ability to transport materials in a dust-free environment, reduce labor costs, and enhance overall operational safety. This article explores the working principle and key features of such equipment, providing insights into its design, functionality, and practical applications.
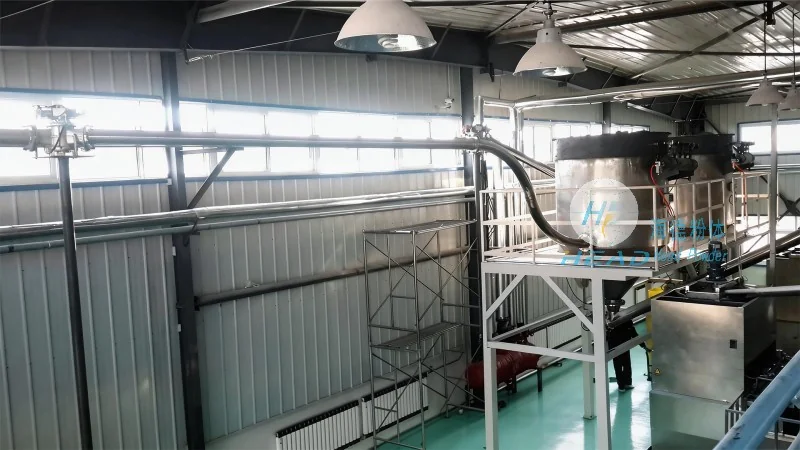
The core of pneumatic conveying equipment lies in the use of air as the conveying medium to transport granular or powdery materials. For vitrified microspheres, the system typically operates under negative pressure (suction) or positive pressure (blowing). In a suction system, a vacuum is created at the material inlet, drawing the microspheres into the conveying line. The air and material mixture then travels through the pipeline to the discharge point, where the material is separated from the air using a cyclone separator or other filtration device. Positive pressure systems, on the other hand, use compressed air to push the material through the pipeline, often requiring higher air pressure and more robust pipeline design. The selection between suction and positive pressure depends on factors such as material characteristics, distance, and system layout. The equipment includes key components like a hopper for material storage, a rotary valve for controlled discharge, a conveying line (usually made of stainless steel or other corrosion-resistant materials to prevent material degradation), a fan or blower for air supply, and a separator for material recovery. The entire process is automated, with sensors and control systems monitoring pressure, flow, and material levels to ensure smooth operation.
1. Dust-Free Operation: Unlike traditional belt or bucket elevators, pneumatic conveying systems operate in a closed loop, minimizing dust generation and improving workplace air quality. This is particularly important for vitrified microspheres, which can be fine and easily airborne, posing health risks and contamination issues. The enclosed system also prevents material loss and cross-contamination.
2. Efficient Material Transport: Pneumatic conveying allows for high-speed material transport over long distances, often up to several hundred meters, with minimal energy consumption compared to mechanical systems. The air velocity and pipeline design are optimized to ensure the material is fully suspended and conveyed without clogging or degradation.
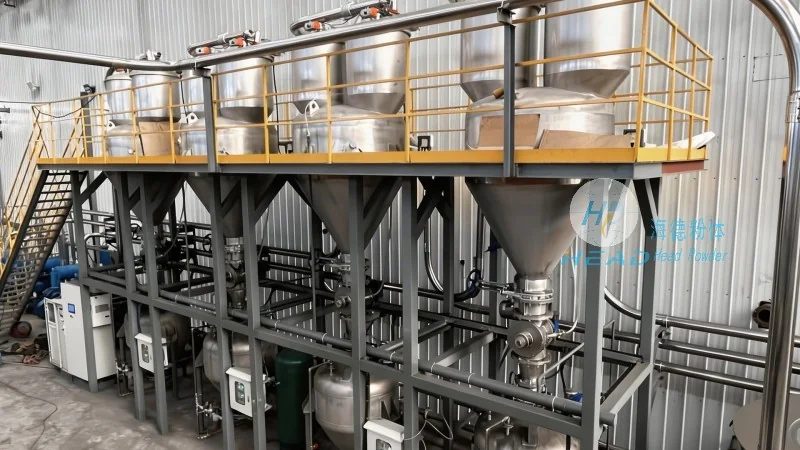
3. Low Maintenance and Long Service Life: The absence of moving parts in the conveying line (except for the hopper and valve) reduces wear and tear, leading to lower maintenance costs and longer equipment lifespan. Stainless steel components further enhance durability, especially when handling corrosive or abrasive materials like vitrified microspheres.
4. Flexible System Design: Pneumatic conveying systems can be easily integrated with existing production lines or expanded to accommodate increased production capacity. The modular design allows for customization based on specific material properties, such as particle size, density, and moisture content. This flexibility makes the equipment suitable for a wide range of industrial applications, from small-scale laboratory use to large-scale manufacturing.
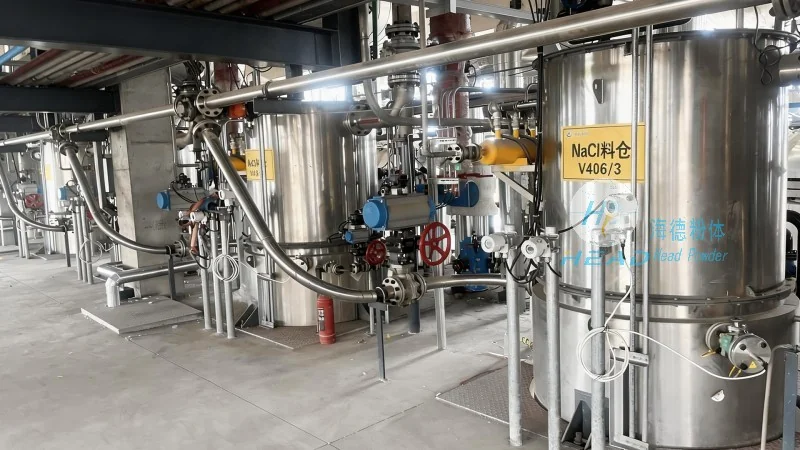
5. Environmental and Safety Benefits: By eliminating the need for open handling, pneumatic conveying reduces the risk of dust explosions and improves overall workplace safety. The closed system also complies with environmental regulations regarding dust emissions, making it an environmentally friendly choice for material transport. Additionally, the system’s ability to handle materials at high temperatures or in hazardous environments (with appropriate modifications) adds to its versatility.
Vitrified microsphere pneumatic conveying equipment is widely used in various industries, including construction, insulation, and composite manufacturing. In the construction sector, it is used to transport microspheres for lightweight concrete and insulation panels, where consistent material quality is critical. The insulation industry benefits from the ability to handle large volumes of microspheres efficiently, reducing production time and costs. Composite manufacturers use the system to blend microspheres with resins and other additives, ensuring uniform distribution and enhancing product performance. The advantages of this equipment, such as dust-free operation and high efficiency, make it a preferred choice over traditional methods in these applications.
Pneumatic conveying equipment for vitrified microspheres offers a reliable, efficient, and safe solution for material transport in industrial settings. Its working principle, based on air as the conveying medium, combined with key features like dust-free operation and low maintenance, makes it an ideal choice for handling lightweight, fine materials. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the specific needs of clients. With a focus on innovation and customer satisfaction, the company provides comprehensive solutions that enhance operational efficiency and product quality. Based in Shandong, China, HeadPowder leverages advanced technology and expertise to deliver equipment that meets the demands of modern industrial production, ensuring long-term success for its clients in the vitrified microsphere industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top