Understanding the working principle and features of dry powder and particulate pneumatic conveying equipment is crucial for industries that rely on efficient material handling solutions. This article provides a detailed overview of how such systems operate and the key characteristics that make them effective in various applications.
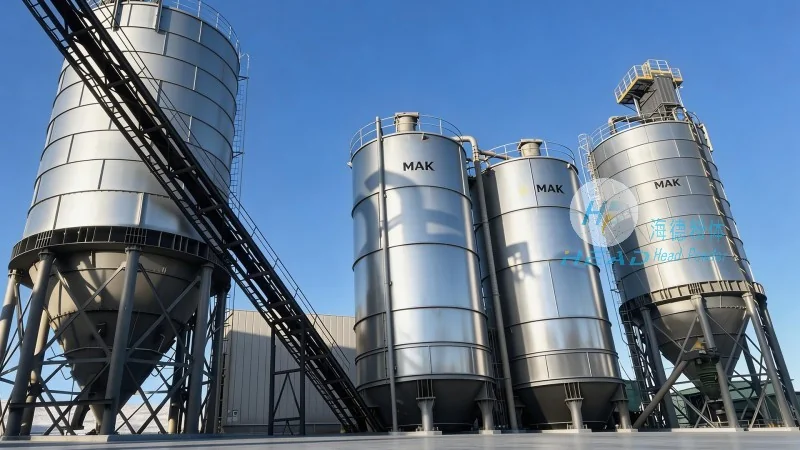
Pneumatic conveying systems are used to transport dry powders and particulate materials through a pipeline using air or gas as the conveying medium. These systems are widely adopted in industries like pharmaceuticals, food processing, chemical manufacturing, and cement production due to their ability to handle a wide range of materials with minimal product degradation. The core components of a typical pneumatic conveying system include a material feed hopper, a conveying line, a dust separator, and a collection bin. The system operates by creating a pressure differential or using vacuum to move the material through the pipeline.
The working principle of dry powder pneumatic conveying equipment involves several key steps. First, the dry powder is fed into the system from a hopper or silo. The material is then introduced into a conveying line where it is mixed with air or gas under controlled conditions. The air flow is typically generated by a blower or a vacuum pump, which creates the necessary pressure or suction to move the material. As the material travels through the pipeline, it is carried by the air stream, and the velocity of the air is adjusted to ensure the material remains suspended and moves efficiently. The conveying process continues until the material reaches the destination point, where it is separated from the air and collected in a designated bin. The separation is often achieved through a cyclone separator or a bag filter, which removes the powder from the air stream. The separated air is then either vented to the atmosphere or recirculated back into the system, depending on the system design and the material properties.
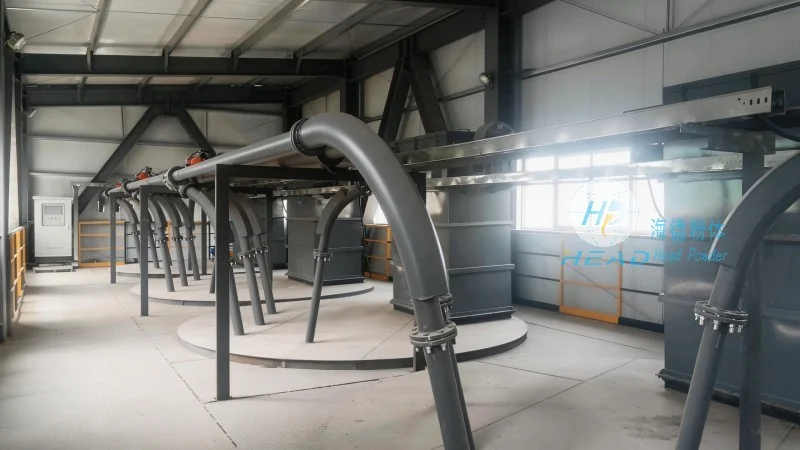
Several key features distinguish pneumatic conveying equipment from other material handling methods. One of the primary advantages is the ability to transport materials over long distances with minimal maintenance. The system is also highly flexible, as it can be easily adapted to handle different types of powders and particulates. Another important feature is the ability to maintain product integrity, as the material is not in direct contact with other surfaces or equipment, reducing the risk of contamination or degradation. Additionally, pneumatic conveying systems can be designed to operate in both positive pressure and negative pressure modes, providing versatility in various industrial settings. The equipment is also relatively compact and can be installed in confined spaces, making it suitable for facilities with limited floor space. Furthermore, modern pneumatic conveying systems are equipped with advanced control systems that allow for precise regulation of air flow, pressure, and material feed rate, ensuring optimal performance and efficiency.
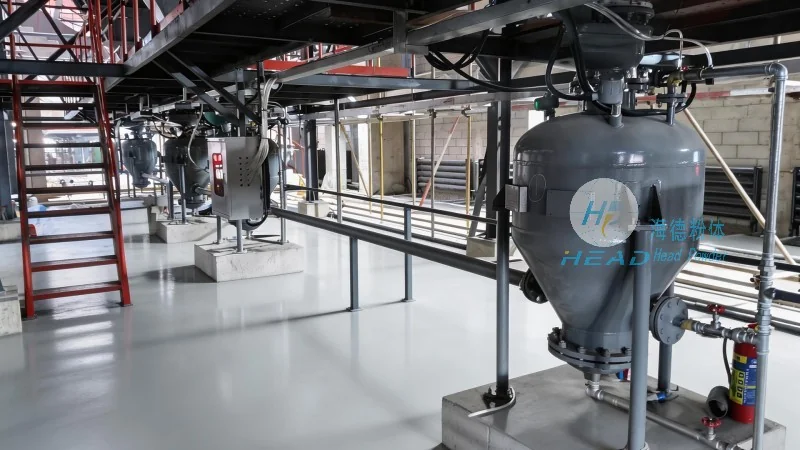
Dry powder and particulate pneumatic conveying equipment is widely used in various industrial applications. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high purity requirements, ensuring that the materials are handled in a sterile and contamination-free environment. In the food processing industry, pneumatic conveying is used to transport ingredients like flour, sugar, and spices, maintaining the quality and freshness of the products. The chemical manufacturing industry utilizes these systems to handle a variety of chemicals, including powders and granules, with the ability to control the temperature and pressure during the conveying process. In the cement and construction industry, pneumatic conveying is used to transport raw materials like limestone and clinker, improving the efficiency of the production process. The benefits of using pneumatic conveying systems in these applications include increased productivity, reduced labor costs, and improved safety, as the material is handled in a closed system, minimizing dust exposure and the risk of accidents.
In conclusion, dry powder and particulate pneumatic conveying equipment is a highly effective and versatile solution for material handling in various industries. The working principle, which involves the use of air or gas to transport materials through a pipeline, offers numerous advantages including minimal product degradation, flexibility, and efficiency. The key features of these systems, such as their ability to handle long distances, maintain product integrity, and operate in different modes, make them suitable for a wide range of applications. As a leading provider of pneumatic conveying solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality equipment tailored to meet the specific needs of different industries. With a focus on innovation and customer satisfaction, HeadPowder provides reliable and efficient solutions that enhance productivity and safety in material handling operations. Based in Shandong, China, HeadPowder serves clients globally, delivering customized pneumatic conveying systems that meet the highest standards of performance and quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top