For industrial applications involving the handling of sodium bicarbonate powder, an efficient and reliable conveying system is essential to ensure smooth material flow and maintain product quality. The pneumatic conveying system for sodium bicarbonate powder, offered by Shandong HeadPowder Engineering Co., Ltd., is a specialized solution designed to meet these demands. This article will explore the working principle and key features of this system, providing a comprehensive understanding of its functionality and benefits.
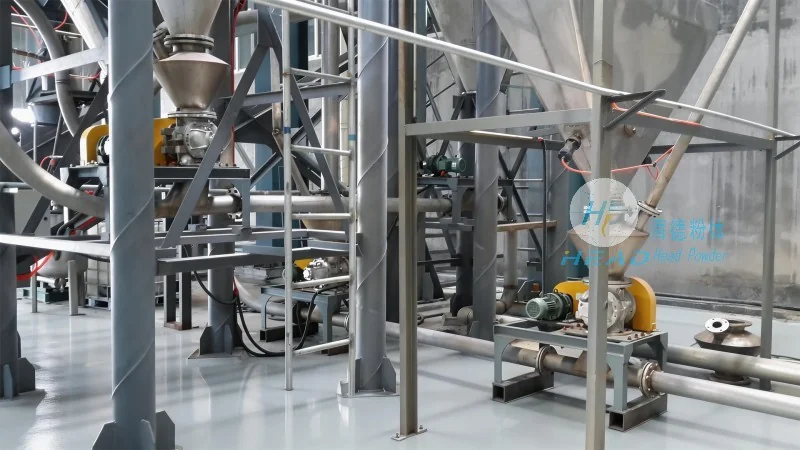
The pneumatic conveying system for sodium bicarbonate powder operates on the principle of using air or gas as the conveying medium to transport dry powder materials. The system typically consists of several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The process begins with the sodium bicarbonate powder being fed from the hopper into the conveying line. A fan or blower then generates a flow of air within the line, creating a pressure differential that propels the powder particles forward. The powder is suspended in the air stream and transported through the pipeline to the destination point. Upon reaching the receiver, the air is separated from the powder, often through a cyclone separator or a filter, and the powder is collected in the receiver. The system may also include a vacuum or pressure mode, depending on the specific application requirements. The entire process is controlled by a system of valves, sensors, and control panels to ensure precise and consistent operation.
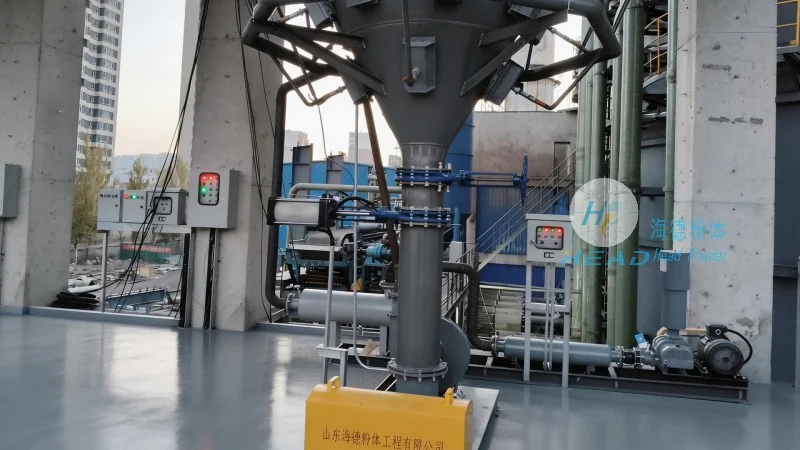
Shandong HeadPowder Engineering Co., Ltd. has designed the sodium bicarbonate powder pneumatic conveying system with several notable features that enhance its performance and reliability. One of the primary features is its ability to handle fine and abrasive powders like sodium bicarbonate without causing excessive wear or degradation. The system utilizes high-quality materials, such as stainless steel or corrosion-resistant alloys, for the conveying line and components to ensure durability and resistance to chemical exposure. Another key feature is the system's flexibility in terms of conveying distance and layout. It can be configured to accommodate various pipeline lengths and angles, making it suitable for complex industrial setups. The system also offers adjustable flow rates and pressure settings, allowing for precise control over the material transport process. Additionally, the system is equipped with safety features, including pressure relief valves and air filtration systems, to prevent over-pressurization and ensure a clean working environment. The integration of advanced sensors and monitoring systems enables real-time tracking of the conveying process, providing operators with valuable data on flow rates, pressure, and material levels. This helps in optimizing the system's performance and preventing potential issues before they occur. The system's design also emphasizes energy efficiency, with optimized air flow and reduced energy consumption compared to traditional mechanical conveying methods. Overall, the sodium bicarbonate powder pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. combines efficiency, reliability, and adaptability, making it an ideal choice for industrial applications requiring the safe and effective transport of sodium bicarbonate powder.
Adopting the sodium bicarbonate powder pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers several significant benefits for industrial operations. Firstly, it eliminates the need for manual handling of the powder, reducing the risk of dust exposure and improving workplace safety. The system also minimizes product contamination, as the enclosed pipeline prevents contact with external contaminants. This is particularly important for sodium bicarbonate, which is often used in food and pharmaceutical applications where purity is critical. The system's ability to maintain consistent flow rates and pressure ensures that the powder is transported uniformly, reducing the risk of segregation or agglomeration. This leads to improved product quality and reduced waste. Additionally, the system's energy efficiency contributes to lower operational costs over time. The reduced need for maintenance due to the use of durable materials and advanced components also minimizes downtime and maintenance expenses. The system's adaptability allows it to be integrated into existing industrial setups with minimal disruption, making it a cost-effective solution for upgrading or expanding material handling capabilities. Overall, the pneumatic conveying system provides a reliable and efficient method for transporting sodium bicarbonate powder, enhancing operational efficiency and product quality while reducing costs and improving safety.
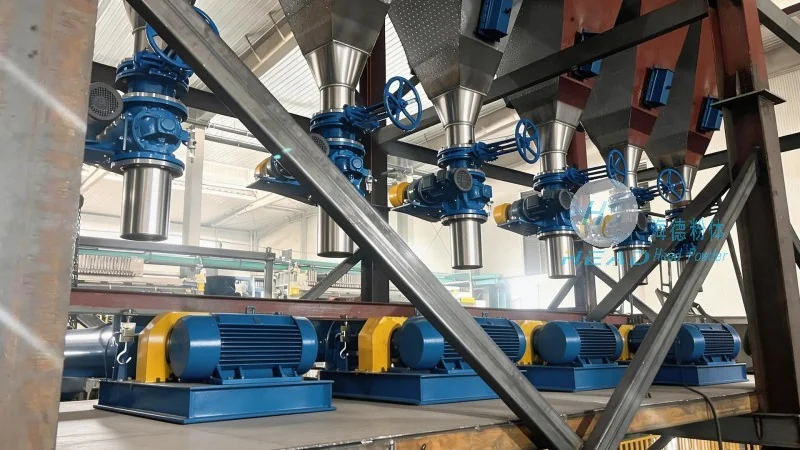
In conclusion, the sodium bicarbonate powder pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. is a sophisticated and effective solution for industrial material handling. By leveraging the principles of pneumatic transport, the system efficiently moves sodium bicarbonate powder while maintaining product integrity and operational safety. The key features, including durability, flexibility, and energy efficiency, make it a superior choice compared to traditional mechanical conveying methods. Implementing this system can lead to significant improvements in operational efficiency, cost reduction, and product quality for industries relying on sodium bicarbonate. With its robust design and reliable performance, the system from Shandong HeadPowder Engineering Co., Ltd. stands as a leading solution for the pneumatic conveying of sodium bicarbonate powder, ensuring long-term success and sustainability in industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top