High-pressure bin pumps represent advanced material handling equipment designed to efficiently transport bulk materials from storage bins to discharge points. This article explores the fundamental working principle and key characteristics of high-pressure bin pumps, offering insights into their operational mechanisms and practical applications in various industrial sectors.
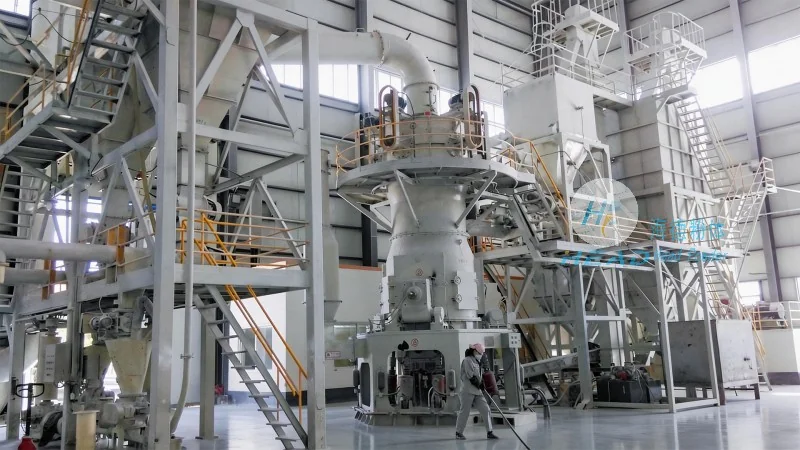
HeadPowder, a prominent manufacturer in the material handling industry, specializes in delivering reliable and efficient equipment solutions. The company operates under the full name Shandong HeadPowder Engineering Co., Ltd., with its headquarters located in Shandong, China. HeadPowder is committed to innovation and customer-centric service, providing high-quality high-pressure bin pumps tailored to meet diverse industrial requirements.
High-pressure bin pumps operate on the principle of pneumatic pressure to facilitate material transport. The process begins with the hopper being filled with the bulk material to be conveyed. Once the hopper is adequately loaded, the pump's air compressor generates high-pressure air, which is then introduced into the pump chamber. This high-pressure air creates a force that propels the material through the discharge line, ensuring a smooth and continuous flow. The pump's design allows for precise control over pressure and flow rate, enabling operators to adjust delivery speed according to specific application needs. This mechanism eliminates the need for mechanical components like belts or gears, reducing maintenance requirements and enhancing operational reliability.
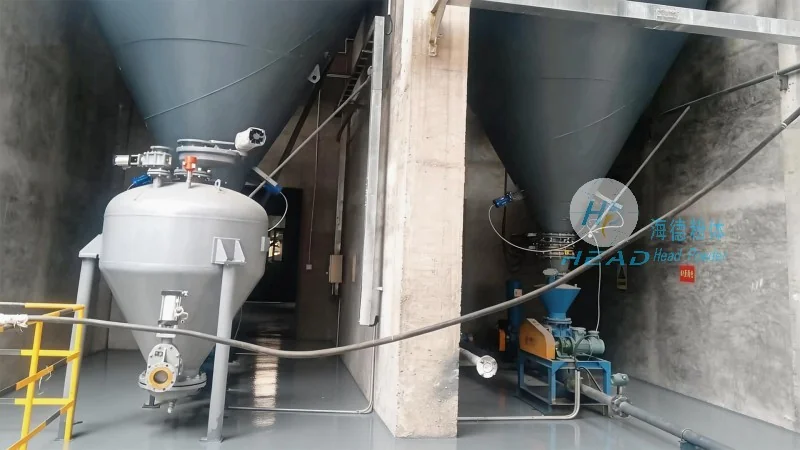
High-pressure bin pumps are distinguished by several notable characteristics that make them suitable for demanding industrial environments. Firstly, they exhibit high efficiency in material transport, minimizing downtime and maximizing productivity. The use of compressed air as the driving force makes them energy-efficient compared to traditional mechanical conveyors. Secondly, these pumps are highly durable and can handle a wide range of materials, including powders, granules, and even abrasive substances, without causing significant wear. Their robust construction ensures long service life and low maintenance costs. Additionally, high-pressure bin pumps are versatile, capable of operating in various settings—from indoor facilities to outdoor installations—making them adaptable to different industrial needs. The compact design also allows for easy integration into existing production lines, reducing installation time and costs.
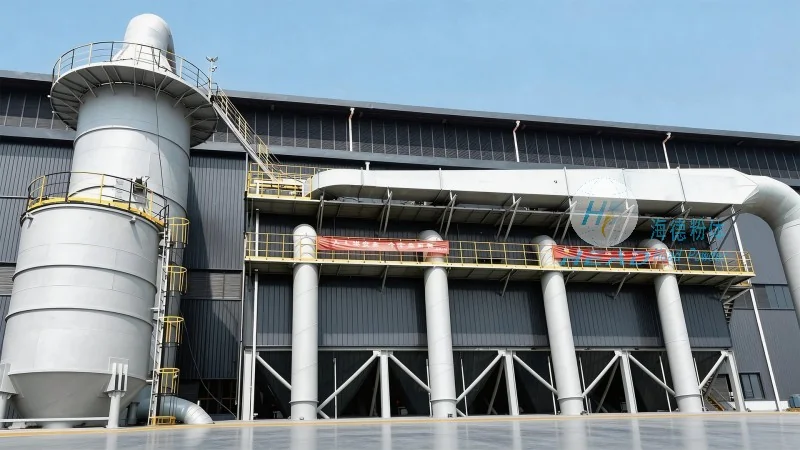
High-pressure bin pumps find extensive applications across multiple industries. In the mining sector, they are used to transport ore and other bulk materials from storage bins to processing plants, ensuring a steady supply of raw materials. In construction, they facilitate the handling of sand, gravel, and cement, improving material flow on job sites. The food processing industry benefits from the hygienic design of high-pressure bin pumps, which allows for safe handling of food-grade materials without contamination. The chemical industry utilizes these pumps for transporting various powders and granules, enabling precise control over material flow and preventing dust emissions. The primary benefits of using high-pressure bin pumps include increased operational efficiency, reduced labor costs, and enhanced safety due to automated material handling processes. Furthermore, their ability to handle abrasive materials reduces equipment wear and extends the lifespan of the system.
High-pressure bin pumps represent a sophisticated solution for bulk material handling, combining advanced technology with practical design. With their efficient working principle and versatile characteristics, they offer significant advantages over traditional conveyor systems. As a trusted manufacturer, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide high-quality high-pressure bin pumps that meet the evolving needs of the industrial sector. By leveraging the expertise and experience of HeadPowder, industries can enhance their material handling processes, improve productivity, and achieve greater operational efficiency. The combination of reliable performance, durability, and adaptability makes high-pressure bin pumps an essential component in modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top