Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of advanced powder handling solutions. Our company specializes in the design, manufacturing, and installation of bottom-discharge powder transport systems, which are essential for efficient material handling in various industrial applications. This article will explore the working principle and key features of these systems, highlighting their benefits and practical applications.
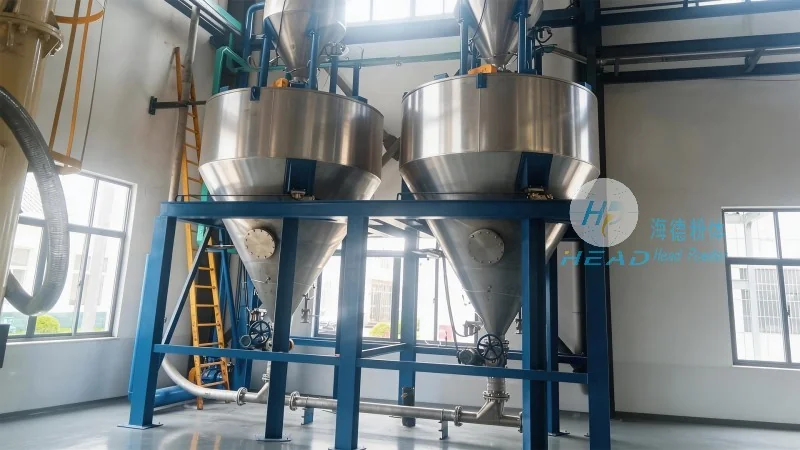
At the core of our bottom-discharge powder handling systems is a specialized design that enables the seamless transfer of bulk powders from storage silos or hoppers to processing units. The system operates by utilizing a combination of mechanical and pneumatic components to ensure reliable and consistent material flow. A primary component is the bottom-discharge valve or feeder, which is integrated into the base of the storage vessel. This valve is engineered to control the release of powder under controlled conditions, preventing clogging and ensuring a smooth discharge process.
The working principle of our bottom-discharge powder handling systems involves several interconnected steps. Initially, the bulk powder is stored in a silo or hopper. The bottom-discharge valve is then activated to allow the powder to flow into a conveying pipeline. Depending on the system configuration, the powder may be conveyed through a pneumatic system, where air is used to create a flow of material, or through a mechanical conveyor system, such as a screw or belt conveyor. The system is designed to maintain a consistent flow rate, ensuring that the material is transported efficiently to the target destination.
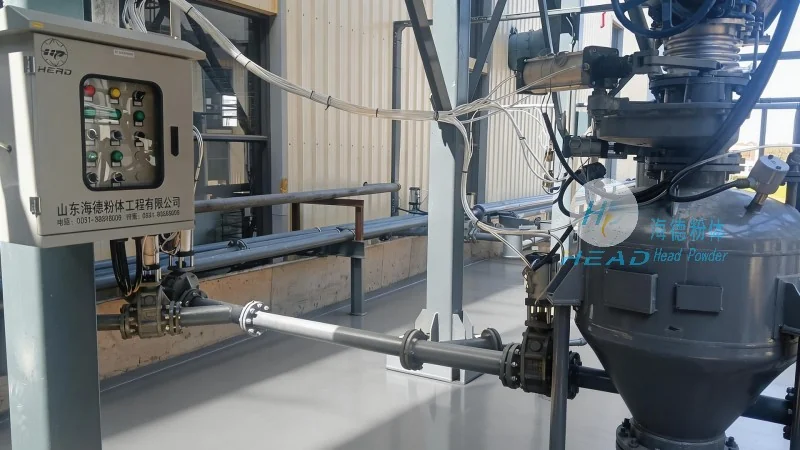
Our bottom-discharge powder handling systems are characterized by several key features that make them ideal for industrial applications. One of the most significant advantages is their ability to handle a wide range of powder types, including fine powders, granules, and bulk materials. The system is designed to minimize material loss and degradation, which is crucial for maintaining product quality. Additionally, the bottom-discharge mechanism reduces the risk of dust accumulation and improves safety in the workplace. The system is also highly customizable, allowing us to tailor the design to meet the specific requirements of each client's operation.
The efficiency of our bottom-discharge powder handling systems is a direct result of their robust engineering and advanced technology. The systems are built to withstand the demands of continuous operation, ensuring long-term reliability. The use of high-quality materials and precision manufacturing processes ensures that the components are durable and resistant to wear and tear. This reliability is further enhanced by the integration of advanced control systems, which allow for real-time monitoring and adjustment of the flow rate. The result is a system that operates with minimal downtime and maximum productivity.
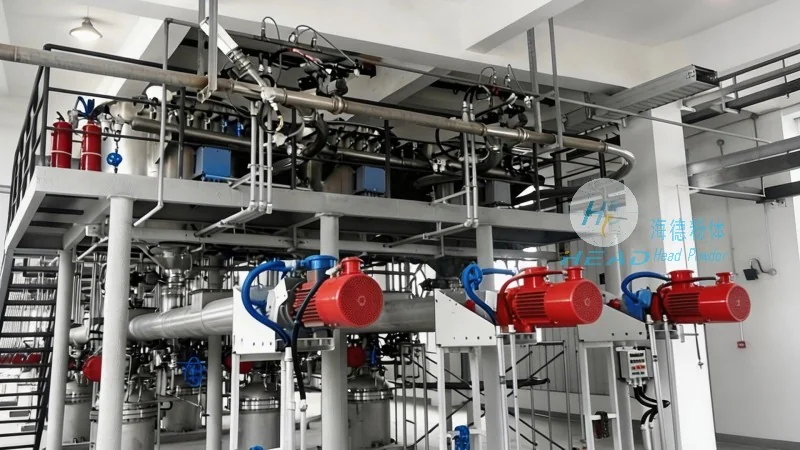
Bottom-discharge powder handling systems are widely used in a variety of industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, these systems are used to handle ingredients such as flour, sugar, and spices, ensuring that the material is transferred without contamination or loss. In the pharmaceutical industry, the systems are used to handle active ingredients and excipients, maintaining the purity and quality of the final product. In the chemical industry, the systems are used to handle raw materials and intermediates, ensuring efficient production processes. The versatility of our systems makes them suitable for a wide range of applications, from small-scale operations to large-scale industrial facilities.
Shandong HeadPowder Engineering Co., Ltd. is committed to providing innovative and reliable bottom-discharge powder handling systems that meet the needs of our clients. Our systems are designed to enhance efficiency, reduce costs, and improve product quality. By leveraging advanced technology and expert engineering, we have developed systems that are efficient, reliable, and adaptable to various industrial requirements. We invite you to explore our range of products and services, and to learn more about how our bottom-discharge powder handling systems can benefit your operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top