When it comes to transporting calcined sand, selecting the right conveying method is crucial for efficiency, cost-effectiveness, and operational safety. In industrial applications, calcined sand, a material derived from the calcination of raw materials like limestone or other minerals, requires specialized handling due to its properties such as high temperature, abrasive nature, and potential dust generation. The choice of conveying system directly impacts production throughput, equipment longevity, and overall process reliability. This article explores the various options available for calcined sand transportation, with a focus on the advanced solutions offered by Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder.
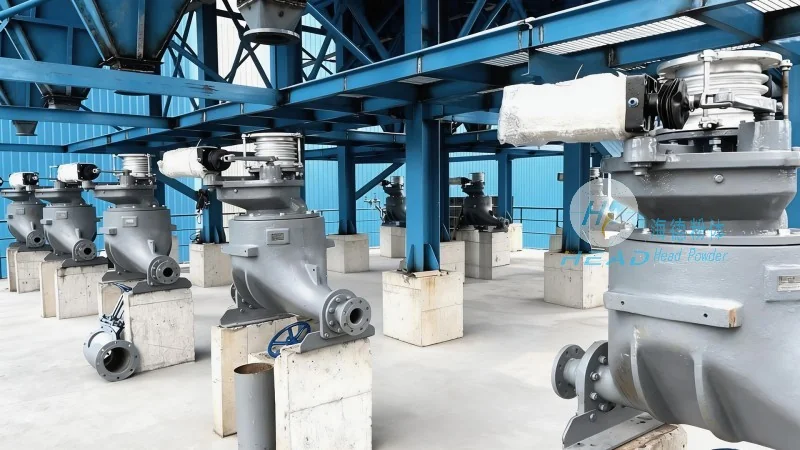
Calcined sand is produced through a high-temperature calcination process, which transforms raw materials into a porous, lightweight material with enhanced properties for specific industrial uses. This material is often used in applications like refractory production, construction materials, and as a component in various manufacturing processes. However, its handling presents unique challenges. The high temperature of the material during processing can lead to heat-related issues if not managed properly. Additionally, calcined sand is typically abrasive, which can cause wear on conveyor components. Dust generation is another critical concern, as it can affect air quality and pose health risks if not controlled. Therefore, the conveying system must be designed to address these challenges effectively, ensuring that the material is transported safely and efficiently from the calcination unit to subsequent processing stages.
Historically, calcined sand has been transported using traditional methods such as belt conveyors, screw conveyors, and bucket elevators. Belt conveyors are widely used for bulk material handling due to their simplicity and ability to transport large quantities over long distances. However, they may not be ideal for calcined sand because of the material's abrasive nature, which can lead to premature wear on the belt and idlers. Screw conveyors are another common option, particularly for horizontal or slightly inclined transport. They are relatively low-cost and can handle a variety of materials, but they are prone to blockages and wear from the abrasive sand, reducing their lifespan and requiring frequent maintenance. Bucket elevators are used for vertical transport, but they can be noisy and may not be suitable for high-temperature materials due to the risk of heat damage to the elevator components. These traditional methods, while effective for some applications, often face limitations in terms of efficiency, maintenance costs, and the ability to handle the specific challenges posed by calcined sand.
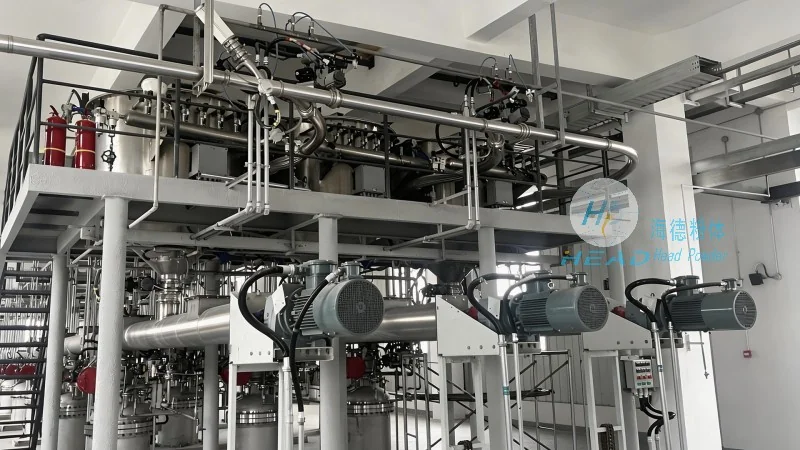
Pneumatic conveying has emerged as a superior alternative to traditional methods for calcined sand transportation. This technology uses compressed air to move the material through a pipeline system, eliminating the need for mechanical components that come into direct contact with the sand. The primary advantages of pneumatic conveying for calcined sand include reduced wear and tear on equipment, as there are no moving parts that can be abraded by the material. This leads to lower maintenance costs and longer equipment life. Additionally, pneumatic systems can handle high-temperature materials without damage, as the material is transported in a sealed pipeline, protecting it from external heat sources. Dust control is another significant benefit, as the system operates in a closed environment, preventing dust from escaping into the workplace and reducing the risk of respiratory issues for operators. Pneumatic conveying also offers flexibility in terms of layout, allowing for complex transport routes that can accommodate changes in the production process or facility layout. This adaptability makes it an attractive option for modern industrial operations.
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced pneumatic conveying solutions tailored to the unique needs of calcined sand applications. The company, based in Shandong, China, has extensive experience in designing and manufacturing customized conveying systems that address the challenges associated with handling this material. HeadPowder's solutions are engineered to maximize efficiency while minimizing operational costs and ensuring compliance with safety and environmental regulations. The company's approach involves a comprehensive understanding of the client's process requirements, including the volume of calcined sand to be transported, the distance and layout of the transport route, and the specific properties of the material. This allows HeadPowder to design a system that is optimized for the application, whether it's a low-pressure, low-velocity system for gentle material handling or a high-pressure, high-velocity system for rapid transport over longer distances.
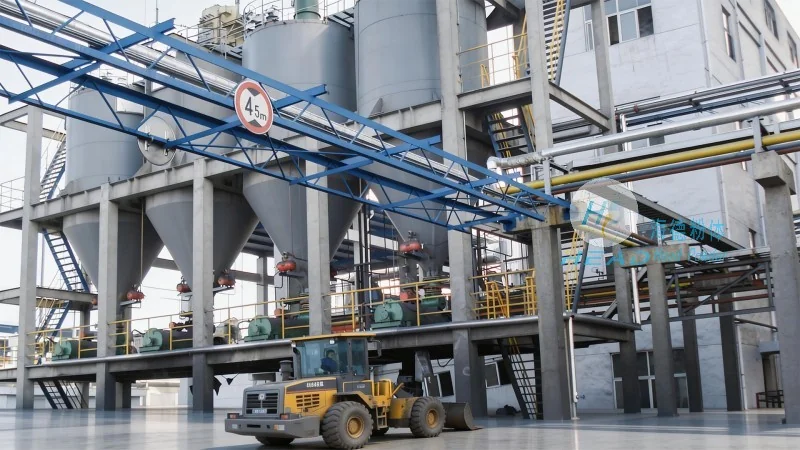
HeadPowder's calcined sand pneumatic conveying systems incorporate several key features that enhance performance and reliability. One of the primary features is the use of high-quality materials for the pipeline and components, such as stainless steel or specialized alloys, which are resistant to the abrasive nature of calcined sand and can withstand high temperatures. The system design includes features to minimize wear, such as smooth interior surfaces and specialized valves that reduce friction and material impact. Additionally, the system incorporates dust collection and filtration components to ensure that the material is transported in a clean, controlled environment, meeting environmental standards and protecting operator health. The control systems are also advanced, allowing for precise regulation of air pressure and flow, which optimizes the conveying process and reduces energy consumption. These features collectively contribute to a more efficient, reliable, and cost-effective conveying solution for calcined sand.
HeadPowder recognizes that each industrial facility has unique requirements, and therefore, the company offers customized pneumatic conveying solutions that can be integrated with existing production lines. The design process involves working closely with clients to understand their specific needs and constraints. This includes assessing the current infrastructure, such as the location of the calcination unit, the storage areas, and the processing equipment, to determine the most efficient transport route. HeadPowder's engineers then design a system that can be seamlessly integrated into the existing setup, minimizing disruptions to production. The company also provides support during the installation and commissioning phase, ensuring that the system is properly set up and functioning optimally. This approach allows clients to upgrade their calcined sand conveying process without major overhauls, making it a cost-effective solution for improving efficiency and reducing maintenance costs.
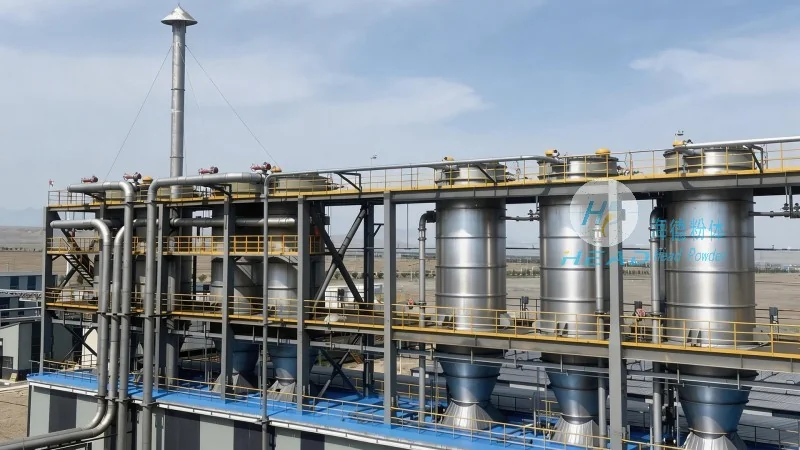
HeadPowder has successfully implemented calcined sand pneumatic conveying systems in various industrial applications, demonstrating the effectiveness of their solutions. For example, in a refractory production facility, the company installed a high-pressure pneumatic system to transport calcined sand from the calcination unit to the mixing and molding areas. The system was designed to handle large volumes of abrasive material over a significant distance, and it has since reduced maintenance costs by 30% and improved production throughput by 20% compared to the previous belt conveyor system. Another case study involves a construction materials manufacturer that used HeadPowder's low-pressure, low-velocity system to transport calcined sand from storage silos to the production line. The system's gentle handling minimized material degradation and reduced dust generation, leading to improved product quality and better compliance with environmental regulations. These examples illustrate the benefits of pneumatic conveying for calcined sand and the effectiveness of HeadPowder's customized solutions in addressing specific client needs.
In conclusion, the choice of calcined sand conveying method is critical for industrial operations, and pneumatic conveying, particularly with advanced solutions from companies like Shandong HeadPowder Engineering Co., Ltd., offers significant advantages over traditional methods. The benefits of reduced wear, improved dust control, and enhanced flexibility make pneumatic systems an attractive option for modern industrial applications. HeadPowder's expertise in designing and manufacturing customized pneumatic conveying solutions ensures that clients can achieve optimal performance, cost savings, and operational efficiency. As industrial processes continue to evolve, the demand for efficient and reliable calcined sand transportation systems will remain high, and companies like HeadPowder will play a key role in providing the technology needed to meet these challenges.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top