Glucose powder, a critical ingredient in various industries including pharmaceuticals, food processing, and chemical manufacturing, requires specialized handling systems to ensure efficient and safe transportation. Understanding the material handling system for glucose powder and its underlying design principles is essential for optimizing production processes and maintaining product quality. This article explores the key components, operational mechanisms, and engineering considerations of glucose powder material handling systems, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in providing tailored solutions for such applications.
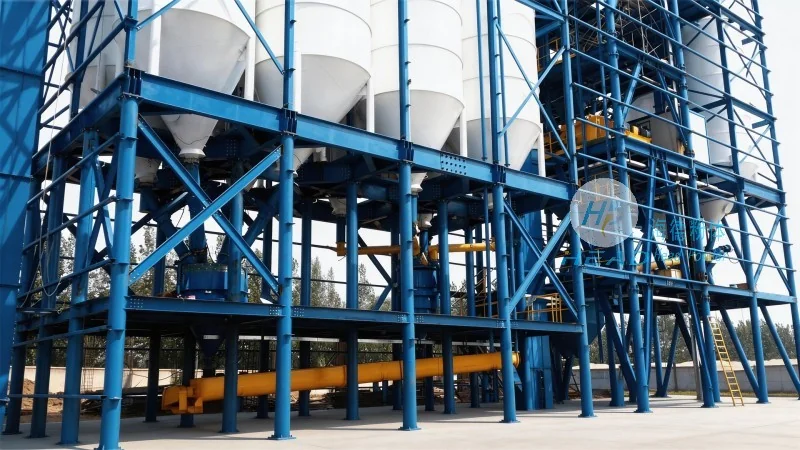
Glucose powder, characterized by its fine particle size and hygroscopic properties, poses unique challenges during material handling. Traditional bulk material handling methods may not be suitable due to the risk of caking, agglomeration, and dust generation. A dedicated glucose powder material handling system is designed to address these challenges by integrating advanced equipment and control strategies. Such systems typically include storage silos, feeding mechanisms, conveying equipment, and processing units, all working in tandem to ensure seamless material flow from storage to end-use applications.
The core components of a glucose powder material handling system are engineered to handle the specific physical and chemical properties of glucose powder. These components include:
1. Storage Silos: Large-capacity, airtight silos are used to store glucose powder, minimizing exposure to moisture and air to prevent caking. The silos are often equipped with internal agitators or vibrators to maintain material flow and prevent material bridging.
2. Feeding Equipment: Precision feeders, such as rotary valves or screw feeders, regulate the flow of glucose powder from the silo to the conveying system. These devices ensure consistent and controlled discharge, which is crucial for maintaining stable conveying rates.
3. Conveying Equipment: Depending on the application and distance requirements, different conveying methods are employed. For short distances, screw conveyors or pneumatic conveying systems are commonly used. Screw conveyors are ideal for horizontal or slight incline transport, while pneumatic systems are suitable for longer distances or when dust control is a priority.
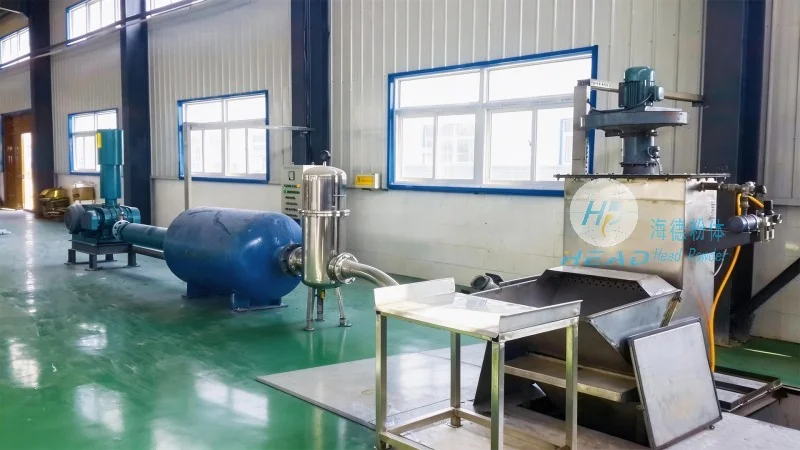
4. Control Systems: Integrated control panels monitor and regulate the entire system, ensuring optimal performance. Sensors for level, flow, and pressure are used to detect anomalies and adjust operations in real-time, enhancing safety and efficiency.
The design of a glucose powder material handling system is guided by several fundamental principles aimed at maximizing efficiency, minimizing product degradation, and ensuring operational safety. These principles include:
1. Preventing Caking and Agglomeration: Glucose powder is prone to forming lumps due to moisture absorption and particle interaction. The system design incorporates features like temperature control, moisture-proofing, and vibration to prevent caking. For instance, heated silos or desiccant systems may be used to maintain optimal moisture levels.
2. Ensuring Uniform Flow: Uniform material flow is critical to avoid surges or blockages in the conveying line. The system uses variable-speed drives and adjustable feeders to maintain a consistent flow rate, which is particularly important for processes that require precise dosing.
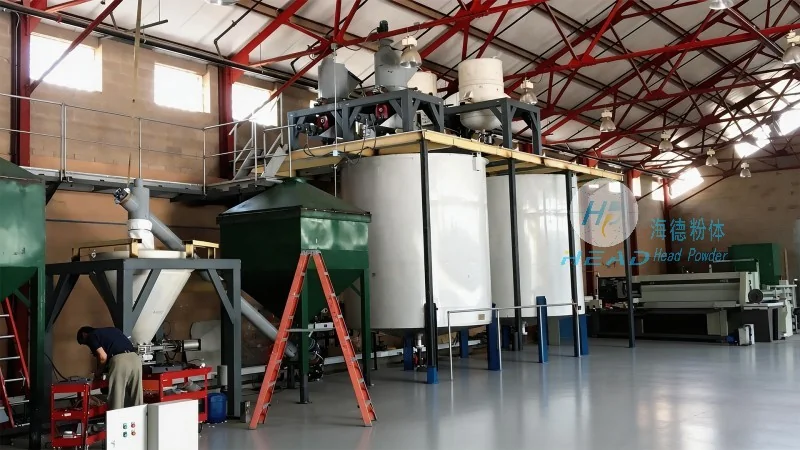
3. Minimizing Dust and Contamination: Glucose powder is a fine particulate that can generate dust during handling. The system incorporates dust collection systems, sealed conveyors, and enclosed feeding mechanisms to contain dust and prevent contamination of the product and the environment.
4. Energy Efficiency: Modern glucose powder handling systems are designed with energy efficiency in mind. This includes using high-efficiency motors, optimizing conveyor speeds, and implementing energy-saving control strategies to reduce operational costs.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized material handling solutions for industries dealing with fine powders like glucose. With years of experience in the field, HeadPowder leverages advanced engineering and manufacturing capabilities to design and supply tailored glucose powder material handling systems. The company’s team of experts works closely with clients to understand their specific requirements, from storage capacity to conveying distance and end-use applications, ensuring that the final system meets all operational and quality standards.
HeadPowder’s commitment to quality and innovation is reflected in its use of cutting-edge technologies and adherence to international standards. The company’s facilities in Shandong, China, are equipped with state-of-the-art equipment and stringent quality control processes, ensuring that every component of the glucose powder handling system is manufactured to the highest specifications. Clients benefit from HeadPowder’s comprehensive service offerings, including system design, installation, commissioning, and after-sales support, providing a complete solution for their material handling needs.
In conclusion, a glucose powder material handling system is a sophisticated engineering solution that addresses the unique challenges associated with handling fine, hygroscopic powders. The design principles and components discussed above are critical for ensuring efficient, safe, and cost-effective operation. For industries relying on glucose powder as a key ingredient, investing in a well-designed material handling system is essential for maintaining product quality, optimizing production efficiency, and ensuring regulatory compliance. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in delivering such specialized systems, combining technical expertise with customer-centric solutions to meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top