Rice grain material handling is a specialized process in the agricultural and food processing industries, focusing on the efficient movement of rice grains from one location to another. This process is crucial for ensuring the smooth operation of rice processing facilities, from storage to packaging. The design principles behind rice grain material handling systems are tailored to address the unique characteristics of rice, such as its size, shape, and moisture content, to minimize damage and maintain quality.
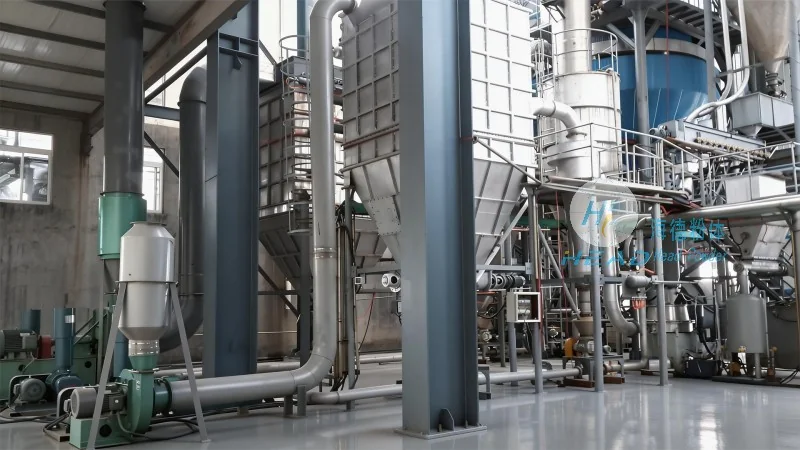
At its core, rice grain material handling involves the use of various equipment and systems to transport, store, and manage rice grains. This includes conveyor systems, elevators, and storage silos, all designed to handle the specific properties of rice. The primary goal is to maintain the integrity of the rice grains, preventing breakage, bruising, or contamination during the handling process. This is particularly important in the food industry, where product quality directly impacts consumer satisfaction and regulatory compliance.
The design of rice grain material handling systems follows several critical principles to ensure optimal performance. First, the equipment must be gentle on the rice grains to avoid physical damage. This often involves using smooth surfaces and low-impact mechanisms, such as belt conveyors with soft materials or rotary valves that minimize friction. Second, the systems must be designed to handle variations in rice grain size and moisture content. Adjustable speed controls and variable tension settings in conveyor belts allow for flexibility in processing different batches of rice. Third, the systems should be hygienic and easy to clean, as rice is a food product that requires strict adherence to food safety standards. Stainless steel components and easy-to-access maintenance points are common features in modern rice grain handling equipment.
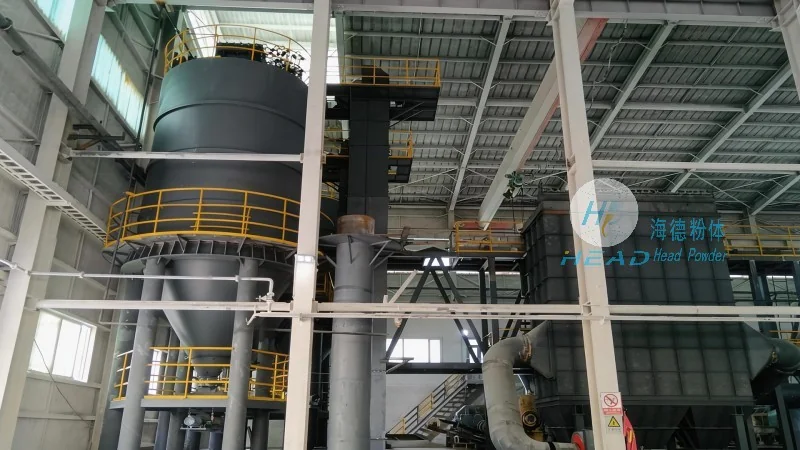
A typical rice grain material handling system consists of several interconnected components. The process often begins with a reception hopper, where raw rice is unloaded from trucks or storage bins. From there, the rice is fed into an elevator or conveyor system that transports it to a cleaning and sorting stage. The cleaning stage may include screens to remove impurities like stones, dust, or other foreign materials. After cleaning, the rice moves to a drying or conditioning unit, if necessary, to adjust moisture levels. Finally, the rice is transferred to a storage silo or packaging line for distribution. Each component is designed to work in harmony, ensuring a continuous and efficient flow of rice throughout the facility.
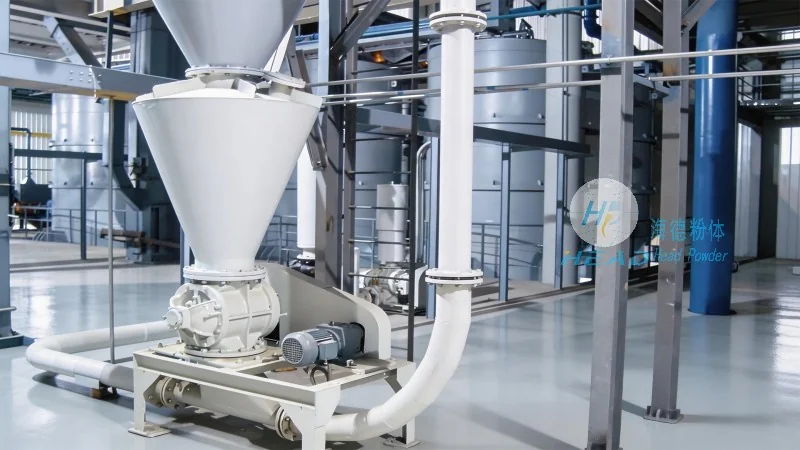
Efficient rice grain material handling is essential for the overall productivity and profitability of rice processing operations. By minimizing damage and loss during handling, companies can reduce waste and lower production costs. Additionally, proper handling ensures that the final product meets quality standards, which is critical for maintaining customer trust and market competitiveness. The design principles and components of the handling system directly impact these outcomes, making them a key investment for any rice processing facility.
In summary, rice grain material handling is a critical aspect of rice processing, requiring specialized equipment and design principles to ensure the quality and integrity of the product. Companies like Shandong HeadPowder Engineering Co., Ltd., based in China, specialize in providing tailored material handling solutions for the rice industry. Their expertise in designing systems that meet the unique needs of rice grains helps processing facilities achieve efficiency, reduce costs, and maintain high standards of product quality. Whether for small-scale or large-scale operations, a well-designed rice grain material handling system is essential for success in the rice processing industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top