Red mud material handling is a specialized process in the mineral processing and industrial waste management sectors, focusing on the efficient transport and handling of red mud, a byproduct of bauxite refining. This material, characterized by its reddish color and high alkalinity, poses unique challenges in terms of handling due to its abrasive nature and potential environmental impact. Understanding the mechanisms and design principles behind red mud material handling is crucial for industries aiming to manage this waste effectively while ensuring operational efficiency and safety. Shandong HeadPowder Engineering Co., Ltd. specializes in providing tailored solutions for red mud material handling, leveraging advanced engineering and materials science to address the challenges associated with this hazardous waste.
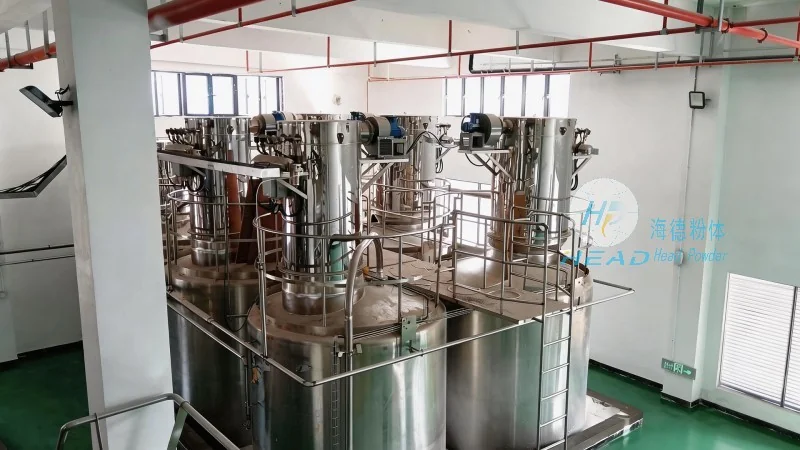
Red mud, also known as bauxite residue, is generated during the Bayer process used to extract aluminum from bauxite ore. It consists of insoluble solids, primarily iron oxides, aluminum hydroxides, and other minerals. The material's properties—such as high density, high moisture content, and abrasive characteristics—make conventional handling equipment less suitable. Therefore, specialized equipment and systems are required to manage red mud safely and efficiently. The primary goal of red mud material handling is to transport this waste from the refinery to disposal or reclamation sites without causing equipment wear, environmental contamination, or operational disruptions.
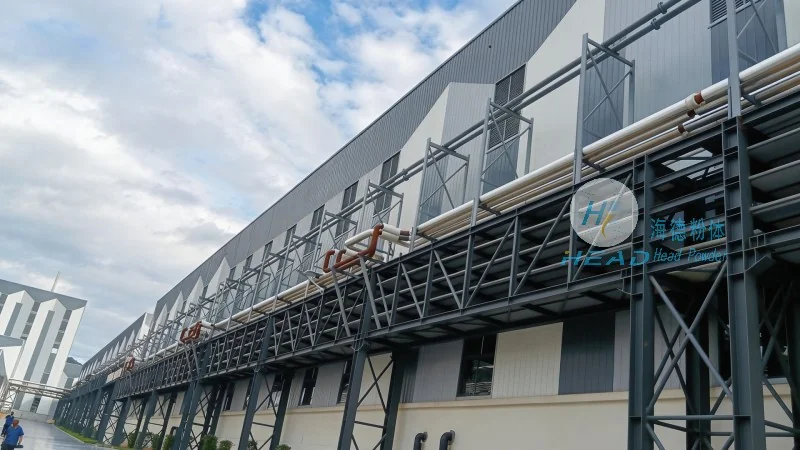
The design of red mud material handling systems adheres to several critical principles to address the unique challenges posed by red mud. First, abrasion resistance is paramount. Equipment components, such as conveyor belts, buckets, and pipelines, must be constructed from durable materials like high-grade steel, rubber, or specialized alloys to withstand the abrasive effects of red mud particles. Second, moisture management is essential. Red mud often contains high levels of moisture, which can affect the flowability and increase the risk of slippage or blockages. Systems may incorporate drying or conditioning steps to improve material handling characteristics. Third, environmental protection is a key consideration. Red mud is a hazardous waste, and handling systems must include measures to prevent dust emissions, leachate formation, and contamination of soil or water. This may involve enclosed conveyor systems, dust suppression mechanisms, and proper containment structures. Fourth, efficiency and reliability are critical for industrial operations. The design must ensure consistent material flow, minimize downtime, and optimize energy consumption. This often involves integrating sensors and automation to monitor system performance and adjust parameters in real-time.
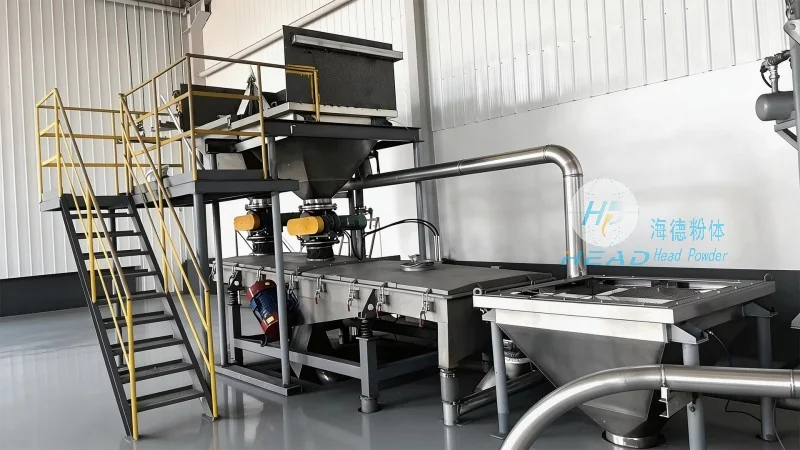
Several types of equipment are commonly used in red mud material handling systems, each tailored to specific operational requirements. Conveyor systems, including belt conveyors and screw conveyors, are widely used for horizontal and vertical transport. Belt conveyors are preferred for long-distance transport due to their high capacity and ability to handle abrasive materials. Screw conveyors are suitable for vertical or inclined transport and can be enclosed to prevent dust emissions. Pneumatic conveying systems use air to transport red mud in a slurry or dry form. This method is effective for short distances and can be integrated with dust collection systems. Bucket elevators are used for vertical transport, particularly in refineries where space is limited. These systems use buckets attached to a chain or belt to lift red mud from lower to upper levels. Pipelines are also employed for transporting red mud, often in a slurry form. These pipelines are typically made of corrosion-resistant materials like stainless steel or lined with protective coatings to prevent wear and leakage.
Modern red mud material handling systems often involve integrated designs that combine multiple equipment types and incorporate automation technologies. This integration enhances operational efficiency and safety. For example, a typical system may include a conveyor belt to transport red mud from the refinery to a storage facility, followed by a screw conveyor to feed a drying or conditioning unit. Sensors are installed along the system to monitor parameters such as flow rate, temperature, and moisture content. Automation systems can adjust conveyor speeds, control the drying process, and alert operators to any anomalies. This level of integration ensures that the system operates smoothly and responds to changes in red mud properties or operational conditions. Additionally, the use of enclosed and sealed equipment reduces the risk of environmental contamination and improves worker safety by minimizing exposure to dust and hazardous materials.
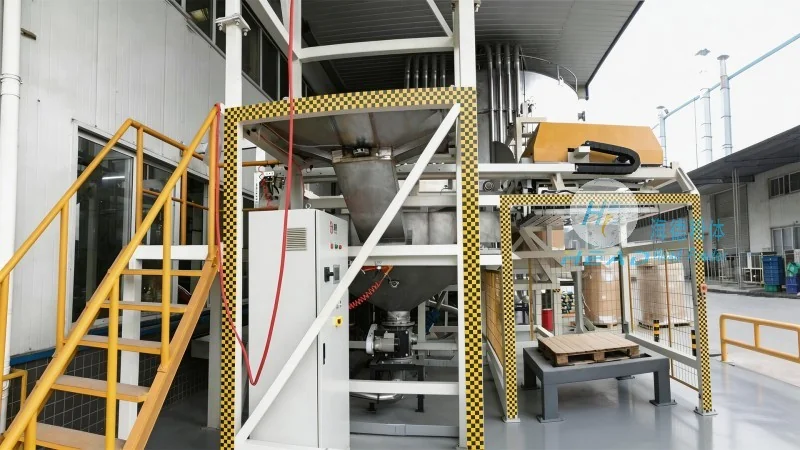
Despite advancements in technology, red mud material handling still faces several challenges. One major challenge is the high cost of specialized equipment and maintenance due to the abrasive nature of red mud. To address this, industries may opt for equipment with replaceable wear parts, such as conveyor belt liners or bucket liners, to reduce long-term costs. Another challenge is the variability in red mud properties, which can affect system performance. To mitigate this, flexible systems with adjustable parameters (e.g., conveyor speed, slurry concentration) are designed to accommodate changes in material characteristics. Environmental regulations also pose challenges, as industries must comply with strict standards for waste disposal and emissions. Solutions include implementing advanced dust suppression systems, using closed-loop water systems to minimize water usage, and conducting regular environmental monitoring to ensure compliance. Finally, the need for skilled personnel to operate and maintain complex systems is a challenge. Training programs and the use of user-friendly automation interfaces help address this by ensuring operators can effectively manage the system.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top