Understanding the Corn Kernels Powder Conveying System Equipment and Its Design Principles
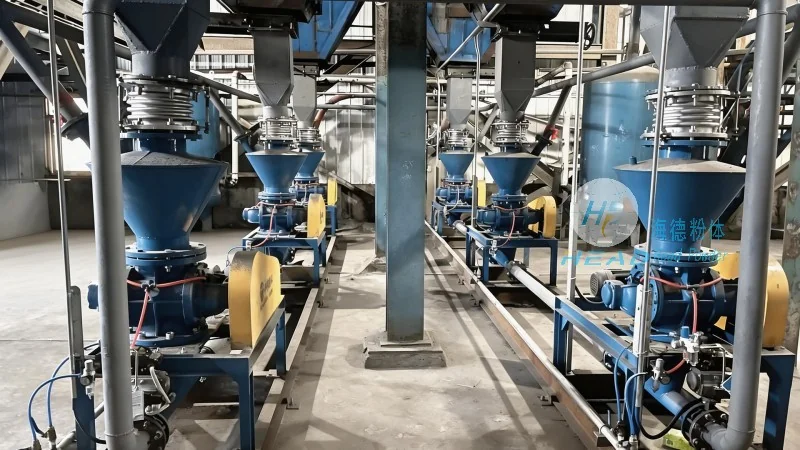
Introduction to Corn Kernels Powder Conveying System Equipment
The corn kernels powder conveying system equipment is a specialized industrial device designed to handle and transport corn kernels in a powder or granular form. This equipment is crucial in various industries, including food processing, agriculture, and chemical manufacturing, where efficient and reliable material handling is essential for production efficiency and product quality. The system typically involves components such as hoppers, conveyors, and control mechanisms that work together to ensure the smooth movement of corn kernels from one processing stage to another.
About HeadPowder: The Manufacturer
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in the design, development, and production of advanced powder handling equipment. With a strong presence in China, particularly in Shandong province, the company has built a reputation for delivering high-quality, durable, and efficient conveying systems tailored to the specific needs of its clients. HeadPowder's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking reliable solutions for their material handling challenges.
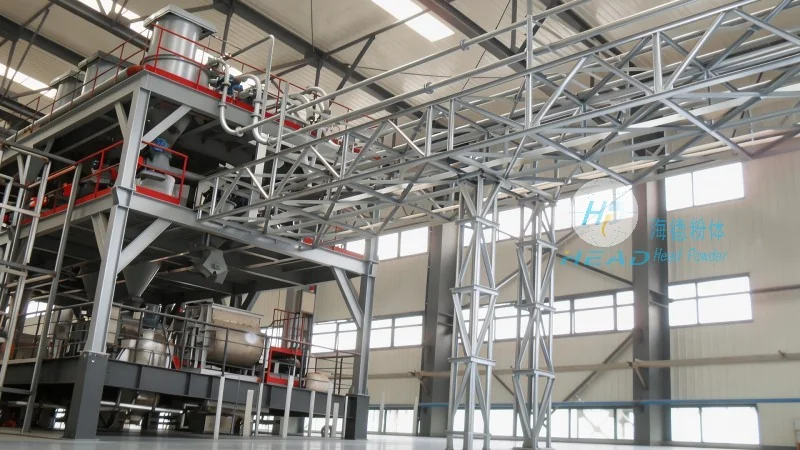
Key Components of the Corn Kernels Powder Conveying System
The corn kernels powder conveying system consists of several key components that work in tandem to ensure optimal performance. The primary components include:
- Hoppers: These are storage containers that hold the corn kernels before they are conveyed. They are designed to accommodate large volumes of material and ensure a steady feed to the conveyor system.
- Conveyors: The core of the system, conveyors are responsible for transporting the corn kernels from the hopper to the processing or packaging area. Different types of conveyors, such as screw conveyors, belt conveyors, or pneumatic conveyors, may be used depending on the specific requirements of the application.
- Control Systems: Advanced control systems are integrated into the equipment to monitor and regulate the conveying process. These systems ensure that the flow rate, pressure, and other parameters are maintained within optimal ranges, preventing issues such as blockages or overloading.
- Feeding Mechanisms: These components are responsible for feeding the corn kernels into the conveyor system. They may include rotary valves, feeders, or other mechanisms that ensure a consistent and controlled flow of material.
Design Principles of the Corn Kernels Powder Conveying System
The design of the corn kernels powder conveying system is based on several fundamental principles aimed at maximizing efficiency, reliability, and safety. The primary design principles include:
- Material Compatibility: The equipment is designed to handle corn kernels without causing damage or degradation to the material. This involves selecting materials for the construction of components that are resistant to corrosion and wear from the corn kernels.
- Efficient Material Flow: The system is engineered to ensure smooth and continuous material flow. This includes optimizing the design of hoppers, conveyors, and feeding mechanisms to minimize friction and resistance, thereby reducing energy consumption and increasing throughput.
- Safety and Reliability: Safety is a top priority in the design of the conveying system. Features such as overload protection, emergency stop mechanisms, and proper sealing are incorporated to prevent accidents and ensure the system operates reliably over long periods.
- Modularity and Flexibility: The system is designed to be modular, allowing for easy customization and adaptation to different production requirements. This flexibility enables businesses to scale their operations and integrate the conveying system with other processing equipment seamlessly.
Applications and Benefits of the Corn Kernels Powder Conveying System
The corn kernels powder conveying system is widely used in various industries due to its versatility and efficiency. Some of the key applications include:
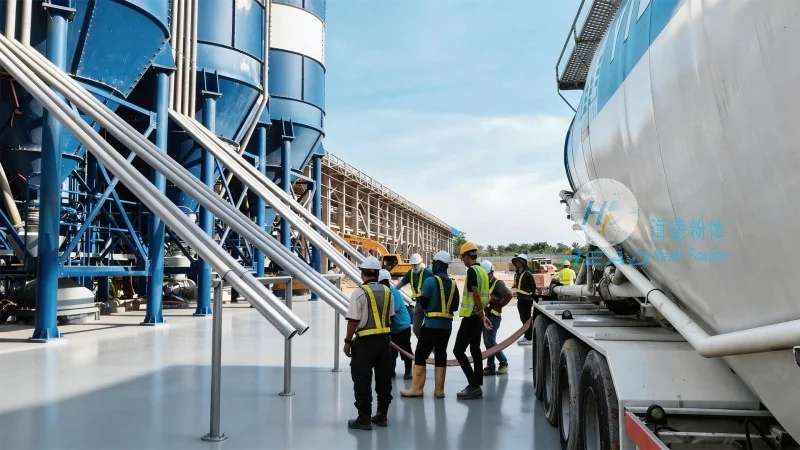
- Food Processing: In the food industry, the system is used to transport corn kernels for processing into products such as corn flour, corn starch, and other food ingredients. Efficient conveying ensures that the material is handled hygienically and without contamination.
- Agricultural Processing: In agricultural settings, the system helps in the processing of corn kernels for animal feed or biofuel production. It enables the smooth transfer of large quantities of corn kernels from storage to processing facilities.
- Chemical Manufacturing: In the chemical industry, the system may be used to transport corn kernels as raw materials for the production of various chemical products. The reliable conveying ensures consistent input to the chemical processing line.
The benefits of using the corn kernels powder conveying system include improved production efficiency, reduced labor costs, enhanced product quality, and increased safety in the workplace. By automating the material handling process, businesses can achieve higher throughput and better control over their operations.
Conclusion
In conclusion, the corn kernels powder conveying system equipment is a critical component in modern industrial operations, particularly in industries dealing with corn kernels. The design principles and components of this system are tailored to ensure efficient, reliable, and safe material handling. With the expertise of manufacturers like Shandong HeadPowder Engineering Co., Ltd., businesses can access high-quality conveying systems that meet their specific needs and contribute to their overall success. The continuous advancement in technology and design ensures that these systems will remain essential tools for efficient production in the future.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
