For industries dealing with bulk materials, efficient and reliable material handling is crucial. A centralized bulk material feeder, often referred to as a bulk material feeding system, plays a pivotal role in streamlining the process of transporting and distributing powders, granules, and other particulate materials. This article explores the concept of centralized bulk material feeders, detailing their design principles and practical applications in various industrial settings.
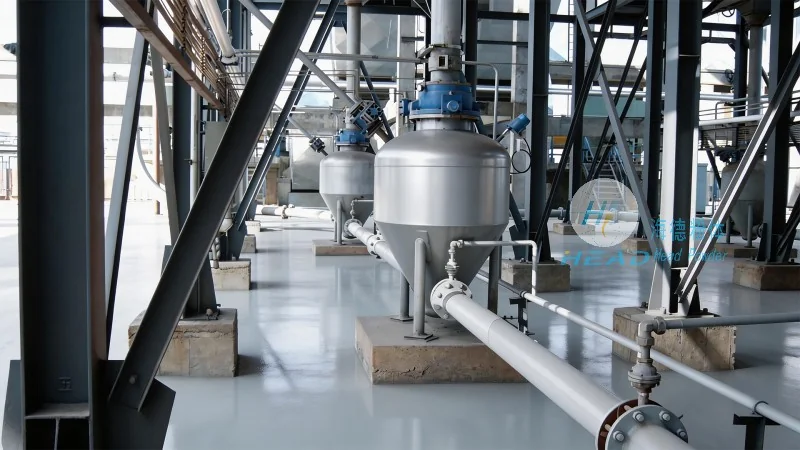
Centralized bulk material feeders are specialized equipment designed to consolidate multiple material sources into a single, controlled feeding system. They are commonly used in manufacturing, pharmaceuticals, food processing, and chemical industries where consistent and precise material flow is essential for production efficiency. The primary goal of such systems is to ensure that raw materials are delivered to processing units in a uniform manner, minimizing variations in feed rate and quality.
The design of a centralized bulk material feeder involves several critical components that work in harmony to achieve optimal performance. These components include:
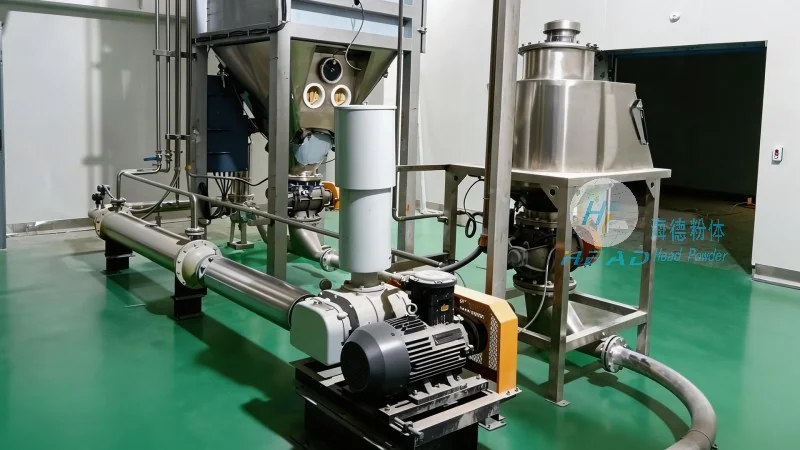
Design principles focus on maximizing efficiency, minimizing material degradation, and ensuring safety. Engineers consider factors such as material properties (e.g., flowability, cohesion), system capacity, and operational environment when designing the feeder. The goal is to create a system that is robust, easy to maintain, and capable of handling a wide range of bulk materials without compromising product quality.
Implementing a centralized bulk material feeder offers several advantages over traditional, decentralized feeding methods. These benefits include:
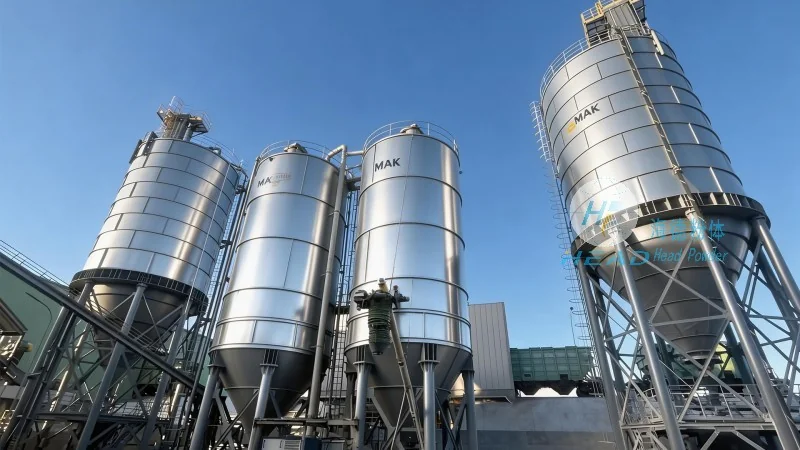
Centralized bulk material feeders are versatile and find applications across multiple sectors. In the pharmaceutical industry, for example, they are used to handle active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring compliance with regulatory standards. In the food processing sector, they are employed to feed raw ingredients like flour, sugar, and spices into production lines, maintaining consistent product quality. Chemical manufacturers also benefit from centralized feeders when handling reactive or hazardous materials, as the system allows for controlled and safe material transfer.
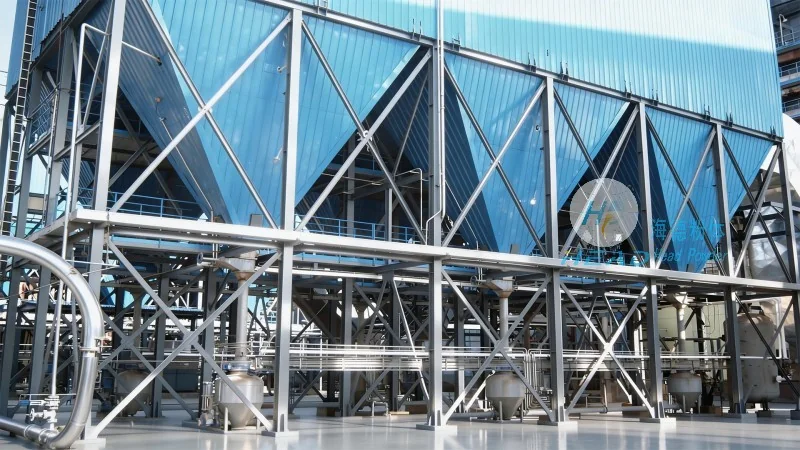
Centralized bulk material feeders are essential equipment for industries that rely on bulk material handling. By understanding the design principles and components of these systems, businesses can optimize their material flow processes, improve efficiency, and maintain product quality. As technology advances, these feeders continue to evolve, incorporating advanced control systems and materials to meet the growing demands of modern manufacturing.
For those seeking reliable bulk material feeding solutions, Shandong HeadPowder Engineering Co., Ltd. offers a range of customized systems tailored to specific industry needs. With a focus on quality and innovation, HeadPowder provides solutions that enhance operational efficiency and ensure consistent material handling in various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top