Diatomaceous earth, a natural, porous sedimentary rock composed of fossilized diatoms, is widely used in various industrial applications due to its unique properties. A diatomaceous earth powder conveyor is a specialized piece of equipment designed to handle and transport this fine powder efficiently. This equipment is crucial for industries that rely on diatomaceous earth, such as filtration, agriculture, and food processing, ensuring consistent and safe material handling.
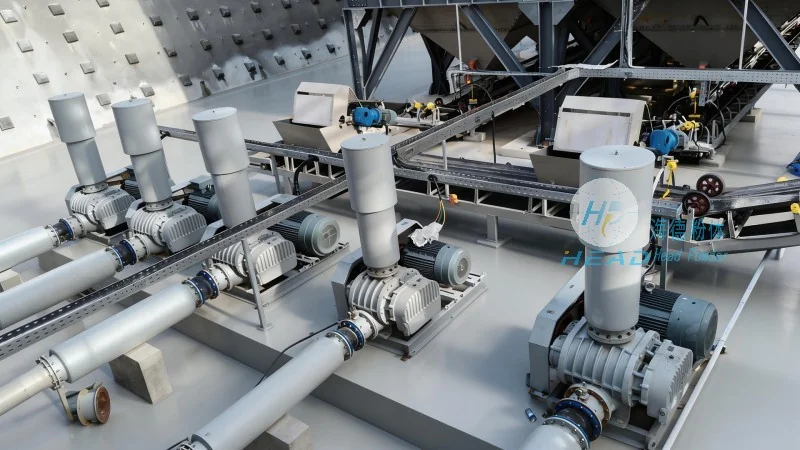
The primary function of a diatomaceous earth powder conveyor is to transport fine, abrasive powders like diatomaceous earth from one location to another within a production facility. These conveyors are engineered to handle materials with high dust content and low bulk density, which can be challenging for traditional conveyor systems. The design must address issues like dust generation, material flow control, and equipment durability, as diatomaceous earth can be abrasive and may cause wear on standard components.
The design of a diatomaceous earth powder conveyor is based on several key principles to ensure optimal performance. First, the system must minimize dust generation and control air flow to prevent contamination and ensure worker safety. This is achieved through enclosed designs and efficient dust collection systems. Second, the conveyor must handle the low bulk density and fine particle size of diatomaceous earth, which requires specialized belt or screw mechanisms that can maintain consistent material flow without clogging. Third, durability is a critical design consideration due to the abrasive nature of the material; components are often made from corrosion-resistant materials like stainless steel or specialized alloys to withstand wear and tear.
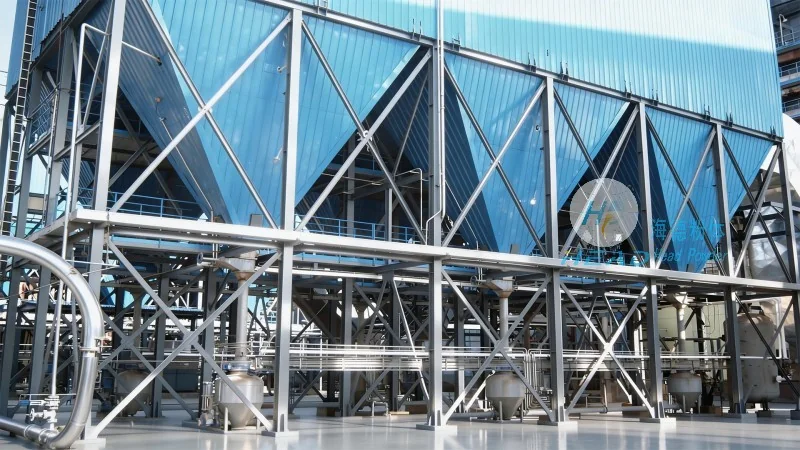
Several key components work together to ensure the efficient operation of a diatomaceous earth powder conveyor. The hopper or feed bin is the initial component where the diatomaceous earth is stored before being fed into the conveyor system. It is designed to hold a sufficient quantity of material and often includes a level indicator to monitor the material level. The feeding mechanism, typically a screw feeder or rotary valve, controls the flow rate of the material into the conveyor, ensuring a consistent feed rate that prevents overloading or underfeeding. The conveyor itself, which may be a belt conveyor or a screw conveyor, transports the material through the system. Belt conveyors are common for horizontal or slight incline applications, while screw conveyors are ideal for vertical or steep incline transport due to their ability to handle fine powders without clogging. The discharge mechanism, such as a rotary valve or a controlled outlet, regulates the release of the material at the end of the conveyor. Finally, the dust collection system, including filters and fans, captures any airborne particles to maintain a clean and safe working environment.
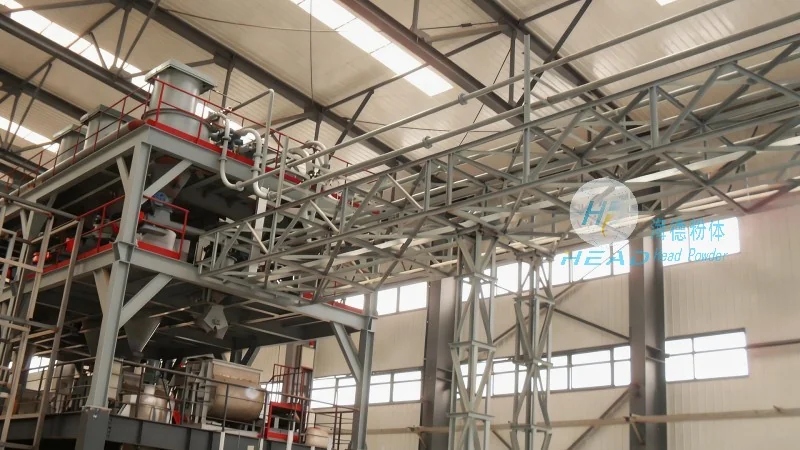
The operational mechanisms of a diatomaceous earth powder conveyor focus on maintaining efficiency and reliability. The feeding mechanism adjusts the material flow rate based on the conveyor's capacity and the downstream processing requirements. The conveyor's speed is controlled to ensure that the material is transported at an optimal rate, avoiding bottlenecks or excessive wear. The system includes sensors and controls to monitor key parameters such as material level, flow rate, and dust levels, allowing for real-time adjustments to maintain performance. Efficiency is also enhanced by the enclosed design, which reduces energy loss and prevents material loss due to dust dispersion. Regular maintenance, including cleaning of components and replacement of worn parts, is essential to maintain the conveyor's efficiency and longevity.
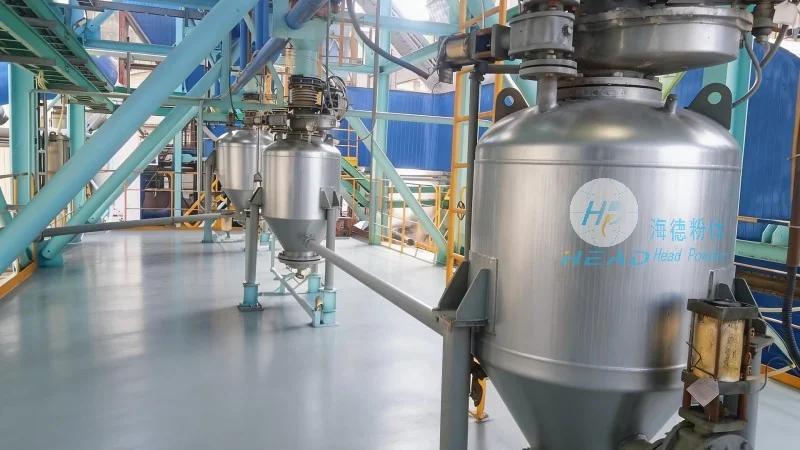
Diatomaceous earth powder conveyors are used in a variety of industries where diatomaceous earth is a key ingredient. In the filtration industry, these conveyors transport diatomaceous earth to filter media production lines, ensuring consistent material supply for water and air filtration systems. In agriculture, they are used to transport diatomaceous earth for pest control products, providing a reliable method to distribute the material to processing facilities. The food processing industry also benefits from these conveyors, as they transport diatomaceous earth used as a food additive or in food packaging applications. Other industries, such as pharmaceuticals and cosmetics, use diatomaceous earth in various products, and the conveyor systems ensure that the material is handled safely and efficiently throughout the production process.
The diatomaceous earth powder conveyor is a critical piece of equipment for industries relying on this versatile material. Its design, based on principles of dust control, material handling, and durability, ensures efficient and safe operation. Companies like Shandong HeadPowder Engineering Co., Ltd., based in China, specialize in manufacturing and supplying such equipment, providing tailored solutions to meet the specific needs of different industries. With a focus on quality and reliability, these conveyors play a vital role in the production processes of various sectors, contributing to the efficient handling and utilization of diatomaceous earth.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top