A centralized powder feeding and conveying line is a sophisticated industrial system engineered to handle, transport, and deliver bulk powders from a central storage or processing point to various destinations within a manufacturing facility. This system is designed to optimize material flow, enhance operational efficiency, and ensure consistent quality control across different production stages. By integrating multiple feeding and conveying mechanisms into a single, coordinated network, such systems eliminate the need for individual, localized feeding solutions, thereby reducing complexity and improving overall process reliability.
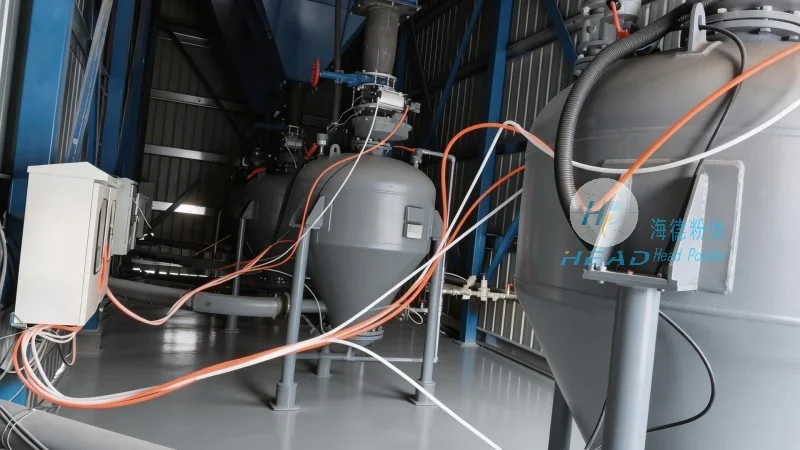
The primary function of a centralized powder feeding and conveying line is to manage the entire lifecycle of bulk powders—from storage and preparation to transport and final discharge. This includes tasks like material weighing, mixing, and transferring, all executed under controlled conditions to prevent contamination, moisture absorption, or degradation of the powder. The system typically operates with automated controls, allowing for precise dosing and consistent delivery, which is crucial in industries such as pharmaceuticals, food processing, and chemical manufacturing where product purity and uniformity are paramount.
The design of a centralized powder feeding and conveying line is governed by several key principles aimed at maximizing efficiency and minimizing operational risks. These principles include:
• Modular Integration: The system is built with modular components that can be easily customized or expanded to meet changing production demands. This flexibility allows manufacturers to adapt to new product lines or increased output without major overhauls.
• Energy Efficiency: Advanced engineering focuses on minimizing energy consumption through optimized airflow, reduced pressure drops, and efficient motor control. This not only lowers operational costs but also aligns with sustainability goals.
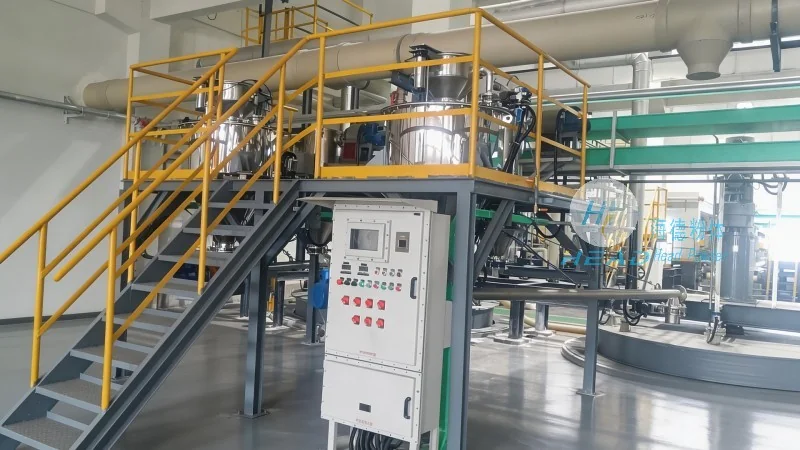
• Material Compatibility: Components are selected based on the specific properties of the powders being handled—such as particle size, moisture content, and chemical reactivity—to ensure compatibility and prevent equipment wear or material degradation.
• Safety and Compliance: The design incorporates safety features, including dust explosion prevention measures, emergency shutdown systems, and compliance with industry standards (e.g., GMP for pharmaceuticals, FDA regulations). This ensures the system operates within regulatory frameworks while protecting personnel and the environment.
A centralized powder feeding and conveying line comprises several critical components, each playing a vital role in the overall operation:
• Feeding Hoppers and Silos: These are large storage vessels designed to hold bulk powders. They are equipped with level sensors and discharge mechanisms to control the flow of material into the system.
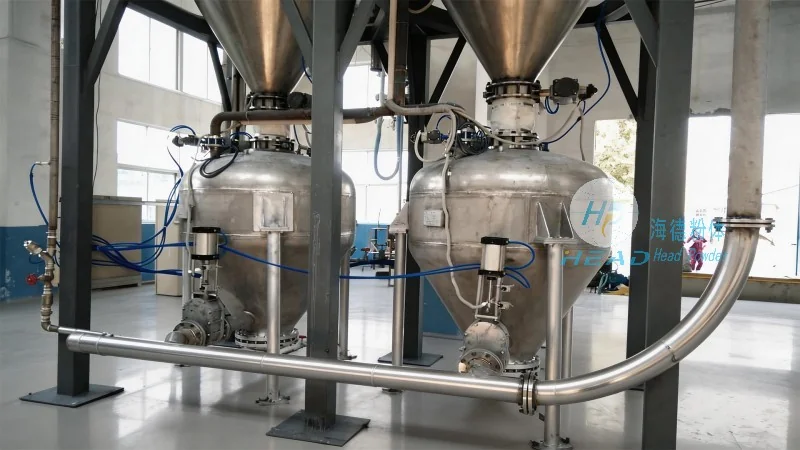
• Conveying Equipment: This includes pneumatic or mechanical conveyors (e.g., rotary valves, screw conveyors, or air slides) that transport the powder from the storage point to the processing or packaging areas. Pneumatic systems use compressed air to move powders, while mechanical systems rely on mechanical motion.
• Dosing and Metering Devices: These components ensure precise control over the amount of powder delivered to each process step. Common devices include gravimetric feeders, volumetric feeders, and loss-in-weight feeders, which maintain consistent material flow rates.
• Control Systems: Integrated PLC (Programmable Logic Controller) or SCADA (Supervisory Control and Data Acquisition) systems manage the entire operation, monitoring parameters like pressure, flow rate, and temperature, and adjusting settings in real-time to maintain optimal performance.
Centralized powder feeding and conveying lines are widely used across various industries due to their ability to handle diverse powder types and meet stringent operational requirements. Some common applications include:
• Pharmaceutical Manufacturing: In this sector, the system ensures that active pharmaceutical ingredients (APIs) and excipients are handled under sterile, controlled conditions, preventing contamination and maintaining batch consistency.
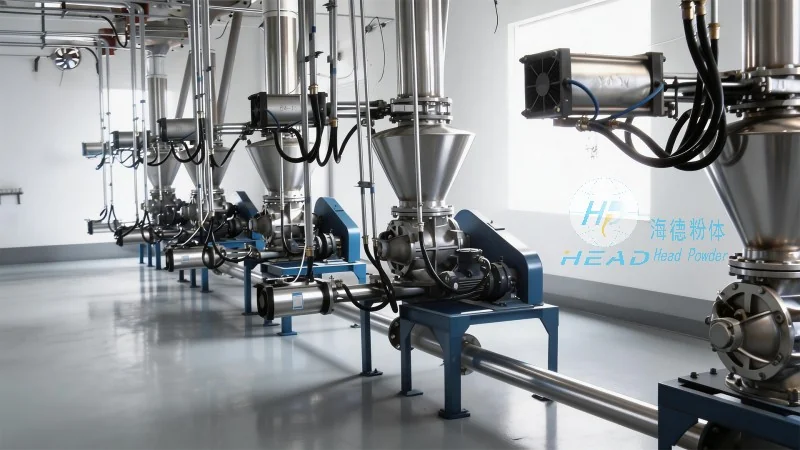
• Food Processing: For food products like flour, sugar, or spices, the system maintains hygiene standards and ensures uniform mixing, which is critical for product quality and consumer safety.
• Chemical and Fertilizer Production: These industries require efficient handling of bulk chemicals and fertilizers, where the system helps manage dust control, material flow, and safety compliance.
• Cement and Construction Materials: The system is used to transport raw materials like limestone and clinker to production lines, optimizing the manufacturing process and reducing downtime.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of centralized powder feeding and conveying systems. With a strong focus on innovation and customer-centric solutions, the company has established itself as a trusted partner in the industrial powder handling sector. HeadPowder's expertise lies in designing and manufacturing customized systems that meet the unique needs of clients, ensuring high performance, reliability, and compliance with industry standards. The company's commitment to quality, safety, and sustainability has earned it a reputation for delivering robust, efficient, and cost-effective powder handling solutions to customers worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top