A nitrogen circulated powder handling system is a specialized industrial solution designed to transport and handle bulk powders in a controlled environment. This system utilizes a closed-loop mechanism where nitrogen gas is used to create a positive pressure or vacuum, enabling the safe and efficient movement of powders without exposure to air. The primary goal is to maintain the integrity of the powder, prevent contamination, and ensure consistent flow characteristics. Such systems are widely used in industries like pharmaceuticals, food processing, and chemical manufacturing, where product purity and process reliability are paramount. HeadPowder, a leading provider of advanced powder handling solutions, specializes in designing and manufacturing these systems tailored to meet the unique needs of various industries. With a focus on innovation and quality, HeadPowder's systems are engineered to deliver reliable performance and enhance operational efficiency. The company, based in Shandong, China, leverages years of expertise in powder technology to develop solutions that address the challenges of modern industrial processes.
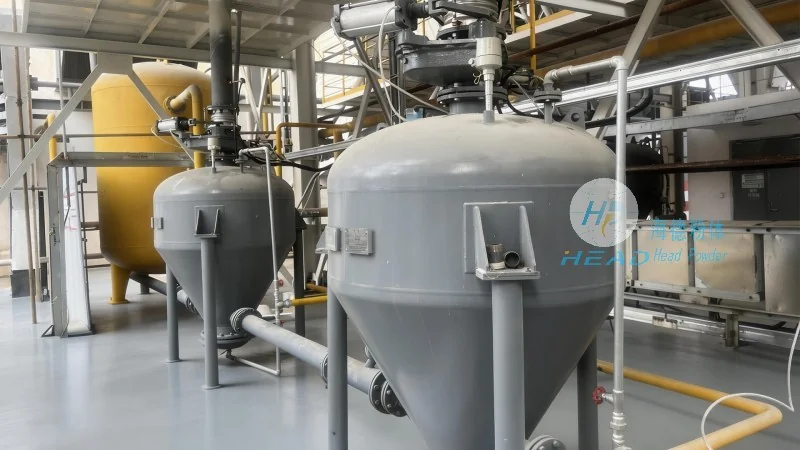
The design of a nitrogen circulated powder handling system is built on several fundamental principles to ensure optimal performance and safety. First, the system employs a sealed pipeline network that isolates the powder from ambient air, thereby preventing oxidation, moisture absorption, or contamination from external sources. The use of nitrogen gas as the conveying medium is critical; it acts as an inert carrier that maintains the powder's properties while providing the necessary pressure differential for movement. Second, the system incorporates advanced control mechanisms, such as variable frequency drives (VFDs) and pressure sensors, to regulate the flow rate and pressure dynamically. This allows for precise control over the powder's velocity and direction, minimizing product degradation and ensuring smooth operation. Third, the system is engineered with robust materials, such as stainless steel and PTFE-coated components, to withstand the corrosive nature of many powders and maintain hygiene standards. Additionally, the design includes features like dust collection and filtration systems to capture any airborne particles, ensuring a clean and safe working environment.
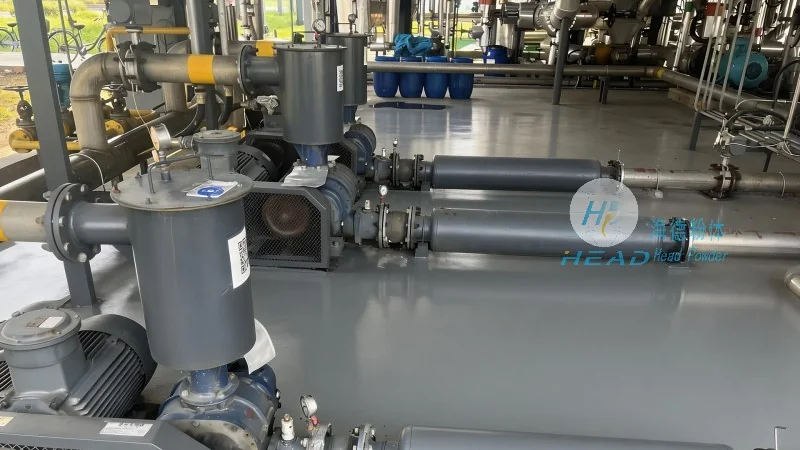
The operation of the nitrogen circulated powder handling system involves a series of coordinated steps that ensure efficient powder transport. The process begins with the loading of the powder into a hopper or silo, where it is stored under a nitrogen blanket to maintain its quality. From there, the powder is drawn into the conveying line using a rotary valve or a venturi system, which creates a pressure differential. The nitrogen gas, introduced at the discharge end, flows backward through the line, carrying the powder particles forward. This creates a positive pressure within the system, preventing air ingress and maintaining the powder's integrity. The system's control panel monitors key parameters, such as pressure, flow rate, and temperature, and adjusts the nitrogen flow or conveyor speed as needed to maintain optimal conditions. The discharge end of the system typically features a filter or cyclone to separate the powder from the nitrogen gas, which is then recirculated back into the system, completing the closed-loop cycle.
Adopting a nitrogen circulated powder handling system offers numerous advantages for industries dealing with sensitive powders. Firstly, it significantly reduces product contamination by eliminating exposure to air, moisture, or other contaminants. This is particularly critical in pharmaceutical and food industries, where product purity directly impacts safety and regulatory compliance. Secondly, the system enhances process efficiency by providing consistent and reliable powder flow, reducing downtime caused by clogging or blockages. The ability to control flow rates precisely allows for better inventory management and reduces waste. Thirdly, the closed-loop design minimizes energy consumption compared to traditional pneumatic systems, as the nitrogen gas is recirculated rather than being vented to the atmosphere. Additionally, the system improves workplace safety by reducing dust emissions and the risk of explosion, as nitrogen is an inert gas that does not support combustion. These benefits make the nitrogen circulated powder handling system a preferred choice for industries seeking to enhance product quality, operational efficiency, and safety.
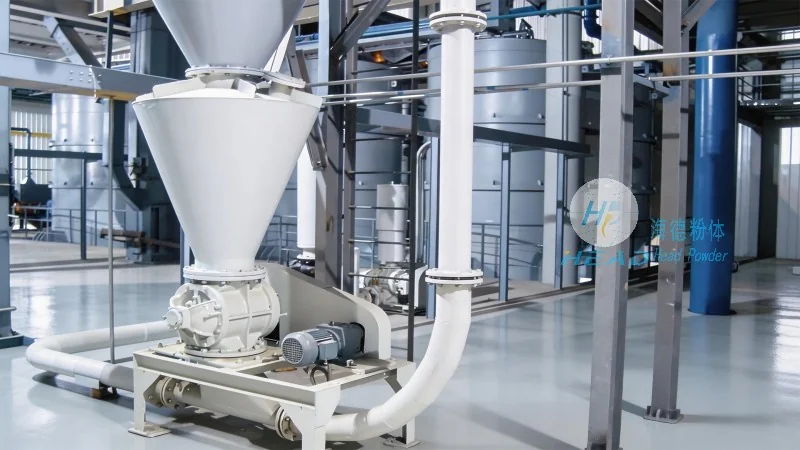
The nitrogen circulated powder handling system is versatile and finds applications across various industries that require the handling of bulk powders. In the pharmaceutical sector, it is used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the final product remains free from contaminants and maintains its potency. The food industry utilizes this system for handling ingredients like flour, sugar, and spices, maintaining freshness and preventing spoilage. In chemical manufacturing, the system is employed to transport reactive powders, such as catalysts and pigments, while preventing unwanted reactions with air. Additionally, the system is used in the cosmetics industry for handling powders like talc and pigments, where color and purity are essential. The adaptability of the nitrogen circulated powder handling system makes it suitable for a wide range of applications, from small-scale laboratory operations to large-scale industrial production lines.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top