Chocolate pneumatic conveying systems are specialized equipment used in the food processing industry, particularly for the efficient and hygienic transport of chocolate and related ingredients. These systems utilize air pressure to move bulk materials through a pipeline network, ensuring a clean and controlled environment that meets stringent food safety standards. As a key component in chocolate production lines, such systems play a crucial role in maintaining product quality and operational efficiency.
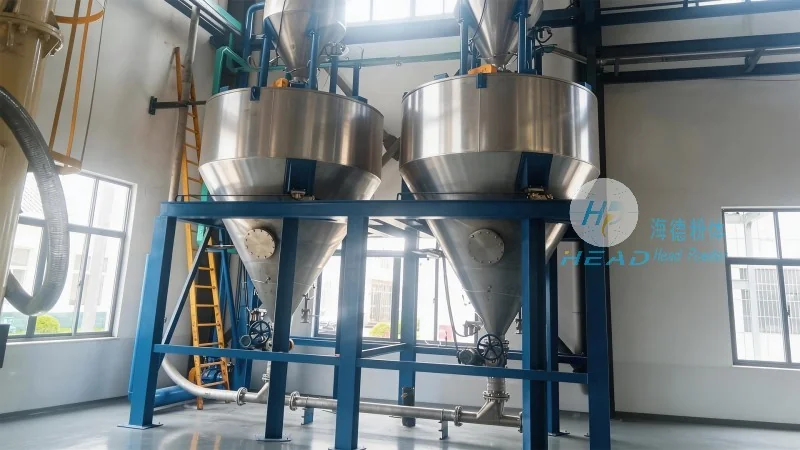
The design of a chocolate pneumatic conveying system is built on several fundamental principles that ensure optimal performance and reliability. The primary mechanism involves creating a pressure differential between the inlet and outlet of the system. By injecting air into the conveying line, the system generates a flow that propels the chocolate particles forward. This process, known as pneumatic conveying, eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and minimizing the risk of contamination.
A critical aspect of the design is the selection of appropriate air velocities and pressure levels. Too low a velocity may cause material settling or blockages, while excessive velocity can lead to wear on the system components and energy inefficiency. Engineers typically calculate the required air velocity based on the density and particle size of the chocolate being conveyed, ensuring that the system operates within safe and efficient parameters. Additionally, the system incorporates features like cyclone separators and filters to separate the chocolate from the air, preventing dust and debris from contaminating the product and the environment.
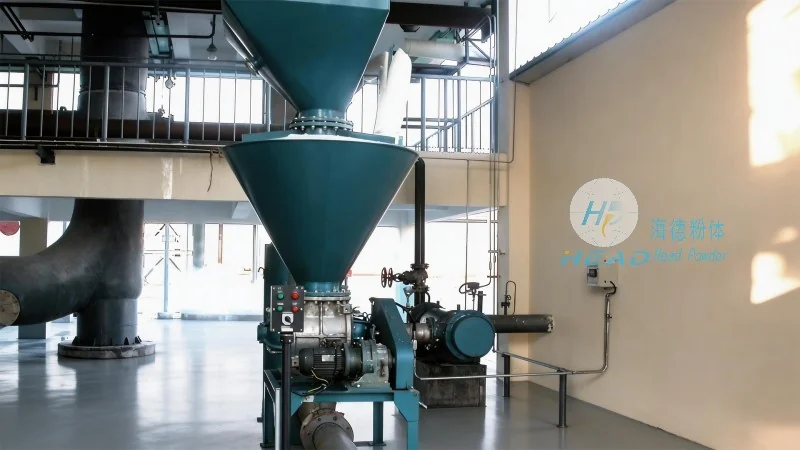
Within the context of chocolate manufacturing, the pneumatic conveying system is integral to the material handling process. It facilitates the movement of raw materials such as cocoa beans, sugar, and milk powders from storage silos to processing units, and also transports finished chocolate products from production lines to packaging areas. The hygienic design of these systems, with smooth, easy-to-clean surfaces and sealed connections, aligns with industry standards like FDA and EU regulations, making them suitable for food-grade applications.
Chocolate pneumatic conveying systems consist of several key components that work in tandem to achieve effective material transport. The main elements include a feed hopper, which holds the chocolate or ingredients and feeds them into the conveying line; a blower or compressor that generates the necessary air pressure; a conveying pipe network that transports the material; and a receiver or discharge hopper where the material is collected. Some systems may also include additional components like rotary valves, which control the flow of material into the system, and cyclone separators, which separate the material from the air stream.
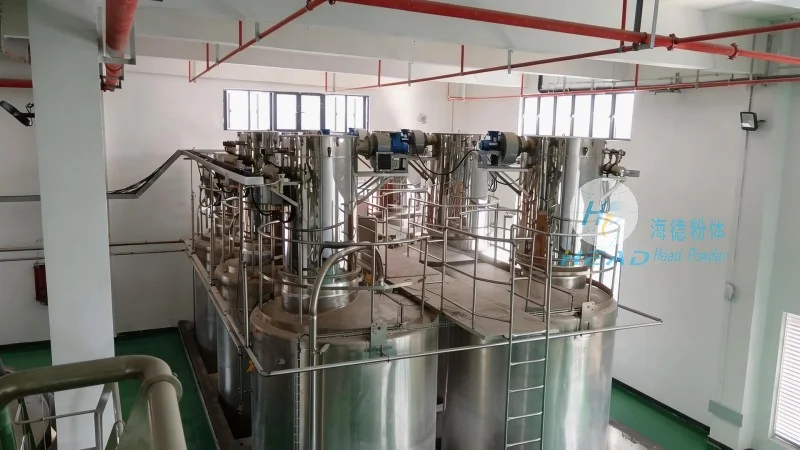
Implementing a chocolate pneumatic conveying system offers several advantages over traditional mechanical conveying methods. First, it provides a hygienic and dust-free environment, which is essential for maintaining the quality and safety of chocolate products. The enclosed system prevents contamination from external sources and reduces the risk of product degradation due to exposure to air or moisture. Second, pneumatic conveying systems are highly flexible, allowing for changes in production volume and layout without significant modifications. This adaptability makes them suitable for both small-scale and large-scale chocolate production facilities. Third, the system reduces labor costs by automating the material handling process, minimizing the need for manual labor in transporting heavy or bulky materials. Finally, the energy efficiency of pneumatic conveying systems, particularly when using low-pressure or vacuum systems, contributes to lower operational costs over time.
Chocolate pneumatic conveying systems are widely used in various stages of chocolate production. In the initial stages, they transport raw ingredients from storage to the grinding and mixing units. During the processing phase, they move the chocolate mass from the mixing tanks to the tempering and molding equipment. In the final stages, they convey finished chocolate products from the production line to the packaging and storage areas. The versatility of these systems allows them to handle different types of chocolate, including dark, milk, and white chocolate, as well as various fillings and toppings.
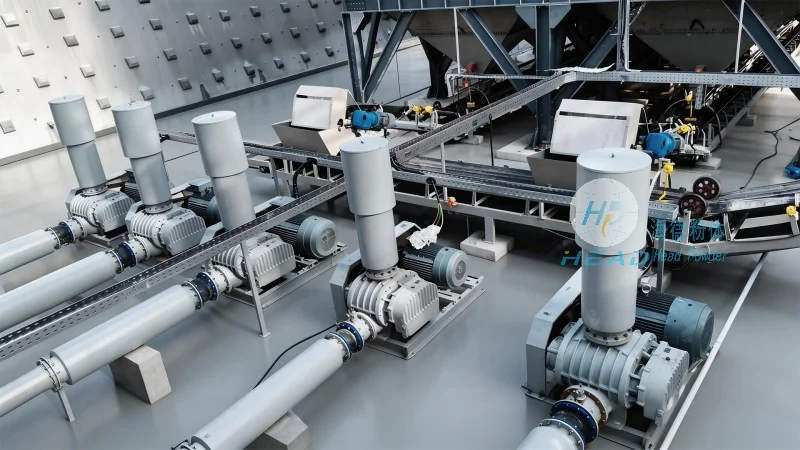
Proper maintenance is crucial to ensure the longevity and efficiency of a chocolate pneumatic conveying system. Regular cleaning of the conveying lines, filters, and cyclone separators is necessary to prevent clogging and maintain air flow. Additionally, checking the blower or compressor for proper operation and replacing worn parts, such as seals and bearings, helps to avoid system failures. Operational considerations also include monitoring air pressure and flow rates to ensure the system is running at optimal levels. By adhering to a regular maintenance schedule and following operational guidelines, manufacturers can maximize the performance and lifespan of their chocolate pneumatic conveying systems.
Chocolate pneumatic conveying systems represent an advanced solution for the efficient and hygienic handling of chocolate and related ingredients in food processing. By leveraging the principles of pneumatic conveying, these systems offer numerous benefits, including improved product quality, reduced contamination risk, and enhanced operational flexibility. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality chocolate pneumatic conveying systems tailored to the specific needs of chocolate manufacturers. With a focus on hygiene, efficiency, and reliability, HeadPowder ensures that their systems meet the stringent requirements of the food industry, supporting the production of safe and delicious chocolate products.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top