Sugar, a fundamental ingredient in the food industry and a key raw material in numerous manufacturing processes, often requires efficient and reliable transportation from storage to processing units. This is where sugar pneumatic conveying equipment emerges as a solution, offering a blend of functionality and operational efficiency. In this article, we will explore what sugar pneumatic conveying equipment is and delve into the design principles that underpin its effective operation.
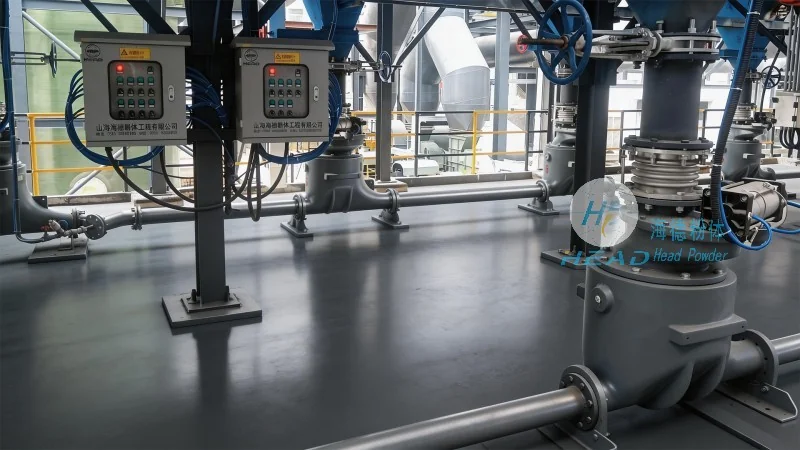
Sugar pneumatic conveying equipment is a system engineered to transport bulk sugar through a pipeline using air or other gases as the conveying medium. Unlike traditional mechanical conveyors, which rely on mechanical components such as belts or screws, pneumatic systems utilize the force of compressed air to move the material. This method is particularly advantageous for sugar, as it minimizes product contamination, reduces handling costs, and enhances overall process safety. The equipment typically comprises several key components, including a hopper for material storage, a feeder to control the flow of sugar, a conveying line where the sugar is propelled by air, and a receiver to collect the material at the destination. These components work in concert to ensure a smooth and continuous transfer of sugar from one location to another.
The design of a sugar pneumatic conveying system is governed by several critical principles that ensure optimal performance and durability. First, the system must be tailored to handle the specific physical properties of sugar, such as its particle size, moisture content, and flow characteristics. Sugar particles can vary in size, and the conveying system must accommodate these variations without causing blockages or excessive wear on components. The design also considers the moisture content of the sugar, as high moisture levels can lead to caking or clumping, which can impede the conveying process. To mitigate this, the system may incorporate drying or conditioning steps to ensure the sugar remains in a free-flowing state.
Second, the system's pressure and airflow requirements are meticulously calculated to maintain the desired conveying velocity. The velocity of the air must be sufficient to lift and transport the sugar particles without causing excessive abrasion or degradation of the material. This balance is crucial for preserving the quality of the sugar, which is essential for its end-use applications. The design also accounts for the length and layout of the conveying line, as these factors impact the overall pressure drop and energy consumption of the system. Proper sizing of the pipeline, along with the use of appropriate fittings and valves, helps minimize energy losses and ensures consistent performance.
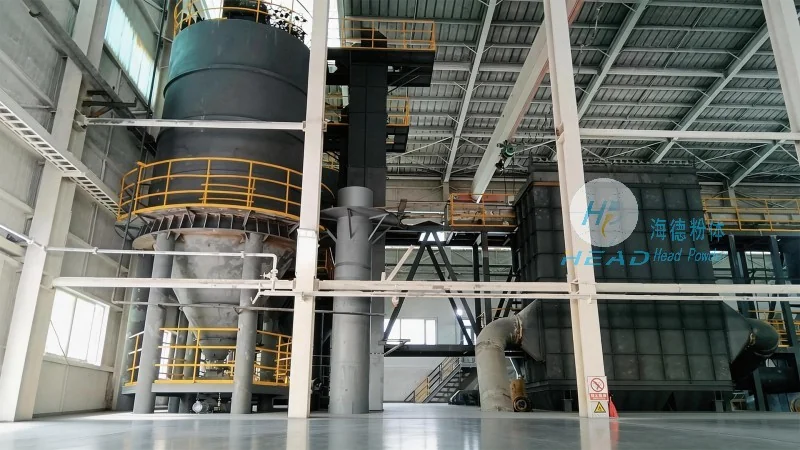
Each component of the sugar pneumatic conveying system plays a vital role in its overall functionality. The hopper, often equipped with a discharge valve or a rotary valve, serves as the primary storage unit for the sugar. It is designed to maintain a consistent material level and prevent the formation of bridging or rat-holing, which can disrupt the feeding process. The feeder, typically a rotary valve or a screw feeder, controls the rate at which sugar is introduced into the conveying line. This component is critical for maintaining a steady flow rate, which is essential for preventing surges or backflow in the system. The conveying line itself is usually made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of sugar particles and to prevent contamination. The line is equipped with pressure sensors and flow meters to monitor the system's performance and ensure that the conveying process is operating within the desired parameters.
Air is the primary driving force in a sugar pneumatic conveying system, and its properties are carefully managed to ensure efficient operation. The air is typically compressed and then introduced into the conveying line at a controlled pressure. The pressure and volume of the air are adjusted based on the material being conveyed and the distance it needs to travel. The system may also incorporate air filtration and drying equipment to ensure that the air used is clean and dry, preventing moisture from being introduced into the sugar and causing caking or other issues. The use of air as the conveying medium also allows for the integration of additional features, such as dust collection systems, which help maintain a clean and safe working environment.
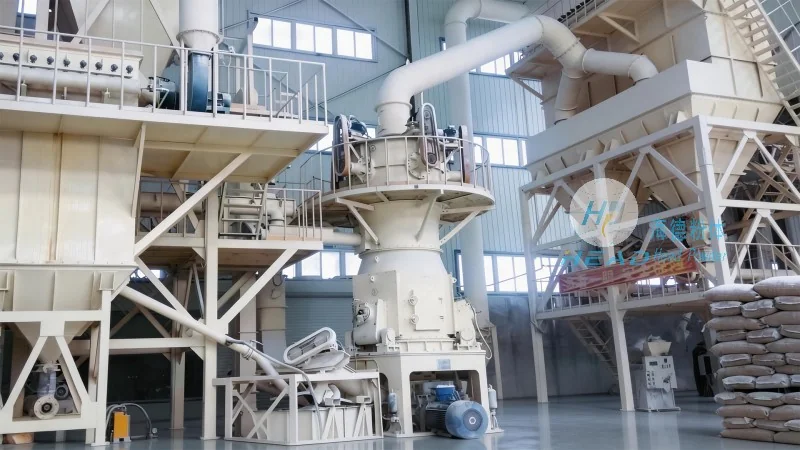
There are several advantages to using sugar pneumatic conveying equipment in industrial settings. One of the most significant benefits is the reduction in labor costs, as the system automates the material handling process, eliminating the need for manual handling of bulk sugar. This not only improves efficiency but also enhances workplace safety by reducing the risk of accidents associated with manual handling. Another advantage is the reduction in product contamination, as the system is enclosed and uses clean air to transport the material. This is particularly important for sugar, which is used in food and pharmaceutical applications where product purity is paramount. Additionally, the system offers flexibility in terms of layout, as the conveying line can be easily reconfigured to accommodate changes in production processes or facility expansions.
Sugar pneumatic conveying systems are widely used in various industries, including food processing, pharmaceutical manufacturing, and chemical processing. In the food industry, these systems are commonly used to transport sugar from storage silos to processing lines, such as those used for making confectionery, beverages, or baked goods. In pharmaceutical applications, the system is used to transport sugar into mixing and blending equipment, where it is combined with other ingredients to form final products. The systems are also used in chemical processing facilities to transport sugar as a raw material for the production of various chemical compounds. Regardless of the application, the primary goal is to ensure that the sugar is transported efficiently and safely, without compromising its quality or integrity.
Sugar pneumatic conveying equipment is a vital component in the modern industrial landscape, offering a reliable and efficient solution for the transportation of bulk sugar. The design principles that govern these systems are carefully considered to ensure optimal performance, durability, and product quality. By understanding the key components and design principles, manufacturers can select and implement the most suitable system for their specific needs. As the demand for efficient and safe material handling continues to grow, sugar pneumatic conveying equipment will remain a critical technology in the food and related industries. With proper design and maintenance, these systems can provide long-term operational benefits and contribute to the overall success of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top