Multi-functional pneumatic conveying systems represent a sophisticated approach to material handling, offering versatility and efficiency in transporting various bulk materials. These systems utilize air or gas as the conveying medium to move powders, granules, and other particulate materials from one location to another. The technology has evolved significantly over the years, providing solutions for diverse industrial applications ranging from food processing to chemical manufacturing. By integrating advanced engineering principles and innovative design, these systems enable industries to streamline their material transport processes, reduce downtime, and enhance overall operational efficiency.
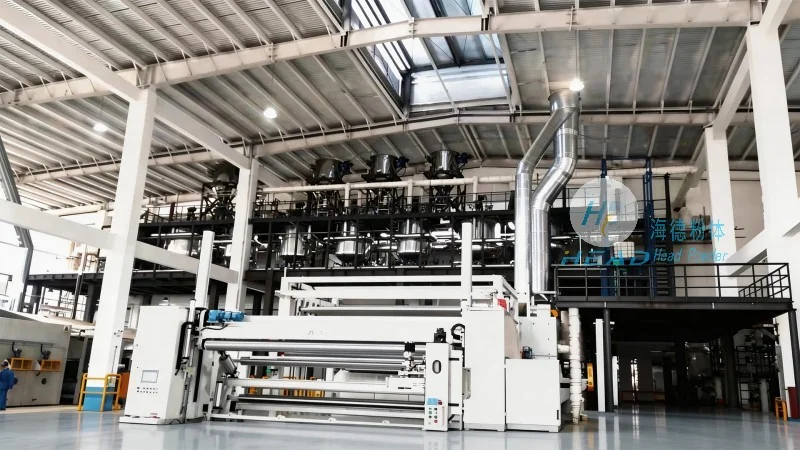
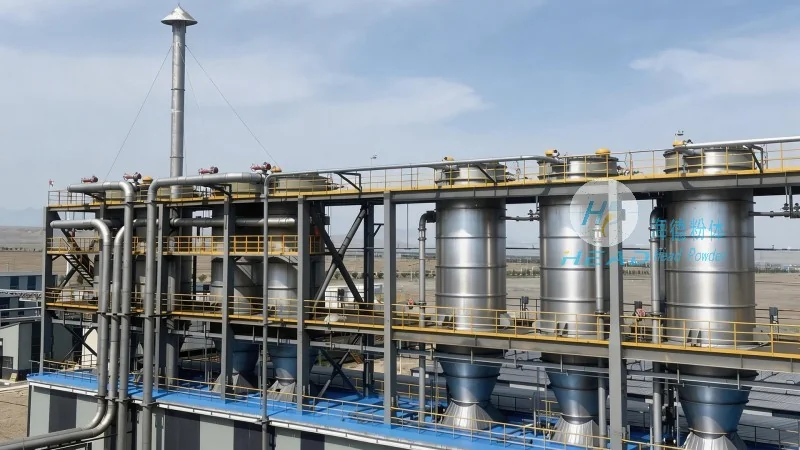
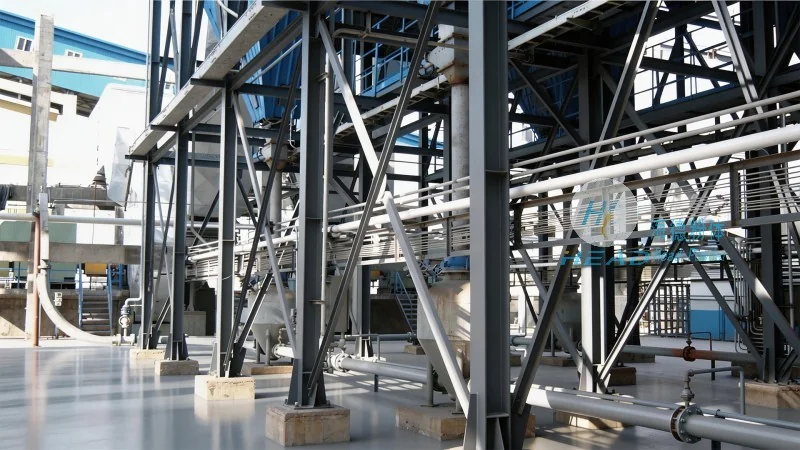
The design of a multi-functional pneumatic conveying system is built on several key principles that ensure optimal performance, reliability, and adaptability. First, the system must be capable of handling a wide range of material properties, including different particle sizes, densities, and flow characteristics. This is achieved through the integration of various components such as feeders, ducts, and separation equipment. Second, the system is designed to operate under different pressure conditions, typically categorized as low-pressure, medium-pressure, or high-pressure systems. Low-pressure systems use air as the primary conveying medium and are suitable for short distances and low material loads. Medium-pressure systems combine air and gas to enhance conveying efficiency, while high-pressure systems utilize compressed air to achieve longer distances and higher material throughput. Third, the system incorporates advanced control mechanisms to regulate the flow of material and air, ensuring consistent and stable operation. This includes sensors and control valves that monitor pressure, flow rate, and material level, allowing for real-time adjustments to maintain optimal performance. Additionally, the design emphasizes energy efficiency by minimizing air consumption and maximizing material transport efficiency. The integration of these principles results in a system that can adapt to changing operational requirements, making it suitable for dynamic industrial environments. For instance, in food processing facilities, multi-functional pneumatic conveying systems are used to transport ingredients like flour and sugar with minimal risk of contamination, while in chemical plants, they handle hazardous materials safely and efficiently.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of advanced pneumatic conveying solutions, headquartered in Shandong, China. With years of experience in the industry, the company specializes in designing, manufacturing, and installing multi-functional pneumatic conveying systems tailored to meet the specific needs of various industries. The company's commitment to quality and innovation has enabled it to deliver reliable and efficient solutions that enhance productivity and reduce operational costs for its clients. HeadPowder Engineering leverages cutting-edge technology and rigorous quality control processes to ensure that each system meets the highest standards of performance and durability. The company's team of experienced engineers and technicians provides comprehensive support, from initial consultation and system design to installation and after-sales service, ensuring that clients receive end-to-end solutions that address their material handling challenges effectively. The company's facilities in Shandong are equipped with state-of-the-art manufacturing equipment and testing facilities, allowing for the production of high-quality components and systems that meet international standards. HeadPowder Engineering also invests in research and development to stay ahead of industry trends, continuously improving its product offerings to provide the best possible solutions for its customers.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top