Efficient material handling is a critical factor in the production and distribution of soap granules. Pneumatic conveying systems have emerged as a reliable and effective solution for transporting these granules from one location to another within industrial settings. This article delves into the fundamental principles behind such systems, highlighting their design, operation, and key benefits for manufacturers.
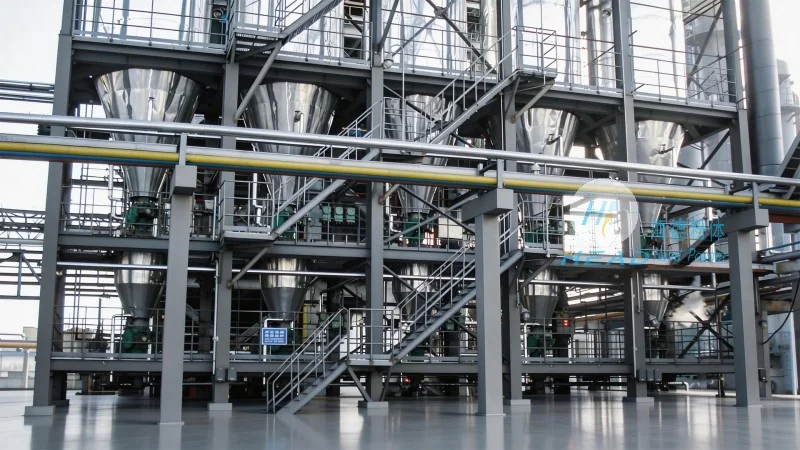
A pneumatic conveying system for soap granules typically consists of several key components that work in tandem to ensure smooth and efficient material transport. The primary elements include a hopper or feed bin for storing the soap granules, a conveying line (often made of metal or flexible tubing), a blower or air compressor to generate the necessary airflow, and a receiver or discharge hopper where the material is deposited. Each component plays a vital role in the overall functionality of the system.
The core mechanism of a pneumatic conveying system relies on the use of compressed air to move the soap granules through the conveying line. When the blower operates, it creates a pressure differential between the inlet and outlet of the system. The soap granules are introduced into the conveying line, either by gravity or by a feeder mechanism, and are then entrained by the airflow. As the air flows through the line, it lifts and transports the granules, maintaining them in a suspended state until they reach the discharge point. The velocity and pressure of the air are carefully controlled to ensure that the granules are conveyed without excessive wear or degradation.
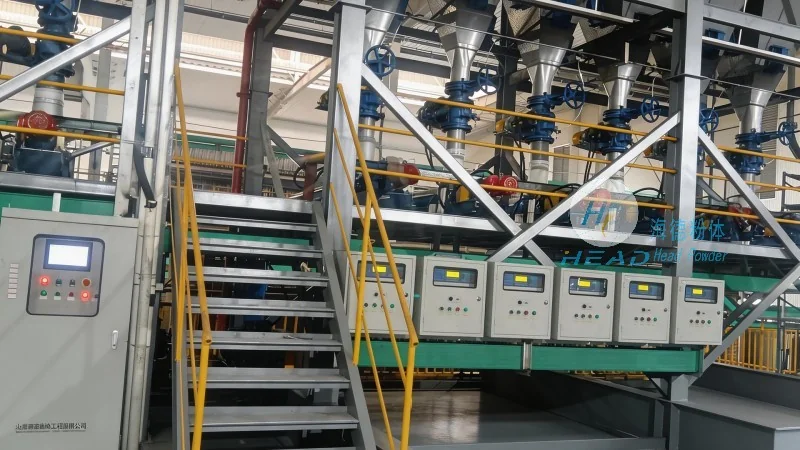
Implementing a pneumatic conveying system for soap granules offers numerous advantages over traditional methods like belt conveyors or manual handling. One of the most significant benefits is the ability to handle the material in a closed system, which helps maintain hygiene and prevent contamination. This is particularly important in the soap manufacturing industry, where product purity is paramount. Additionally, pneumatic systems are highly flexible, allowing for easy integration into existing production lines and the ability to transport materials over long distances or through complex layouts without the need for multiple transfer points.
The effectiveness of a pneumatic conveying system for soap granules depends on careful design and customization to match the specific characteristics of the material and the operational requirements of the facility. Factors such as the size, density, and moisture content of the soap granules, as well as the distance and layout of the conveying path, must be considered during the system design phase. Engineers from Shandong HeadPowder Engineering Co., Ltd. specialize in tailoring pneumatic conveying solutions to meet these specific needs, ensuring optimal performance and minimal downtime.
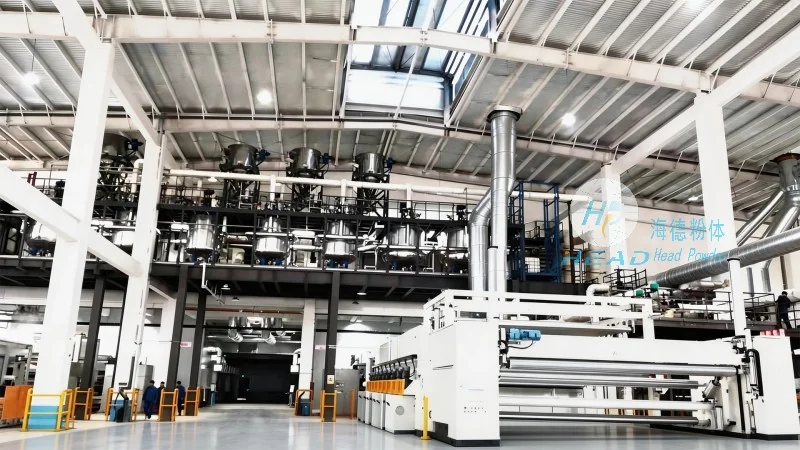
Pneumatic conveying systems are widely used in various stages of soap granule production, from raw material handling to finished product packaging. They are particularly beneficial in facilities that require high throughput and consistent material flow, such as large-scale soap manufacturing plants. By streamlining the material handling process, these systems contribute to increased productivity, reduced labor costs, and improved overall operational efficiency.
As the soap manufacturing industry continues to evolve, the importance of efficient and reliable material handling systems cannot be overstated. Pneumatic conveying systems, with their ability to handle soap granules with precision and care, represent a significant advancement in industrial material transport. Companies like Shandong HeadPowder Engineering Co., Ltd., with their expertise in engineering and design, play a crucial role in providing tailored solutions that enhance the productivity and quality of soap production processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top