Calcium carbonate, a widely used industrial material, is often transported using pneumatic conveying systems. These systems offer efficient and flexible solutions for moving bulk materials like calcium carbonate, which is essential in various industries including construction, plastics, and paper manufacturing. Understanding the types, key features, and application ranges of calcium carbonate pneumatic conveying is crucial for optimizing material handling processes and ensuring operational efficiency.
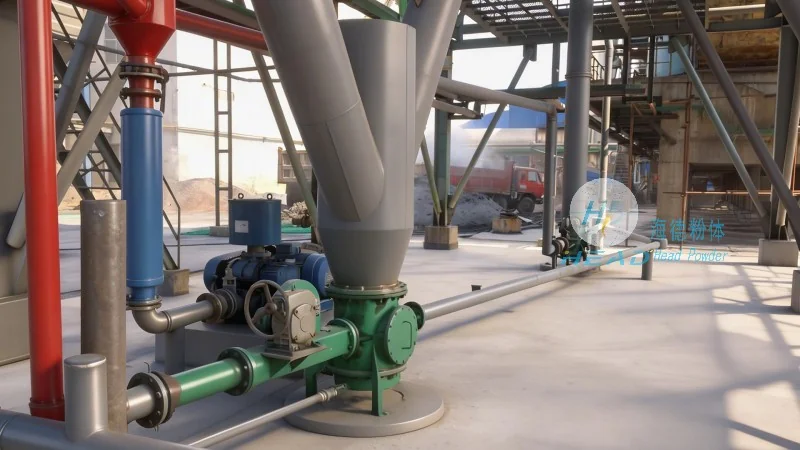
Calcium carbonate (CaCO₃) is a common mineral used as a filler or extender in many industrial applications. Its transportation requires specialized equipment to handle the material's properties, such as its fine particle size and potential for dust generation. Pneumatic conveying systems are preferred for calcium carbonate due to their ability to transport dry powders over long distances with minimal loss and contamination. This method involves using air or gas to move the material through a pipeline, making it an ideal choice for industries that demand high purity and consistent material flow.
There are several types of pneumatic conveying systems designed for calcium carbonate, each with distinct characteristics and operational principles. The primary categories include pressure, vacuum, and mixed flow systems, which are selected based on the application requirements, material characteristics, and system layout.
Pressure conveying systems operate by injecting compressed air or gas into the material stream at the loading point. This method is suitable for short to medium-distance transport and is commonly used when the material needs to be conveyed from a storage silo or hopper to a processing unit. The pressure system ensures that the material is moved efficiently without the need for vacuum pumps, making it cost-effective for applications where the conveying distance is relatively short. In pressure systems, the air is introduced at high pressure, creating a positive pressure environment that pushes the material through the pipeline. This approach is particularly effective for calcium carbonate with a relatively low moisture content and non-abrasive properties, as it minimizes the risk of material degradation during transport.
Vacuum conveying systems, on the other hand, use a vacuum pump to create a negative pressure that draws the material from the source to the destination. This method is ideal for longer distances and when the material needs to be transported from multiple points or from a low-level source. Vacuum systems are often preferred in applications where the material is sensitive to pressure changes or where the conveying distance exceeds the capabilities of pressure systems. The vacuum approach allows for gentle handling of the material, reducing the risk of particle breakage and maintaining the material's quality. For calcium carbonate, vacuum systems are commonly used in industries such as paper manufacturing, where the material is transported from a storage area to a mixing or coating unit. The system typically includes a vacuum receiver, a filter, and a blower, which work together to create the necessary suction force and ensure efficient material transport.
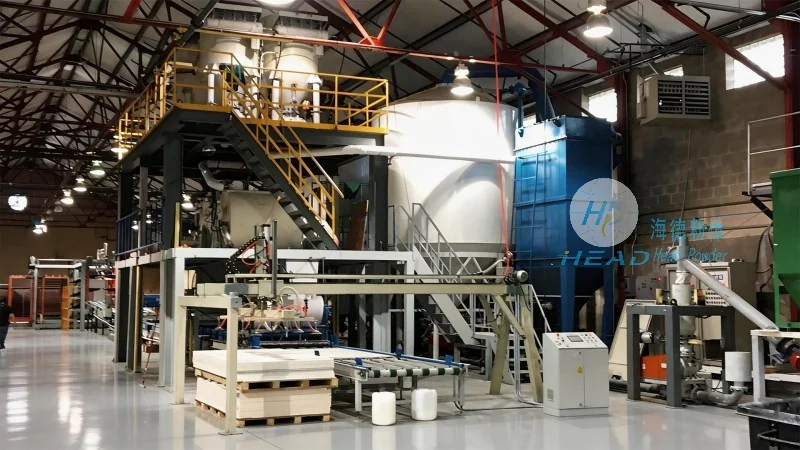
Mixed flow systems combine elements of both pressure and vacuum conveying, offering a versatile solution for various calcium carbonate applications. These systems are designed to handle both short and long distances, as well as different material characteristics. In mixed flow, the conveying medium (air or gas) is introduced at a moderate pressure, creating a flow that is neither purely positive nor negative. This approach is beneficial when the system needs to accommodate varying material loads or when the distance is intermediate. Mixed flow systems are often used in industrial settings where the material is transported from multiple sources to a central processing facility. The flexibility of mixed flow allows for efficient material handling while maintaining the material's integrity and preventing dust accumulation in the pipeline.
Regardless of the system type, calcium carbonate pneumatic conveying systems share several key features that contribute to their effectiveness and reliability. These features include high material transport efficiency, minimal material loss, and the ability to handle fine powders without clogging or blockages. The systems are designed to maintain the material's purity by using filters and separation equipment to remove any entrained air or dust particles. This ensures that the calcium carbonate reaches its destination in the desired form, without contamination or degradation.
The application ranges of calcium carbonate pneumatic conveying systems are broad and cover various industries that rely on this material. The systems are commonly used in the following sectors:
In the construction industry, calcium carbonate is used as a filler in cement, concrete, and plaster products. Pneumatic conveying systems are employed to transport the material from storage silos to production lines, ensuring a consistent supply of high-quality calcium carbonate. The systems are designed to handle large volumes of material, often over long distances, and maintain the material's particle size distribution. This is crucial for achieving the desired strength and durability of construction materials. The pressure and vacuum systems are both used in this industry, with pressure systems preferred for shorter distances and vacuum systems for longer or more complex layouts.
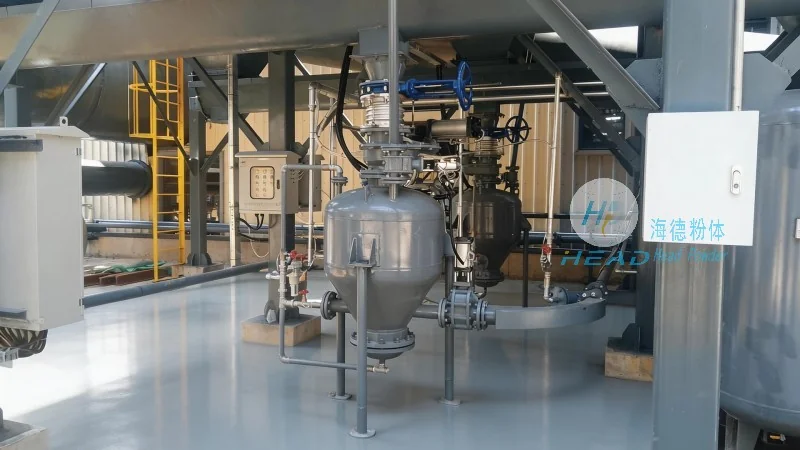
The plastics and rubber industry utilizes calcium carbonate as a cost-effective filler to improve the mechanical properties of products such as PVC pipes, rubber tires, and plastic films. Pneumatic conveying systems are essential for transporting the material from bulk storage to mixing and extrusion units. The systems must be capable of handling fine powders and maintaining the material's purity, as any contamination can affect the final product's quality. Mixed flow systems are often used in this industry due to their ability to handle varying material loads and distances. The systems are designed to ensure that the calcium carbonate is evenly distributed in the plastic matrix, enhancing the product's strength and reducing manufacturing costs.
In the paper manufacturing industry, calcium carbonate is used as a coating and filler in paper products. Pneumatic conveying systems are used to transport the material from storage areas to the coating and drying units. The systems are required to handle fine powders and maintain the material's consistency, as the coating process demands a uniform material supply. Vacuum conveying systems are commonly used in this industry, as they provide gentle handling and prevent particle breakage. The systems are equipped with filters and separation equipment to ensure that the calcium carbonate reaches the coating unit in the desired form, without any dust or air entrainment. This contributes to the production of high-quality paper products with improved brightness and surface smoothness.
The chemical industry uses calcium carbonate in various applications, including as a filler in coatings, adhesives, and sealants. Pneumatic conveying systems are employed to transport the material from bulk storage to processing units, ensuring a continuous supply of high-purity calcium carbonate. The systems are designed to handle different material characteristics, such as varying moisture content or particle size, and maintain the material's quality throughout the transport process. Pressure and vacuum systems are both utilized in this industry, depending on the specific application requirements. The systems are equipped with specialized components, such as cyclone separators and filters, to ensure that the material is transported efficiently and without contamination.
Calcium carbonate pneumatic conveying systems offer efficient and reliable solutions for transporting this essential industrial material. The various types of systems, including pressure, vacuum, and mixed flow, are designed to meet the specific needs of different industries and applications. The key features of these systems, such as high transport efficiency and minimal material loss, contribute to improved operational performance and cost savings. By understanding the types, features, and application ranges of calcium carbonate pneumatic conveying, industries can optimize their material handling processes and enhance overall productivity. The systems are a critical component in the supply chain for calcium carbonate, ensuring that the material is delivered in the desired form and quality for various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top