HeadPowder, a leading provider of material handling solutions, specializes in advanced pneumatic conveying systems tailored for the efficient and safe delivery of magnesium sulfate. This article explores the various types of pneumatic conveying systems and their practical applications in industrial settings, particularly focusing on the unique requirements of magnesium sulfate handling.
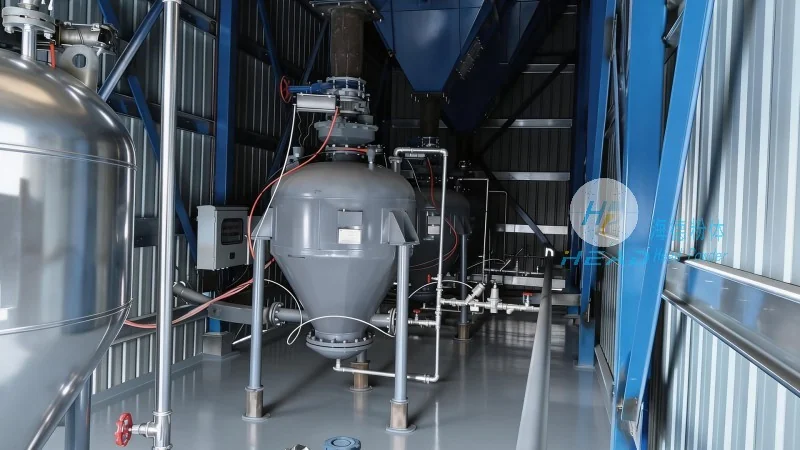
Pneumatic conveying systems utilize air or gas to transport bulk materials like magnesium sulfate through a pipeline network. These systems are categorized into two primary types: positive pressure and negative pressure systems. Positive pressure systems generate air pressure above atmospheric levels to push material through the pipeline, while negative pressure systems create a vacuum to draw material into the system. Each type offers distinct advantages depending on the application's specific needs, such as material characteristics, distance, and environmental considerations.
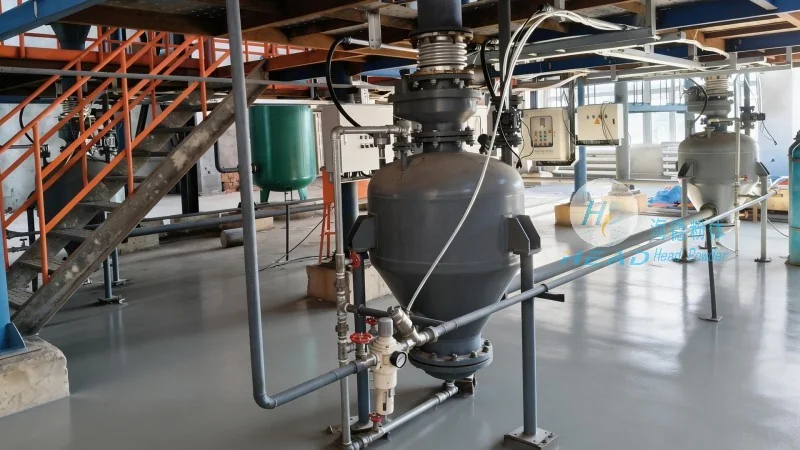
For magnesium sulfate, which is often handled as a fine powder or granules, several specialized pneumatic conveying solutions are commonly employed. One key system is the positive pressure dilute phase system, which is ideal for long-distance transport and high material throughput. This system uses high-pressure air to propel material through the pipeline, ensuring consistent flow and minimal product degradation. Another effective option is the negative pressure dense phase system, which operates at lower velocities and higher material concentrations, reducing the risk of material degradation and ensuring precise control over the delivery process. Additionally, combination systems that integrate both positive and negative pressure components are used for complex material handling scenarios, such as multi-stage transport or material transfer between different processing units.
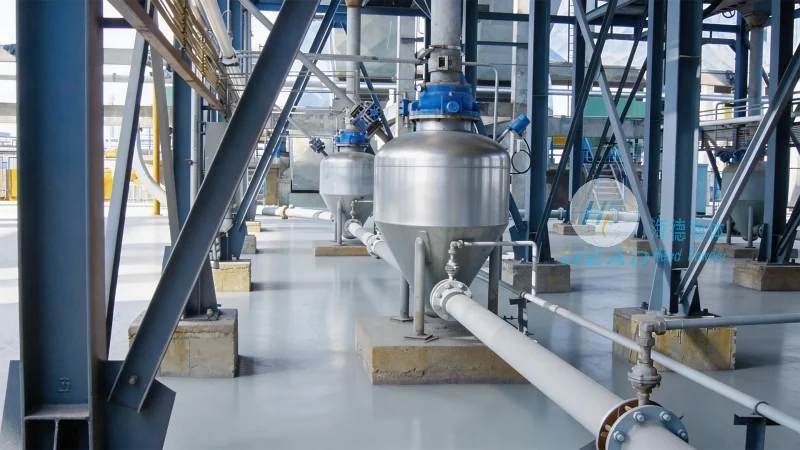
The practical application of pneumatic conveying systems for magnesium sulfate delivery is widespread across various industries, including chemical manufacturing, pharmaceutical production, and food processing. In chemical plants, these systems are crucial for transferring magnesium sulfate from storage silos to processing reactors, ensuring a continuous and controlled supply of raw material. The systems' ability to handle fine powders without clogging or degradation makes them particularly suitable for sensitive applications, such as the production of magnesium sulfate heptahydrate, a key ingredient in agricultural fertilizers and water treatment chemicals. In pharmaceutical facilities, the hygienic design of pneumatic conveying systems allows for the safe and sterile transfer of magnesium sulfate, which is used in the formulation of various medications and supplements. The systems' flexibility also enables integration with existing production lines, minimizing downtime and enhancing operational efficiency.
Compared to traditional mechanical conveying methods, pneumatic conveying systems offer several advantages when handling magnesium sulfate. First, they provide a closed system that prevents dust contamination and product loss, which is critical for maintaining product quality and compliance with environmental regulations. Second, the systems are highly efficient in terms of energy consumption, especially when operating at optimal pressure and flow rates. This efficiency translates to lower operational costs and reduced environmental impact. Third, pneumatic conveying systems offer greater flexibility in terms of material transport, allowing for vertical, horizontal, or mixed-direction movement, which is essential for complex industrial layouts. Finally, these systems are relatively easy to install and maintain, with minimal downtime required for routine maintenance or system upgrades.
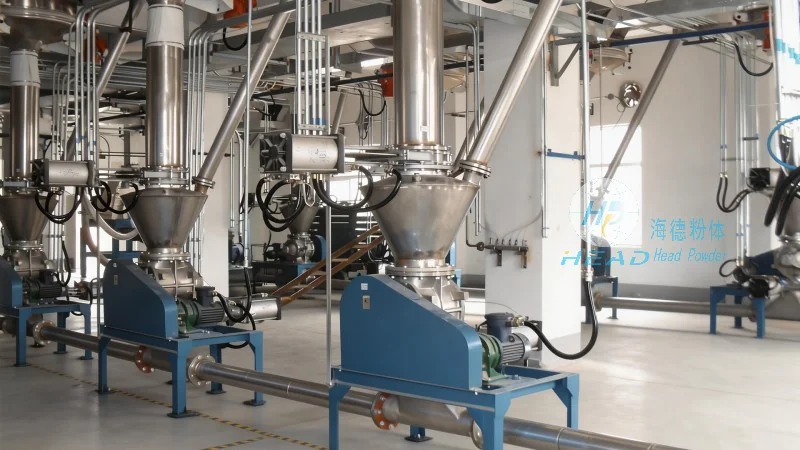
HeadPowder's expertise in designing and implementing pneumatic conveying systems for magnesium sulfate delivery highlights the importance of tailored solutions in industrial material handling. By understanding the specific characteristics of magnesium sulfate and the operational requirements of each application, companies can select the most appropriate pneumatic conveying system to ensure efficient, safe, and cost-effective material transport. As a trusted partner in the material handling industry, HeadPowder continues to innovate and provide solutions that meet the evolving needs of its clients, ensuring reliable and sustainable magnesium sulfate delivery across various industrial sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top