Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of industrial equipment, specializes in the design and manufacturing of advanced pneumatic conveying systems. With a strong commitment to innovation and precision engineering, the company has established itself as a trusted partner for clients seeking efficient and reliable solutions for ash handling and material transportation. HeadPowder's expertise lies in developing customized systems that meet the unique demands of various industrial applications, ensuring optimal performance and durability.
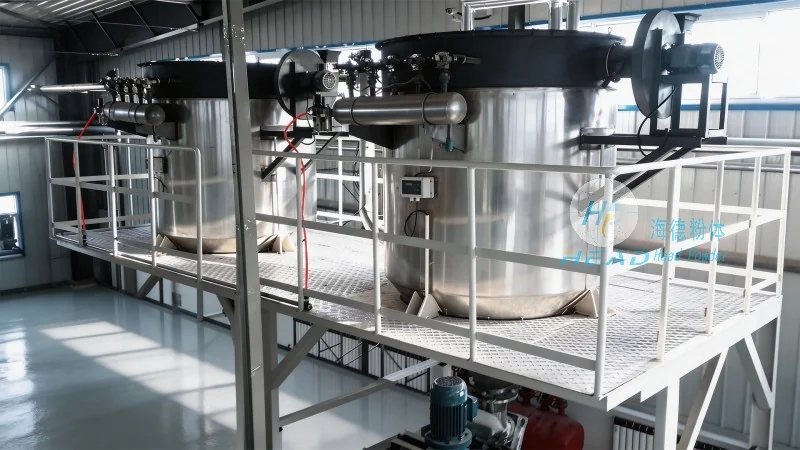
At the core of HeadPowder's product line is the purified ash pneumatic conveying device, engineered to handle the challenges associated with ash transportation in power plants and other industrial facilities. This system is designed to efficiently convey ash from storage silos or hoppers to disposal or processing units, while maintaining a high level of air quality and operational safety. The device incorporates advanced filtration and purification technologies to minimize dust emissions and ensure compliance with environmental regulations. By integrating state-of-the-art components and robust construction, the system delivers consistent performance under varying operational conditions.
The purified ash pneumatic conveying device from Shandong HeadPowder Engineering Co., Ltd. is equipped with several key technical features that enhance its functionality and efficiency. One of the primary advantages is its ability to handle abrasive and high-density ash materials without causing excessive wear on components. The system utilizes high-pressure air or gas to create a consistent flow, reducing the risk of blockages and ensuring smooth material transfer. Additionally, the device incorporates intelligent control systems that monitor pressure, flow rate, and temperature in real-time, allowing for automated adjustments and preventive maintenance. This proactive approach minimizes downtime and extends the service life of the equipment. The design also emphasizes energy efficiency, with optimized air consumption and reduced power requirements compared to traditional conveying methods. Furthermore, the system is constructed with corrosion-resistant materials, ensuring long-term durability in harsh industrial environments.
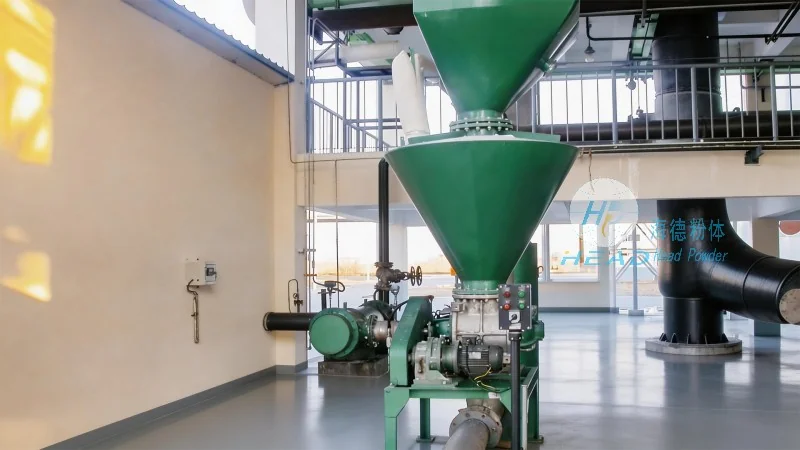
The purified ash pneumatic conveying device is widely applicable in power generation, cement production, and waste management industries, where the safe and efficient handling of ash is critical. In power plants, the system facilitates the transfer of fly ash from boiler ash hoppers to storage silos or disposal sites, improving operational efficiency and reducing manual handling risks. In cement plants, the device aids in the transportation of raw materials and byproducts, contributing to streamlined production processes. The system's ability to handle large volumes of ash at high speeds makes it ideal for facilities with high throughput requirements. Operational benefits include reduced labor costs, minimized environmental impact through effective dust control, and enhanced safety by eliminating the need for manual ash handling. The device also supports scalability, allowing for easy integration with existing infrastructure or expansion as production needs grow.
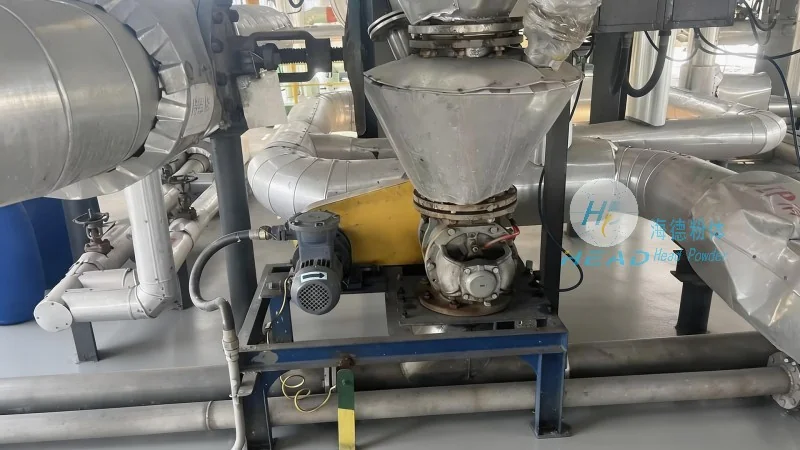
Shandong HeadPowder Engineering Co., Ltd. adheres to stringent quality standards in the development and production of its pneumatic conveying systems. Each component of the purified ash pneumatic conveying device undergoes rigorous testing and inspection to ensure compliance with industry specifications and safety requirements. The company employs advanced manufacturing techniques and quality control measures to minimize defects and ensure consistent performance. The system is designed with redundancy and fail-safe mechanisms to prevent operational failures and maintain continuous operation. Regular maintenance and service programs are also available to support clients in keeping their equipment in optimal condition. By prioritizing quality and reliability, HeadPowder ensures that its clients receive durable and dependable solutions that meet their long-term operational needs.
Shandong HeadPowder Engineering Co., Ltd. continues to innovate in the field of industrial pneumatic conveying, with the purified ash pneumatic conveying device representing a significant advancement in ash handling technology. The company's dedication to customer satisfaction, technical excellence, and environmental responsibility positions it as a leading provider of customized solutions for industrial material transportation. By leveraging its expertise and commitment to quality, HeadPowder aims to deliver systems that not only meet but exceed the expectations of its clients, contributing to the efficiency and sustainability of industrial operations worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top