Glucose, a vital carbohydrate widely used in pharmaceuticals, food processing, and chemical industries, requires efficient and reliable material handling solutions for its transportation. Pneumatic conveying systems have emerged as a preferred method for transporting granular and powdered materials like glucose due to their ability to handle delicate products while ensuring minimal contamination and loss. This technical analysis delves into the two primary pneumatic conveying modes—positive pressure and negative pressure—and compares their operational principles, advantages, disadvantages, and suitability for glucose transport applications.
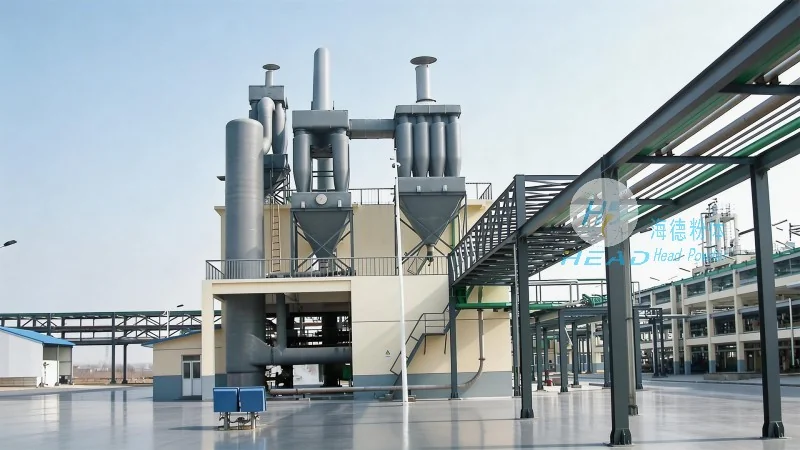
Glucose, often in the form of powdered or granular solids, is a critical raw material in various industries. Traditional methods like bucket elevators or belt conveyors may not be suitable for handling such materials due to their susceptibility to dust, caking, or product degradation. Pneumatic conveying systems offer a solution by using air or gas to transport materials through a pipeline, eliminating the need for mechanical contact and reducing the risk of contamination. The choice between positive pressure and negative pressure systems depends on factors such as material characteristics, system layout, and operational requirements.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer specializing in the design, development, and supply of pneumatic conveying systems. With a focus on precision engineering and customer-centric solutions, HeadPowder has established itself as a trusted partner for industries dealing with sensitive materials like glucose. The company’s headquarters is located in Shandong, China, and it leverages advanced technology and industry expertise to deliver high-performance conveying solutions tailored to specific application needs.
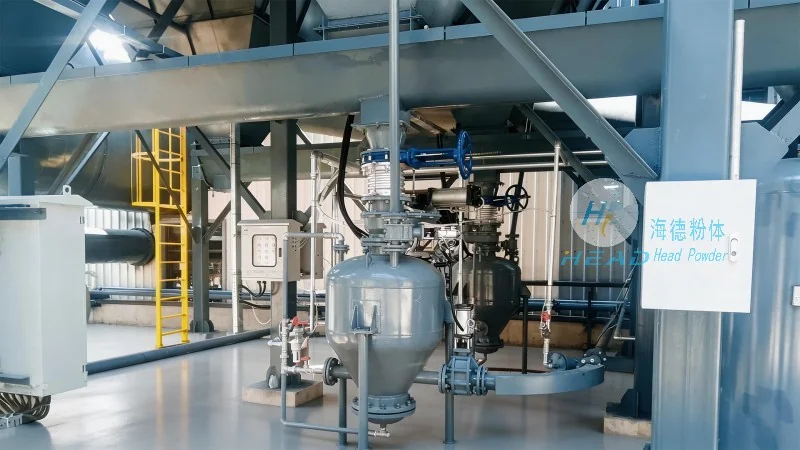
Positive pressure systems operate by blowing air or gas into the conveying line, creating a pressure higher than the ambient air pressure. This pressurized air propels the material forward through the pipeline. In the context of glucose transport, positive pressure systems are commonly used for short to medium-distance conveying, where the material is transported from a storage silo or hopper to a processing unit. The system typically consists of a blower, a hopper with a feeder, and a pipeline network. The air is introduced at the inlet of the hopper, and the material is drawn into the pipeline by the moving air stream. This mode is particularly effective for handling free-flowing materials like glucose, as the pressurized air maintains consistent flow and prevents material settling in the pipeline.
Key advantages of positive pressure systems include high conveying capacity, the ability to handle abrasive materials without significant wear on components, and the flexibility to transport materials over varying distances. The pressurized environment also helps in maintaining product integrity by reducing exposure to external contaminants. However, these systems require robust blower units and may generate higher noise levels compared to negative pressure systems. Additionally, the high air pressure can lead to increased energy consumption, making them less suitable for long-distance or large-scale applications where energy efficiency is a priority.
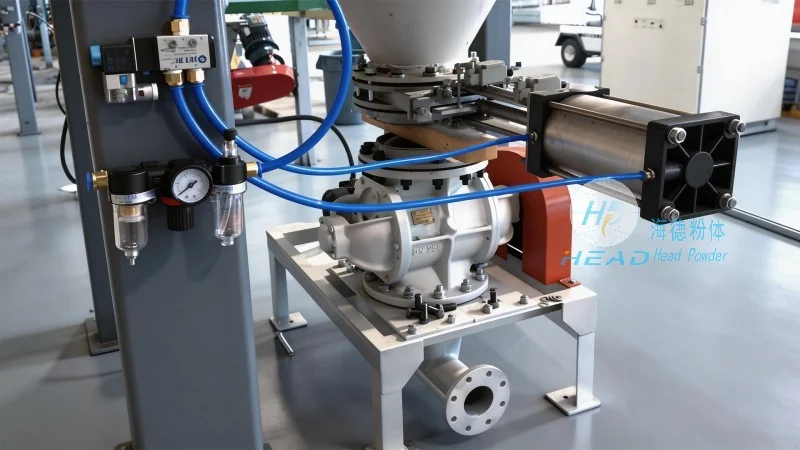
Negative pressure systems, also known as suction systems, operate by creating a vacuum or negative pressure within the conveying line. The material is drawn into the pipeline by the suction force, and the air carrying the material is then filtered and released into the atmosphere. For glucose transport, negative pressure systems are often employed for long-distance conveying, where the material needs to be transported from a remote storage location to a processing facility. The system typically includes a vacuum pump, a collection hopper, and a pipeline network. The material is introduced into the hopper, and the vacuum pump creates a negative pressure that pulls the material and air mixture into the pipeline.
One of the primary advantages of negative pressure systems is their energy efficiency, especially for long-distance conveying. The vacuum pump operates at lower pressures compared to the high-pressure blowers used in positive pressure systems, resulting in reduced energy consumption. This makes negative pressure systems more cost-effective for large-scale operations. Additionally, the suction mode allows for the collection of material from multiple points and transport to a central processing unit, enhancing operational flexibility. However, negative pressure systems are more susceptible to material degradation due to prolonged exposure to air and potential dust emissions during the conveying process. They also require careful maintenance of the filtration system to prevent dust from escaping into the environment.
When selecting between positive and negative pressure pneumatic conveying systems for glucose transport, several factors must be considered. The choice is often influenced by the distance of the conveying line, the material's flow characteristics, and the overall system cost. Positive pressure systems are generally preferred for short to medium distances (typically up to 100 meters) and for handling free-flowing, non-abrasive materials like glucose. They offer high conveying rates and better product protection due to the pressurized environment. In contrast, negative pressure systems are more suitable for long-distance conveying (up to several hundred meters) and for applications where energy efficiency is a critical factor. They are also advantageous when the material needs to be collected from multiple sources and transported to a central location.
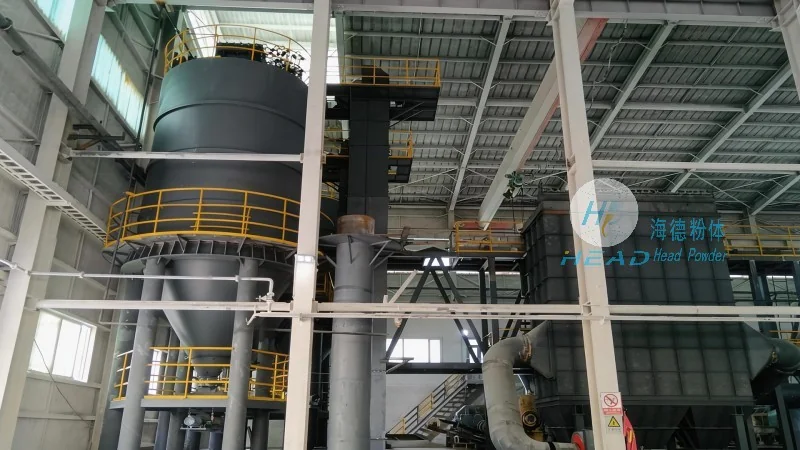
From an operational perspective, positive pressure systems are simpler to install and maintain, as they do not require extensive filtration systems to handle dust emissions. The pressurized air also helps in preventing material caking and blockages in the pipeline. Negative pressure systems, while energy-efficient, demand more sophisticated filtration and dust control measures to comply with environmental regulations. The choice between the two modes also depends on the specific application requirements, such as the need for product containment or the presence of abrasive particles in the material.
Both positive pressure and negative pressure pneumatic conveying systems offer viable solutions for transporting glucose, with each mode having its own set of advantages and limitations. Positive pressure systems excel in short-distance, high-capacity applications, providing reliable and efficient material handling with minimal product degradation. Negative pressure systems, on the other hand, are ideal for long-distance conveying and energy-efficient operations, though they require more careful management of dust and filtration. For industries dealing with glucose and other sensitive materials, the choice of system should be based on a thorough evaluation of operational needs, material characteristics, and cost considerations. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing customized pneumatic conveying solutions that cater to these diverse requirements, ensuring optimal performance and product integrity in glucose transport applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top