Lysine is a crucial amino acid widely used in animal feed and agricultural applications. The method of transporting lysine from production sites to processing facilities or storage areas directly impacts operational efficiency, material integrity, and overall production costs. Among the various transport technologies available, positive pressure and negative pressure systems are two primary options. Understanding the differences between these two approaches is essential for selecting the most suitable solution for lysine transport. This article provides a detailed comparison of positive pressure and negative pressure transport systems, outlining key factors to consider when making a decision.
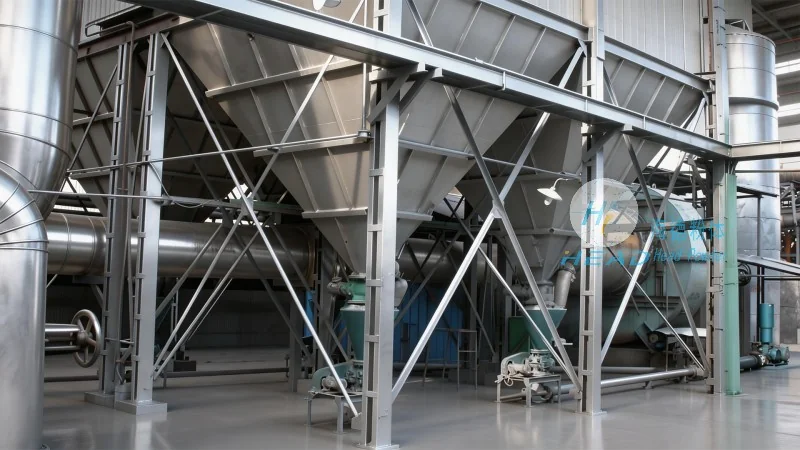
Positive pressure transport, also known as pressure blow or pneumatic conveying, operates by forcing air or gas through a pipeline at a pressure higher than the ambient air pressure. The pressurized air creates a flow that carries the lysine particles along the pipeline. This method is particularly effective for transporting lysine over long distances, through complex networked systems, or when dealing with materials that are prone to clogging or have varying particle sizes.
One of the main advantages of positive pressure systems is their ability to handle a wide range of material characteristics. They can transport dry, free-flowing lysine efficiently, even when the material is dusty or has a tendency to agglomerate. Additionally, positive pressure systems are less susceptible to external atmospheric pressure changes, ensuring consistent flow rates and preventing material backflow. However, they typically require higher energy input due to the need to maintain elevated pressure levels, which can increase operational costs over time.
Negative pressure transport, or vacuum conveying, works by creating a vacuum in the pipeline, drawing lysine particles into the system. The vacuum is generated by a fan or pump that pulls air (and the lysine particles) through the pipeline. This method is commonly used for shorter transport distances, typically up to a few hundred meters, and is ideal for materials that are light, have good flowability, and are less prone to clogging.
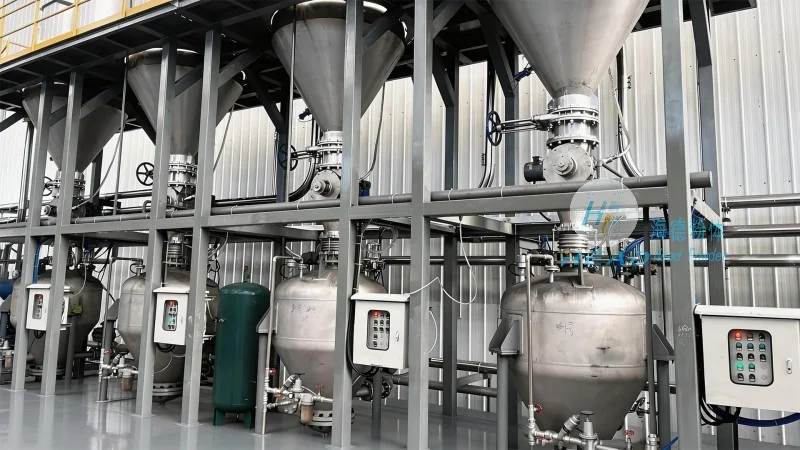
One of the key benefits of negative pressure systems is their lower energy consumption compared to positive pressure systems. The vacuum generation process requires less power, making them more cost-effective for shorter transport needs. Furthermore, negative pressure conveying tends to cause less wear and tear on the lysine particles, preserving their quality and reducing the risk of degradation. However, the effective distance is limited, and the system may be more sensitive to changes in ambient air pressure, which can affect performance if the transport distance is extended.
When deciding between positive and negative pressure transport for lysine, several factors must be carefully evaluated. The most critical consideration is the distance over which the lysine needs to be transported. Positive pressure systems are generally preferred for long-distance applications, while negative pressure is suitable for short distances. The physical properties of the lysine, such as particle size, moisture content, and flowability, also play a significant role. Materials with larger particles or higher moisture content may require positive pressure to ensure proper flow and prevent blockages. Conversely, fine, dry lysine with excellent flow characteristics can often be handled by negative pressure systems.
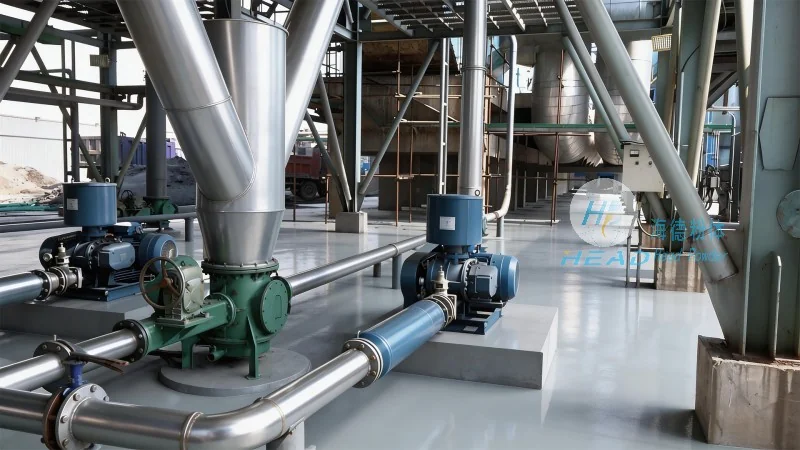
System complexity and maintenance requirements are additional factors to consider. Positive pressure systems may involve more complex piping and pressure control mechanisms, which can increase installation and maintenance costs. Negative pressure systems, while simpler in design, may require more frequent filter changes to prevent dust accumulation and maintain vacuum efficiency. The overall budget and operational costs are also important. Positive pressure systems may have higher upfront and ongoing energy costs, whereas negative pressure systems offer lower energy consumption but may have higher initial investment for the vacuum generation equipment.
For businesses seeking reliable and efficient lysine transport solutions, Shandong HeadPowder Engineering Co., Ltd. offers comprehensive engineering and equipment solutions tailored to specific operational needs. With years of experience in the chemical and agricultural sectors, the company specializes in designing and manufacturing transport systems that optimize material handling while minimizing downtime and operational expenses. Based in Shandong, China, HeadPowder leverages advanced technology and industry best practices to deliver customized solutions that meet the unique requirements of lysine producers and processors.
The company’s team of engineers and technicians works closely with clients to assess their transport challenges, recommend the most appropriate system (positive or negative pressure), and provide installation and maintenance support. By focusing on material integrity and system efficiency, HeadPowder ensures that lysine is transported safely and effectively, preserving its quality from the production stage to the final application. Whether a client requires a new transport system or upgrades to an existing one, HeadPowder’s expertise and commitment to quality make it a trusted partner in the lysine transport industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top