Phenolic resin, a versatile and widely used industrial material, often requires efficient and reliable transportation methods for processing and application. Pneumatic conveying systems offer a robust solution for handling phenolic resin, ensuring consistent flow, minimal material degradation, and enhanced safety in industrial operations. This article outlines key design considerations for such systems, focusing on the technical and operational aspects that contribute to optimal performance.
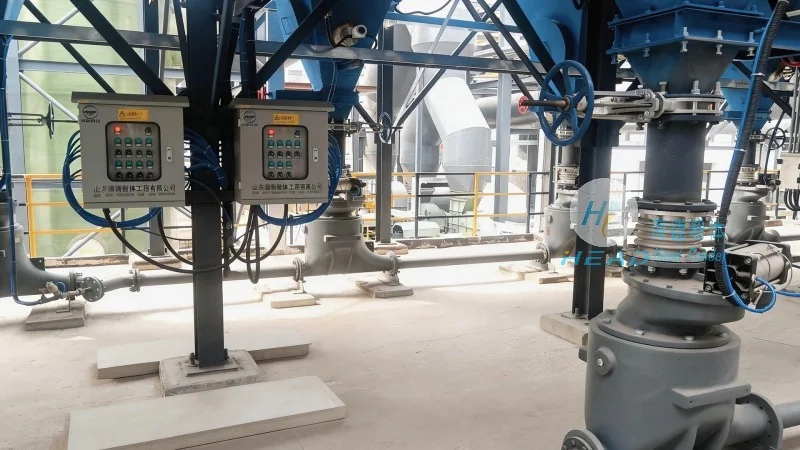
Before designing a pneumatic conveying system for phenolic resin, it is crucial to understand the material's physical and chemical characteristics. Phenolic resins are typically solid particles with varying sizes, densities, and flow properties. Their handling requirements may include considerations for moisture content, temperature sensitivity, and potential dust generation. These factors directly impact the selection of system components, such as hoppers, feeders, and conveying lines, to ensure efficient and safe material transport. For instance, the choice of hopper design may need to accommodate the resin's bulk density and flowability, preventing bridging or clogging that could disrupt the conveying process.
The core components of a phenolic resin pneumatic conveying system include the hopper, material feeder, conveying line, and receiver. Each component plays a critical role in the overall system performance. The hopper, often equipped with a discharge gate or rotary valve, stores the phenolic resin and controls the material flow into the system. The feeder, such as a rotary or vibratory type, ensures a consistent and controlled feed rate, preventing surges or drops that could affect the conveying efficiency. The conveying line, typically made of stainless steel or other corrosion-resistant materials, transports the resin particles through compressed air or other gas streams. The receiver, positioned at the end of the line, collects the conveyed material and may include a dust collection system to manage any airborne particles. The selection of these components must align with the resin's properties and the desired conveying capacity, ensuring long-term reliability and minimal maintenance.
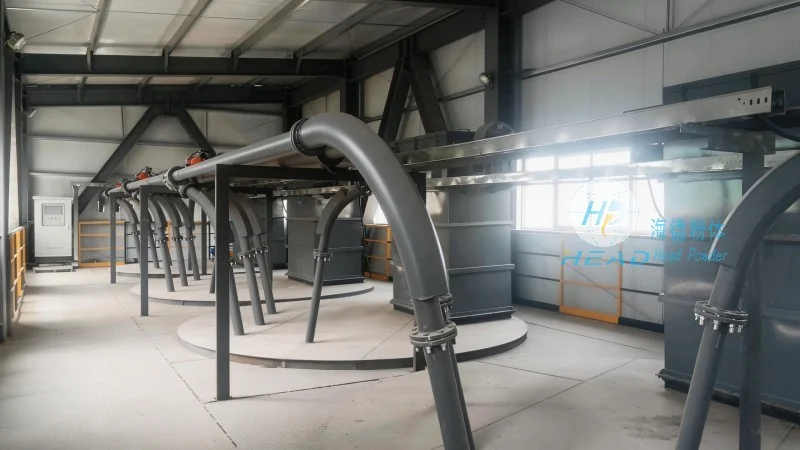
Proper material flow and pressure management are essential for the effective operation of phenolic resin pneumatic conveying systems. The system operates under positive or negative pressure, depending on the application. Positive pressure systems use compressed air to push the resin through the line, while negative pressure systems use vacuum to draw the material. The pressure levels must be optimized to maintain consistent flow rates and prevent material degradation. For phenolic resin, which can be sensitive to high temperatures or pressure fluctuations, the system design must include temperature control and pressure regulation mechanisms. This may involve the use of heat exchangers or pressure relief valves to protect the resin and system components from damage. Additionally, the design should account for the resin's particle size distribution, as larger particles may require higher air velocities to maintain suspension and prevent blockages in the conveying line.
Integrating the pneumatic conveying system with other industrial processes is a critical aspect of its design. The system must be compatible with existing equipment, such as mixing or processing units, to ensure seamless material transfer. Control systems, including sensors and programmable logic controllers (PLCs), are essential for monitoring and regulating the conveying process. These systems can track flow rates, pressure levels, and material levels, providing real-time data for process optimization. For phenolic resin applications, the control system may need to include features for moisture control or temperature monitoring to maintain the resin's quality. The integration of these controls ensures that the system operates efficiently and safely, minimizing downtime and maximizing productivity.
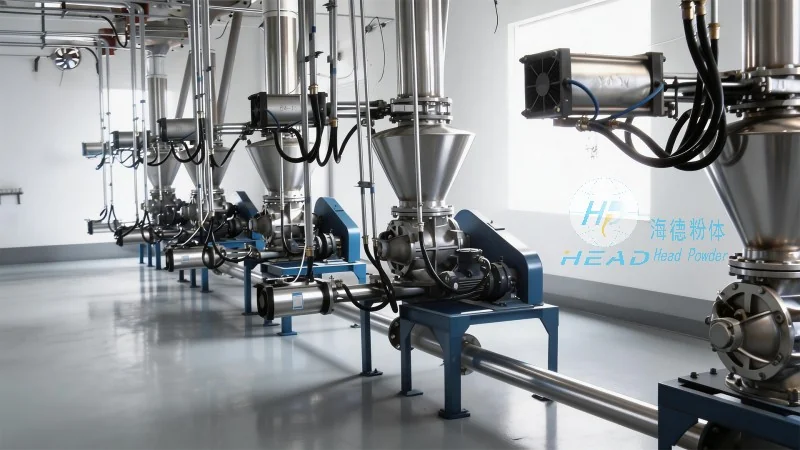
Regular maintenance is vital for the longevity and performance of phenolic resin pneumatic conveying systems. The system components, especially the conveying line and hoppers, may accumulate resin residue or dust over time, which can affect flow and efficiency. Routine cleaning and inspection of these parts are necessary to prevent clogging and ensure consistent operation. Additionally, the system should be equipped with monitoring tools to detect any issues early, such as pressure drops or abnormal flow rates, allowing for timely maintenance. For phenolic resin, which may be abrasive or corrosive, the use of high-quality materials and protective coatings is recommended to extend the system's lifespan. The maintenance schedule should be tailored to the resin's handling frequency and the system's operational load, ensuring that it remains in optimal condition throughout its service life.
Designing a phenolic resin pneumatic conveying system requires a comprehensive understanding of the material's properties, system components, and operational requirements. By addressing key considerations such as material flow, pressure management, and system integration, manufacturers can ensure efficient and reliable transportation of phenolic resin. The use of robust components, proper control systems, and regular maintenance further enhances the system's performance and longevity. For industries relying on phenolic resin, investing in a well-designed pneumatic conveying system is essential for optimizing production processes and maintaining product quality. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in the design and implementation of such systems, leveraging expertise to deliver tailored solutions that meet the specific needs of clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top