HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for industrial applications. This article focuses on the design of a borax granule pneumatic conveying system, highlighting key considerations, technical specifications, and practical applications that ensure efficient and reliable material handling in borax processing facilities.
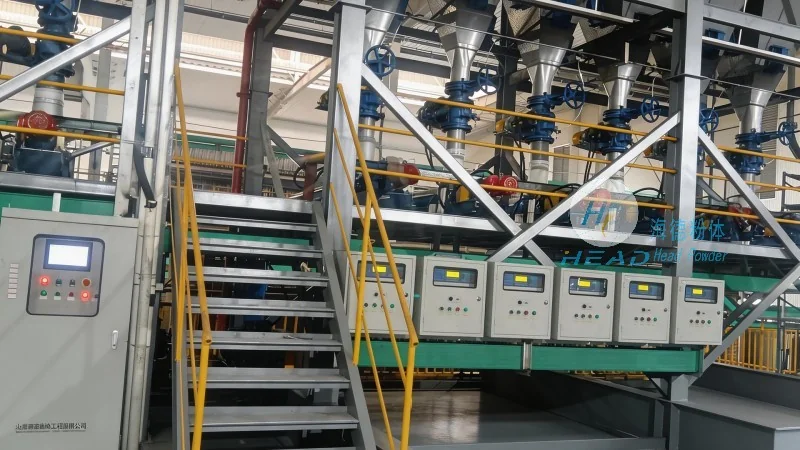
The borax granule pneumatic conveying system is engineered to transport borax granules from storage silos to processing units or packaging areas. The system integrates several critical components, including a feed hopper, rotary airlock valve, positive displacement blower or pressure vessel, and a conveying pipeline network. Each component is selected to meet the specific flow rates, particle characteristics, and operational requirements of borax granules, ensuring optimal performance and minimal material degradation.
When designing a pneumatic conveying system for borax granules, several factors must be carefully evaluated. First, the particle size and density of borax granules influence the choice of conveying method—whether it is a dilute phase or dense phase system. Borax granules typically have a particle size range of 0.5 to 2.0 mm and a bulk density of approximately 800 to 1000 kg/m³, which affects the air velocity and pressure requirements. Additionally, the system must account for the hygroscopic nature of borax, as moisture absorption can impact material flow and equipment performance. To mitigate this, the design incorporates moisture-resistant materials and proper sealing mechanisms to prevent material caking or blockages.
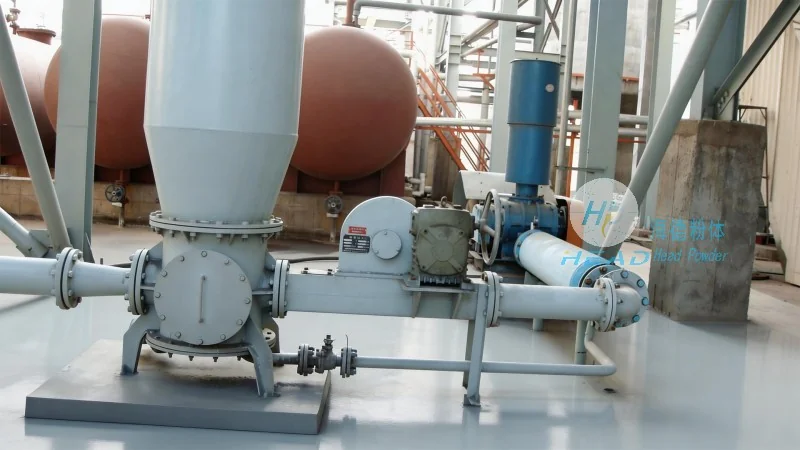
The borax granule pneumatic conveying system is designed to achieve a conveying capacity of up to 50 tons per hour, with a maximum conveying distance of 200 meters. The system utilizes a positive displacement blower capable of generating a pressure of 0.6 MPa, ensuring sufficient air flow to maintain consistent material transport. The conveying pipeline is constructed from corrosion-resistant stainless steel to withstand the chemical properties of borax and prevent degradation over time. Performance metrics such as conveying efficiency, energy consumption, and material loss are monitored through integrated sensors and control systems, allowing for real-time adjustments to optimize operation.
Borax granule pneumatic conveying systems are widely used in the chemical, pharmaceutical, and food industries, where precise material handling is critical. In the context of borax processing, the system integrates seamlessly with existing storage and processing infrastructure, reducing downtime and improving overall production throughput. The system’s modular design allows for easy expansion or modification to accommodate changes in production volume or product specifications. HeadPowder’s expertise in customizing pneumatic conveying solutions ensures that clients receive a system tailored to their specific operational needs, enhancing productivity and reducing operational costs.
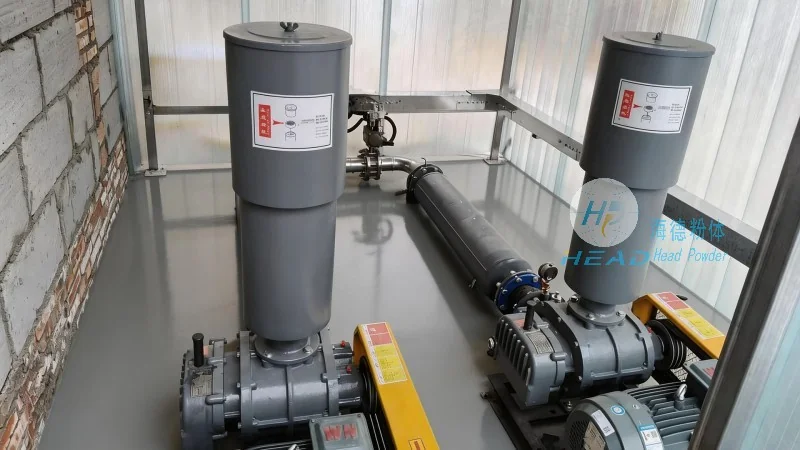
Proper maintenance is essential to ensure the long-term reliability of the borax granule pneumatic conveying system. Regular inspections of components such as the feed hopper, rotary airlock valve, and pipeline for wear or damage are recommended. Cleaning procedures, including the use of compressed air or mechanical cleaning tools, should be performed to remove accumulated material and prevent blockages. Operational best practices include monitoring air pressure and flow rates, adjusting system parameters based on material conditions, and conducting periodic performance tests to verify system efficiency. By adhering to these guidelines, operators can maximize the lifespan of the system and minimize downtime, ensuring consistent and reliable material transport.
The design of a borax granule pneumatic conveying system by HeadPowder exemplifies the integration of advanced engineering principles and practical industrial solutions. By addressing key design considerations, technical specifications, and operational best practices, the system ensures efficient, safe, and cost-effective transport of borax granules. HeadPowder’s commitment to quality and customization makes it a trusted partner for industries requiring reliable material handling solutions, particularly in the borax processing sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top