When it comes to the efficient and reliable transport of solid powders, pneumatic conveying systems have emerged as a critical solution across various industries. These systems utilize air or other gases to move bulk materials from one location to another, offering advantages such as reduced contamination, improved safety, and the ability to handle a wide range of powder characteristics. However, the success of a pneumatic conveying system hinges on meticulous design and careful consideration of several key factors. This article explores the essential design considerations for solid powder pneumatic conveying systems, providing insights into how to optimize performance and ensure long-term operational efficiency.
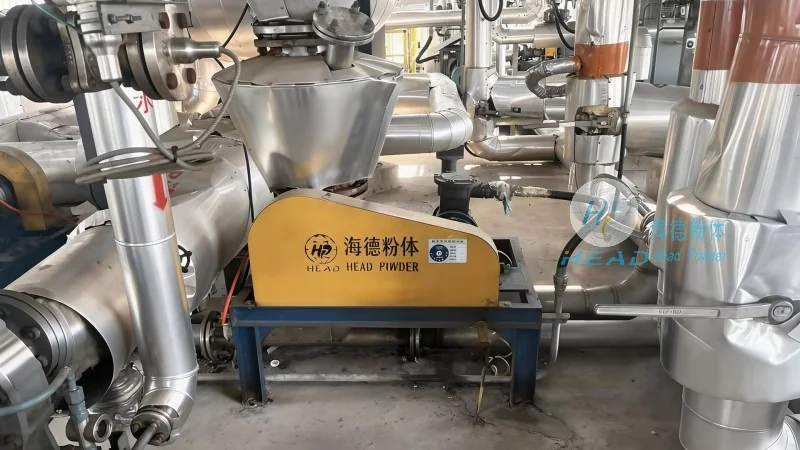
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, development, and implementation of advanced pneumatic conveying solutions. With a deep understanding of the unique challenges associated with solid powder handling, HeadPowder leverages years of industry experience to deliver tailored system solutions that meet the specific needs of clients across diverse sectors. The company's commitment to quality, innovation, and customer satisfaction has established it as a trusted partner in the field of material handling technology.
The design of a solid powder pneumatic conveying system involves a comprehensive evaluation of several critical parameters to ensure optimal performance and durability. The first step in the design process is to determine the appropriate conveying method, which can be broadly categorized into pressure and vacuum systems. Pressure systems, where air is introduced under pressure at the inlet, are commonly used for long-distance or high-capacity applications, while vacuum systems, which draw material into a low-pressure environment, are often preferred for shorter distances or when material needs to be transferred from multiple sources.
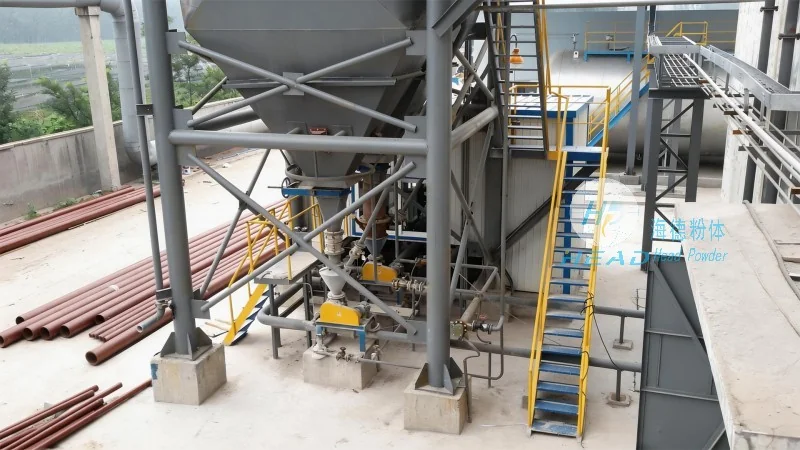
Another crucial aspect is the selection of the conveying line configuration. The choice between dilute-phase and dense-phase systems depends on the material's properties, such as particle size, density, and flowability. Dilute-phase systems, which operate at higher velocities, are suitable for free-flowing powders and require less energy but may generate more dust. Dense-phase systems, which operate at lower velocities and higher pressure, are ideal for cohesive or abrasive materials, offering better control over material flow and reduced wear on equipment.
Pipeline design is another critical factor that directly impacts system performance. The diameter and length of the conveying line must be carefully calculated to maintain the required air velocity and pressure drop. Properly sized elbows, bends, and other fittings are essential to minimize pressure losses and prevent material buildup or blockages. Additionally, the material of construction for the pipeline—such as stainless steel, plastic, or metal—must be selected based on the chemical compatibility of the powder and the operating conditions, ensuring resistance to corrosion and wear.
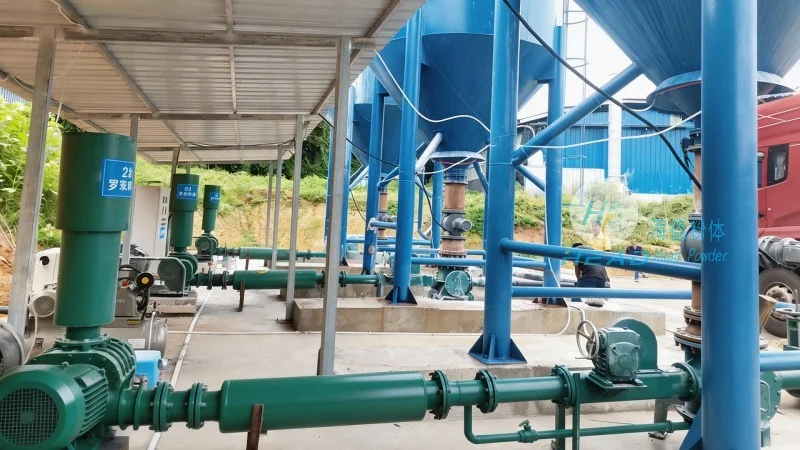
Equipment selection is a key component of the design process. The type of feeder, such as a rotary valve or a star feeder, plays a vital role in controlling the flow rate and preventing material degradation. The choice of the air compressor or vacuum pump must be matched to the system's pressure and flow requirements, ensuring sufficient power to maintain the desired conveying conditions. The use of filters and cyclones is also essential to separate the conveyed material from the air stream, allowing for recycling of the air and collection of the powder for reuse or disposal.
System integration and control are critical for ensuring smooth operation and maintaining optimal performance. A well-designed control system allows for real-time monitoring of pressure, flow, and temperature, enabling operators to adjust parameters as needed to prevent system failures or inefficiencies. Additionally, incorporating safety features, such as pressure relief valves and emergency shut-off mechanisms, is essential to protect both personnel and equipment from potential hazards.
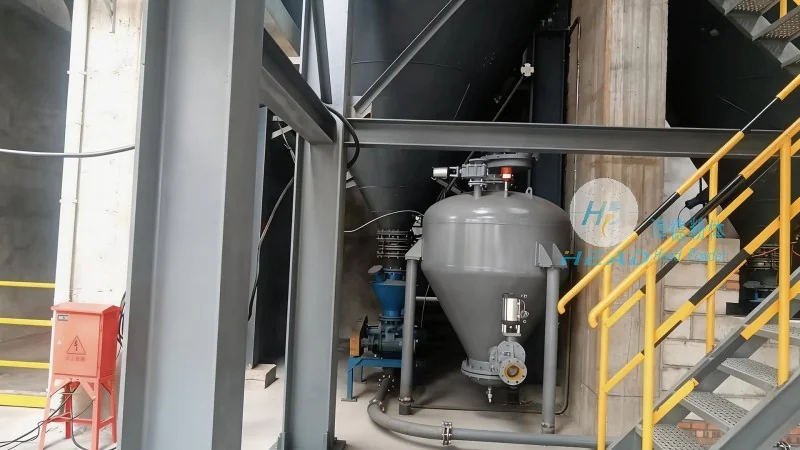
Solid powder pneumatic conveying systems are widely used across various industries due to their versatility and efficiency. In the chemical industry, these systems are used to transport raw materials, intermediates, and finished products, such as powders, granules, and pellets. The ability to handle abrasive and corrosive materials makes them ideal for applications involving chemicals, pharmaceuticals, and food products. In the pharmaceutical sector, the use of stainless steel and other sanitary materials ensures compliance with regulatory standards, making these systems suitable for handling active pharmaceutical ingredients (APIs) and other sensitive materials. The food industry also benefits from pneumatic conveying systems, which can be designed to meet strict hygiene requirements, ensuring the safe and efficient transport of food powders like flour, sugar, and spices.
In the cement and construction industry, pneumatic conveying is used to transport raw materials, such as limestone and clay, from storage silos to processing facilities. The high capacity and reliability of these systems make them well-suited for large-scale operations, where consistent material flow is essential. The mining industry also utilizes pneumatic conveying systems to transport ore and other minerals from mining sites to processing plants, reducing the need for manual handling and improving operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top