Pharmaceutical powder pneumatic conveying systems are critical infrastructure in the manufacturing and distribution of medicinal products. These systems are designed to safely and efficiently transport powders, ensuring compliance with stringent regulatory standards while maintaining product integrity. The design of such systems involves careful consideration of multiple factors, from material properties to operational requirements. This article outlines key design considerations for pharmaceutical powder pneumatic conveying systems, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
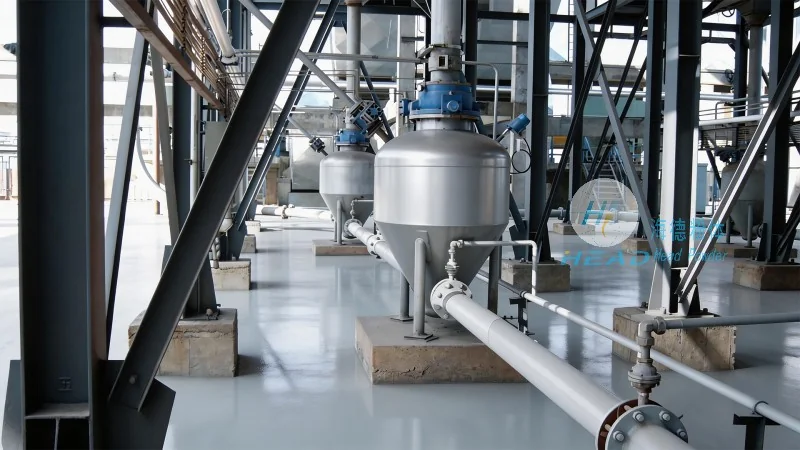
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a specialized engineering firm based in Shandong, China. With a strong focus on the pharmaceutical industry, the company has developed extensive expertise in designing and implementing advanced powder handling solutions. headpowder's team of engineers and technicians brings years of experience in adhering to GMP (Good Manufacturing Practice) and other regulatory requirements, ensuring that every system they design meets the highest standards of safety and efficiency.
The design of a pharmaceutical powder pneumatic conveying system must prioritize several key principles to ensure optimal performance and compliance. First, the system must be constructed from materials that are non-reactive and easy to clean, typically stainless steel or other inert materials, to prevent contamination of the product. This is crucial in pharmaceutical applications where product purity is paramount. Second, the system must be designed to minimize particle degradation and agglomeration during transport. This involves selecting appropriate air velocities and pipeline diameters to maintain the powder's physical properties while preventing clogging or blockages.
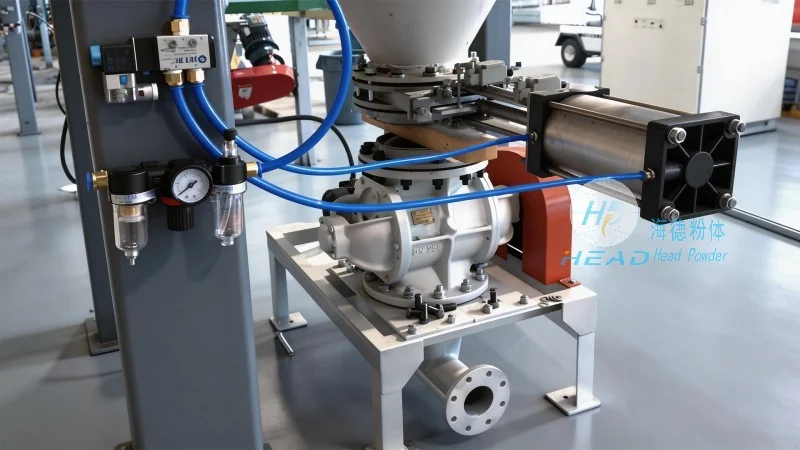
A pharmaceutical powder pneumatic conveying system typically consists of several key components, each playing a vital role in the overall operation. The primary components include the hopper or feeder, which stores and meters the powder; the conveying line, which transports the powder using air pressure; and the receiver or discharge unit, which collects the powder at the destination. The hopper design is critical, as it must prevent material bridging and ensure consistent feeding. The conveying line must be sized appropriately to handle the specific powder characteristics, such as particle size, density, and flowability. The receiver must be equipped with proper filtration and dust collection systems to maintain air quality and prevent environmental contamination.
Contamination control is a top priority in pharmaceutical powder handling. The design of the pneumatic conveying system must incorporate features that prevent cross-contamination between different product batches. This includes using closed systems with minimal dead spaces, as well as implementing proper cleaning and sanitization procedures. The system should also be designed to handle powders with varying properties, such as hygroscopic or abrasive materials, without causing wear or degradation. headpowder specializes in customizing systems to meet these specific material handling challenges, ensuring that each component is optimized for the unique characteristics of the pharmaceutical powder being transported.
Pharmaceutical manufacturing is heavily regulated, and the pneumatic conveying system must comply with all relevant standards and regulations. This includes adherence to GMP guidelines, which dictate the design, construction, and operation of equipment to ensure product quality and safety. The system must be designed with safety features such as pressure relief valves, emergency shut-off mechanisms, and proper ventilation to prevent accidents and ensure operator safety. Additionally, the system should be equipped with monitoring and control systems that allow for real-time tracking of parameters like pressure, flow rate, and temperature, enabling immediate intervention if any issues arise.
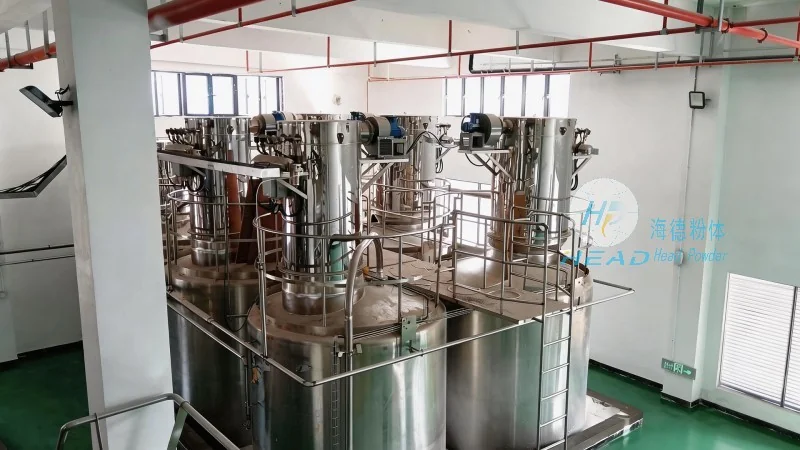
Every pharmaceutical facility has unique requirements, and a one-size-fits-all approach to pneumatic conveying is not feasible. headpowder offers customized solutions tailored to the specific needs of each client. This includes designing systems that can handle varying powder quantities, different product types, and specific operational conditions. The systems can be scaled from small laboratory-scale units to large industrial-scale installations, ensuring flexibility and adaptability. The company's engineers work closely with clients to understand their production processes and design a system that maximizes efficiency while minimizing downtime and maintenance costs.
Designing a pharmaceutical powder pneumatic conveying system requires a comprehensive approach that balances technical performance with regulatory compliance and safety. Shandong HeadPowder Engineering Co., Ltd. brings the necessary expertise and experience to deliver high-quality, customized solutions that meet the stringent demands of the pharmaceutical industry. By focusing on material properties, system components, contamination control, and regulatory adherence, headpowder ensures that each system is optimized for reliability, efficiency, and product integrity. For pharmaceutical manufacturers seeking reliable and compliant powder handling solutions, headpowder is a trusted partner in the design and implementation of advanced pneumatic conveying systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top