Ammonium bicarbonate is a widely used chemical in various industrial applications, and its efficient handling and transportation are crucial for maintaining production efficiency and product quality. Pneumatic conveying is a common method for transporting such bulk materials, offering advantages like reduced dust generation, improved safety, and flexibility in system design. This article explores several effective solutions for the pneumatic conveying of ammonium bicarbonate, highlighting key considerations and practical implementations.
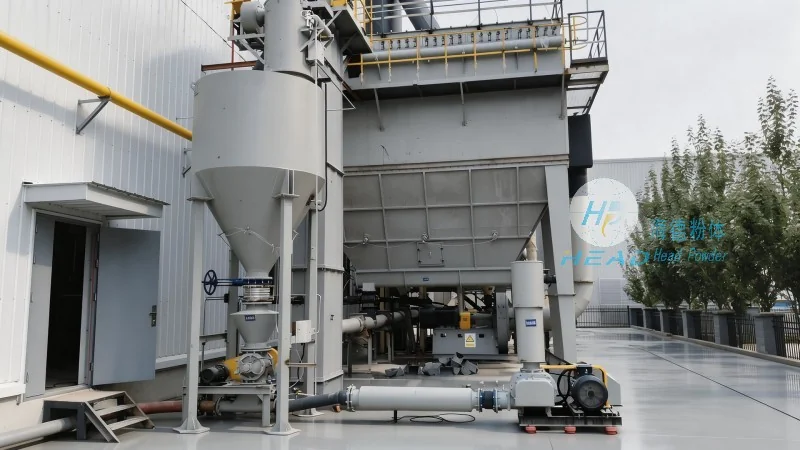
Pneumatic conveying systems are designed to transport bulk materials like ammonium bicarbonate through a pipeline using air or other gases. The primary goal is to move the material from a source (such as a storage silo or production line) to a destination (like a processing unit or packaging area) without the need for mechanical components like conveyor belts or buckets. These systems are particularly suitable for ammonium bicarbonate due to its hygroscopic nature and the need to minimize exposure to moisture and air, which can affect its stability and performance.
When designing a pneumatic conveying system for ammonium bicarbonate, several factors must be carefully evaluated to ensure optimal performance and longevity. First, the material's physical properties, such as particle size distribution, density, and flowability, play a critical role. Ammonium bicarbonate particles are typically fine and can be prone to agglomeration, which may affect the system's efficiency. Second, the system must be designed to prevent moisture absorption, as ammonium bicarbonate is hygroscopic and can degrade when exposed to humidity. This often requires the use of dry, filtered air and proper sealing of the system components. Third, the system's capacity and pressure requirements must be matched to the production needs, ensuring that the conveying velocity and pressure are sufficient to move the material without causing excessive wear or energy consumption.
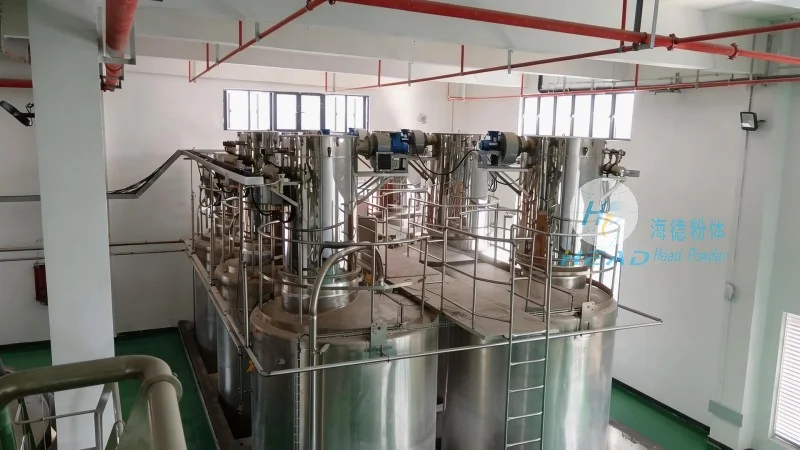
There are several pneumatic conveying solutions tailored to the specific needs of ammonium bicarbonate handling. One common approach is the positive pressure system, where air is supplied under pressure to push the material through the pipeline. This system is effective for short to medium distances and can handle a wide range of material flow rates. Another solution is the negative pressure (or vacuum) system, which uses a vacuum to draw the material into the pipeline. This method is often preferred for applications requiring gentle handling, as it minimizes particle breakage and is suitable for longer conveying distances. Additionally, a hybrid system combining both positive and negative pressure can be used for more complex layouts, allowing for efficient material transport over varying distances and elevations.
Effective pneumatic conveying of ammonium bicarbonate relies on several key components. The feeders are critical for controlling the material flow rate and ensuring consistent feeding into the system. For ammonium bicarbonate, which can be prone to bridging or caking, a rotary valve or a screw feeder with anti-clogging features is often used. The conveying line itself is typically made of materials resistant to the chemical properties of ammonium bicarbonate, such as stainless steel or special coatings, to prevent corrosion and material degradation. The air supply system includes compressors, filters, and dryers to provide clean, dry air at the required pressure and flow rate. Additionally, separators and cyclones are used to separate the material from the air stream at the receiving end, ensuring that the material is deposited accurately and the air is filtered before release.
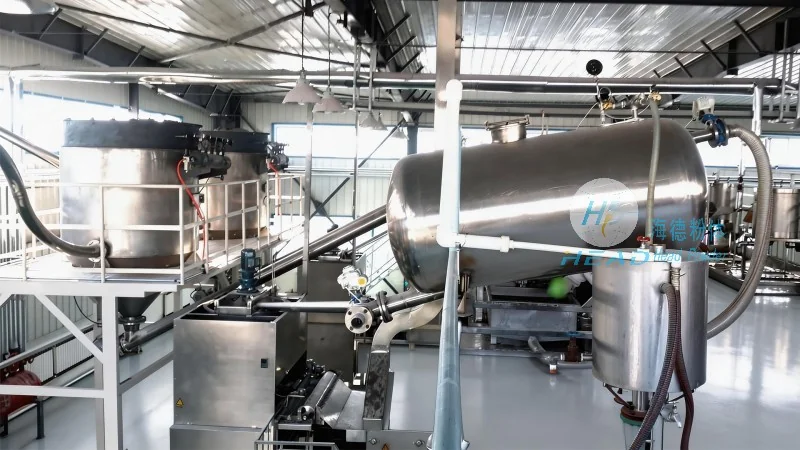
Pneumatic conveying offers several advantages for handling ammonium bicarbonate, including reduced dust exposure, improved safety, and the ability to transport materials in a closed system, minimizing environmental impact. However, there are also challenges to consider. For example, the hygroscopic nature of ammonium bicarbonate can lead to moisture absorption in the system, affecting the material's quality and potentially causing corrosion. Additionally, the fine particle size may lead to increased wear on system components, requiring regular maintenance and replacement of parts. Proper system design and maintenance are essential to mitigate these challenges and ensure long-term operational efficiency.
Choosing the right pneumatic conveying solution for ammonium bicarbonate is essential for optimizing production processes and maintaining product quality. By considering the material's physical properties, system requirements, and operational constraints, industries can select the most suitable conveying method. Regular maintenance and monitoring of the system components are also crucial to ensure consistent performance and extend the system's lifespan. As a leading provider of engineering solutions, Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in designing and implementing customized pneumatic conveying systems tailored to the specific needs of ammonium bicarbonate handling. With years of experience in the industry, the company offers expert guidance and high-quality equipment to help clients achieve efficient and reliable material transport.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top