HeadPowder, a leading provider in the field of material handling solutions, specializes in advanced pneumatic conveying systems tailored for the transportation of sodium dithionite. This article explores the benefits, technical aspects, and practical applications of pneumatic conveying for sodium dithionite, highlighting how this method addresses the challenges of traditional material transport while promoting efficiency and environmental sustainability.
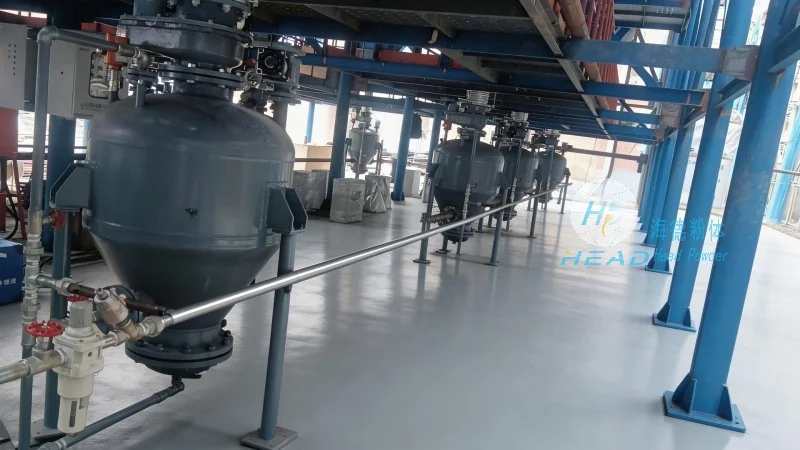
HeadPowder, operating as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. With a focus on innovative engineering solutions, the company has established itself as a trusted partner for industries requiring reliable and eco-friendly material handling systems. Our expertise lies in designing and implementing pneumatic conveying technologies that optimize the movement of bulk materials like sodium dithionite, ensuring safety, efficiency, and minimal environmental impact.
Sodium dithionite, also known as sodium hydrosulfite, is a critical chemical used in various industrial processes, including textile bleaching, food processing, and water treatment. Traditional methods of transporting this material often involve manual handling or mechanical systems that pose risks of dust exposure, contamination, and operational inefficiencies. Pneumatic conveying offers a superior alternative, leveraging compressed air to transport sodium dithionite in a closed system. This approach significantly reduces the risk of dust inhalation and environmental contamination, aligning with modern industrial safety and sustainability standards. The efficiency of pneumatic conveying is evident in its ability to handle large volumes of material with minimal downtime, enhancing overall production throughput. Additionally, the closed system design minimizes material loss and ensures consistent quality, which is crucial for applications where purity is paramount.
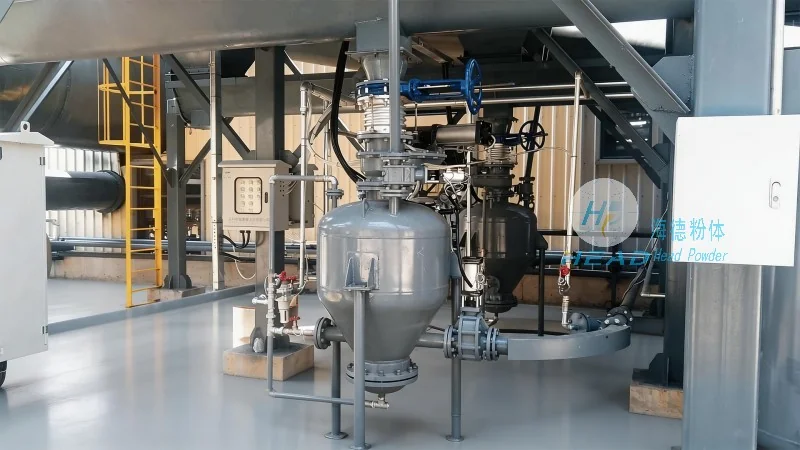
The effectiveness of pneumatic conveying for sodium dithionite depends on several key technical components. The system typically includes a hopper for material storage, a rotary valve or feeder to control the flow rate, a conveying line (often made of stainless steel to resist corrosion from the chemical), and a receiver for the material at the destination. The choice of conveying method—positive or negative pressure—depends on the distance, material characteristics, and operational requirements. Positive pressure systems use compressed air to push the material through the line, while negative pressure systems use vacuum to draw the material. For sodium dithionite, which is hygroscopic and can degrade if exposed to air, a positive pressure system is often preferred as it maintains a dry, inert environment. The system also incorporates filters and cyclones to separate the material from the air, ensuring that the conveyed material remains clean and free from contaminants. Proper maintenance of these components is essential to prevent blockages and ensure consistent performance.
Pneumatic conveying of sodium dithionite is widely adopted across multiple industries due to its versatility and efficiency. In the textile industry, it is used for bleaching processes where consistent material delivery is critical to maintain fabric quality. The food and beverage sector utilizes it in applications such as food processing and water treatment, where hygiene and purity are non-negotiable. Additionally, in the chemical manufacturing industry, pneumatic conveying ensures safe and efficient transport of sodium dithionite between production stages, reducing the risk of accidents and improving operational safety. The system's ability to handle varying material flow rates makes it suitable for both small-scale and large-scale operations, catering to the diverse needs of different industrial applications.
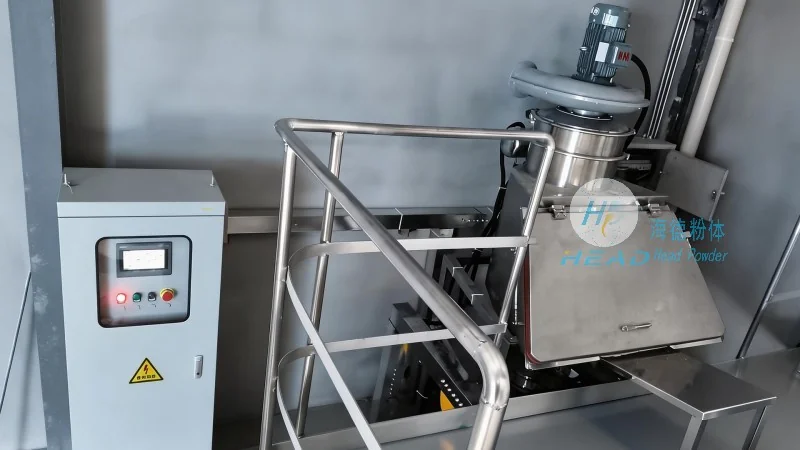
One of the most significant advantages of pneumatic conveying for sodium dithionite is its environmental impact. Unlike traditional methods that may involve open-air handling, which can lead to dust pollution and health hazards, pneumatic conveying operates in a closed system, minimizing emissions and protecting both workers and the environment. This aligns with global sustainability goals and regulatory requirements, making it an attractive option for companies committed to reducing their ecological footprint. From an operational perspective, the system enhances productivity by reducing labor costs associated with manual handling and minimizing material loss. The automated nature of the process also reduces human error, leading to consistent and reliable material delivery. Furthermore, the closed system design allows for better temperature and humidity control, which is essential for maintaining the quality of sodium dithionite, a material that is sensitive to environmental conditions.
HeadPowder's pneumatic conveying solutions for sodium dithionite represent a cutting-edge approach to material handling that combines efficiency, safety, and environmental responsibility. By leveraging advanced engineering and innovative technology, the company provides tailored systems that meet the specific needs of various industries. The benefits of this method, including reduced dust exposure, improved material quality, and enhanced operational efficiency, make it a preferred choice for companies seeking sustainable and reliable material transport solutions. With a strong presence in Shandong, China, HeadPowder continues to lead the way in developing and implementing state-of-the-art pneumatic conveying systems that drive industrial progress while protecting the environment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top