For industries dealing with biological enzymes, efficient and reliable material handling is crucial. The Biological Enzyme Pneumatic Conveying System, developed by Shandong HeadPowder Engineering Co., Ltd., offers a sophisticated solution that combines advanced engineering with practical application. This system is designed to handle the unique challenges associated with enzyme powders, ensuring minimal degradation and maximum productivity.
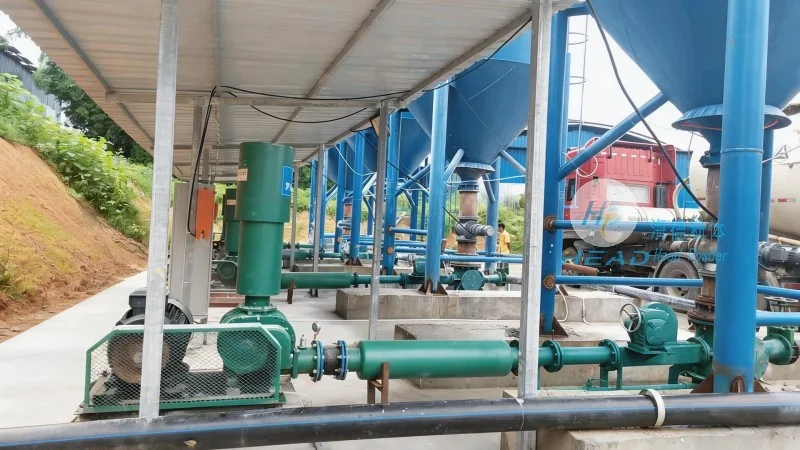
The Biological Enzyme Pneumatic Conveying System is a specialized piece of equipment engineered to transport biological enzyme powders through a pneumatic system. At its core, the system utilizes air pressure to move material from one location to another, eliminating the need for mechanical components that could potentially damage sensitive enzyme products. The equipment is constructed with materials that are compatible with enzyme powders, preventing contamination and maintaining product integrity throughout the conveying process.
The system operates on the principle of pneumatic conveying, where compressed air is used to create a flow that transports the material. Key components include the hopper, which stores the enzyme powder; the air compressor, which provides the necessary pressure; the conveying line, which transports the material; and the discharge valve, which controls the release of the material at the destination. Each component is designed to work in harmony, ensuring smooth and consistent operation. The hopper is equipped with a feeding mechanism that controls the flow of powder into the conveying line, while the air compressor maintains a consistent pressure to prevent clogging and ensure efficient transport. The conveying line is typically made of flexible or rigid tubing, depending on the application, and is connected to the discharge valve, which regulates the output of the material.
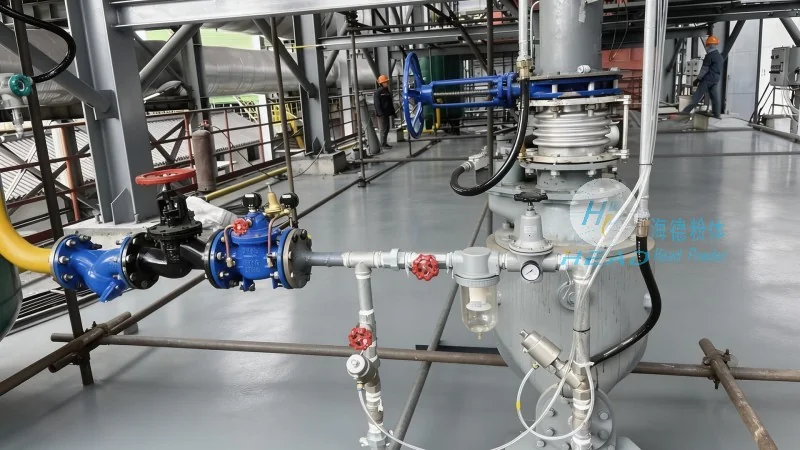
One of the primary advantages of this system is its ability to handle sensitive biological materials without compromising their quality. The system’s design minimizes exposure to air and moisture, which are common factors that can degrade enzyme powders. Additionally, the pneumatic conveying method reduces the risk of contamination from external sources, as the material is enclosed within the conveying line. The system also offers high efficiency in terms of material transport, with minimal downtime and low maintenance requirements. The use of compressed air allows for precise control over the flow rate, ensuring that the material is transported at the optimal speed for maximum product integrity. Furthermore, the system is scalable, allowing it to be adapted to different production volumes and operational needs.
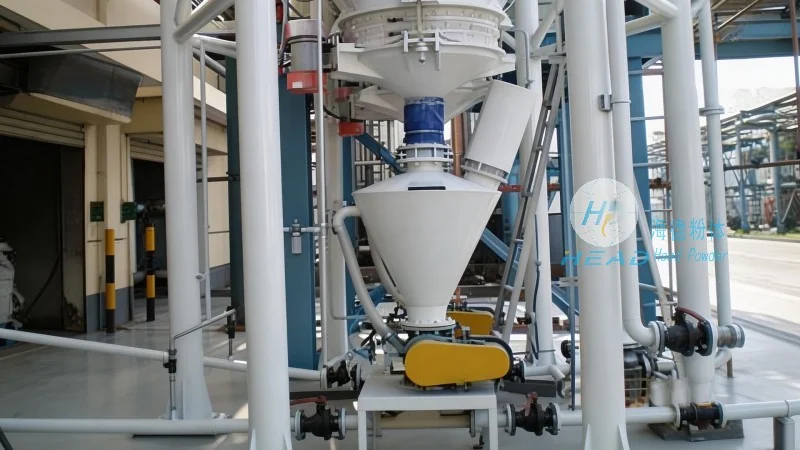
The Biological Enzyme Pneumatic Conveying System is widely used in various industries that rely on enzyme powders, such as food processing, pharmaceuticals, and biotechnology. In the food industry, it is used to transport enzymes used in baking and fermentation processes, ensuring that the enzymes remain active and effective. In the pharmaceutical industry, the system is used to convey enzymes used in drug manufacturing, maintaining the purity and potency of the product. In biotechnology, the system is used to transport enzymes used in research and development, where precision and consistency are critical. The system’s ability to handle sensitive materials makes it an ideal choice for industries where product quality is paramount.
Shandong HeadPowder Engineering Co., Ltd., the manufacturer of the Biological Enzyme Pneumatic Conveying System, is a leading provider of engineering solutions for material handling. The company is based in Shandong, China, and has a team of experienced engineers and technicians who specialize in the design and development of pneumatic conveying systems. The company offers comprehensive technical support, including installation, maintenance, and troubleshooting services. Additionally, the company provides customized solutions to meet the specific needs of its clients, ensuring that the system is tailored to the client’s operational requirements. The company’s commitment to quality and customer satisfaction has made it a trusted partner for many industries worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top