Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of powder handling technology, presents the intelligent tonne bag feeding station and pneumatic conveying system. This equipment is designed to efficiently handle bulk powder materials, offering a reliable solution for industries such as food, pharmaceuticals, chemicals, and more. The system integrates advanced automation and pneumatic technology to ensure precise and safe material transfer from bulk bags to processing equipment.
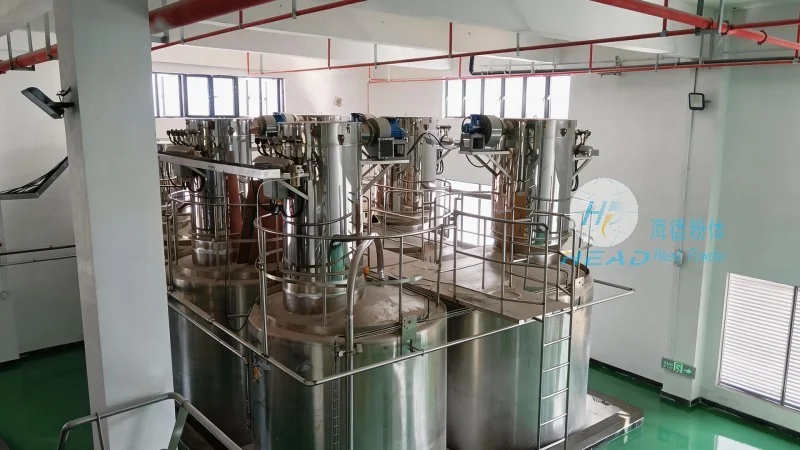
The intelligent tonne bag feeding station comprises several core components that work in harmony to achieve seamless material handling. The primary elements include the bulk bag unloading unit, the pneumatic conveying pipeline system, the dust collection and filtration system, and the control panel with automated feeding mechanisms. Each component is engineered to meet high standards of performance and durability, ensuring long-term operational efficiency.
The bulk bag unloading unit is a critical part of the system, responsible for safely and efficiently emptying material from tonne bags. It typically features a lifting and tilting mechanism that allows the bag to be positioned correctly for material discharge. The system may include a bag support frame and a discharge valve that controls the flow rate, preventing overloading or blockages. This component is designed to handle various bag sizes and types, ensuring versatility in material handling.
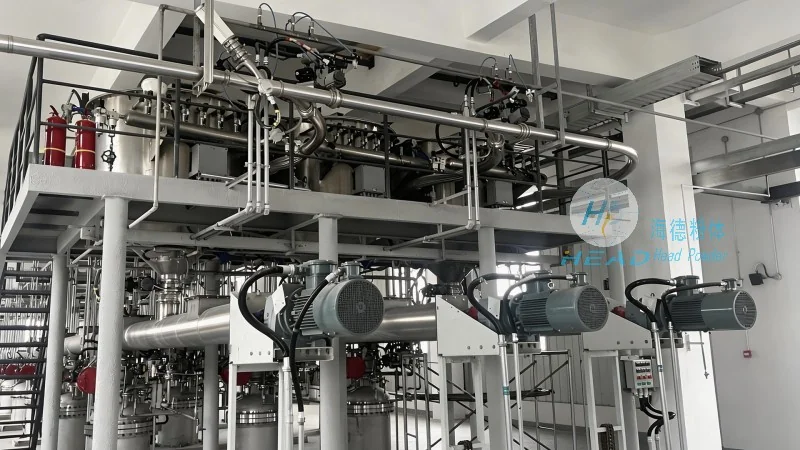
The pneumatic conveying system utilizes air pressure to transport powder materials through a network of pipelines. The system includes a blower or compressor that generates the necessary airflow, a hopper or receiver to collect the material, and a series of ducts and fittings to direct the material to the processing equipment. The design of the pipeline system is optimized for minimal pressure drop and maximum material flow, ensuring efficient and consistent material transfer. The system may also incorporate features such as air filtration and moisture control to maintain material quality.
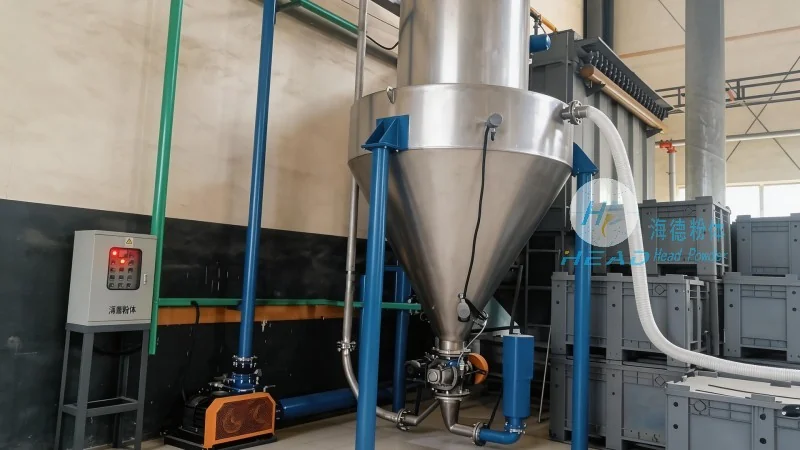
To ensure a safe and clean working environment, the system includes a dust collection and filtration system. This component captures airborne particles and dust generated during the material handling process, preventing contamination and protecting personnel from respiratory hazards. The system typically uses a combination of cyclone separators and bag filters to effectively remove dust from the air, with the collected material being returned to the system or disposed of as needed. This feature enhances operational safety and compliance with environmental regulations.
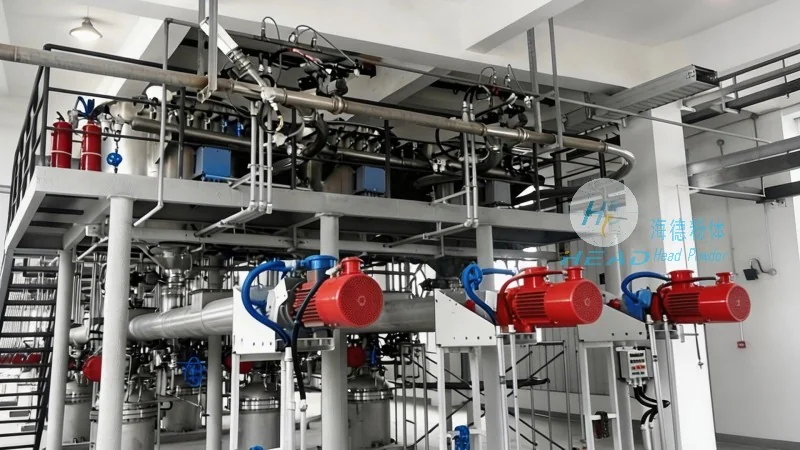
The control panel of the intelligent tonne bag feeding station is equipped with advanced automation features that allow for precise control and monitoring of the material handling process. It includes user-friendly interfaces, such as touchscreens or buttons, that enable operators to start, stop, and adjust the feeding rate. The system may also include sensors and feedback mechanisms to detect blockages, overfilling, or other issues, triggering automatic alerts or shutdowns to prevent equipment damage or material loss. This automation enhances operational efficiency and reduces the need for manual intervention, minimizing human error and improving overall productivity.
The intelligent tonne bag feeding station and pneumatic conveying system offers several advantages over traditional material handling methods. These include improved safety through reduced manual handling of bulk bags, enhanced efficiency through automated feeding and material transfer, and increased precision in material dosing. The system is particularly suitable for industries that require high purity and consistent material quality, such as pharmaceuticals and food processing. Additionally, the system is designed to be flexible and scalable, allowing it to adapt to different production requirements and future growth.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top