Heptahydrate magnesium sulfate, commonly known as Epsom salt, is a widely used chemical compound in various industrial applications. The efficient handling and transportation of this material often require specialized equipment, such as pneumatic conveyors. This article provides an overview of the heptahydrate magnesium sulfate pneumatic conveyor, focusing on its structure and operational principles.
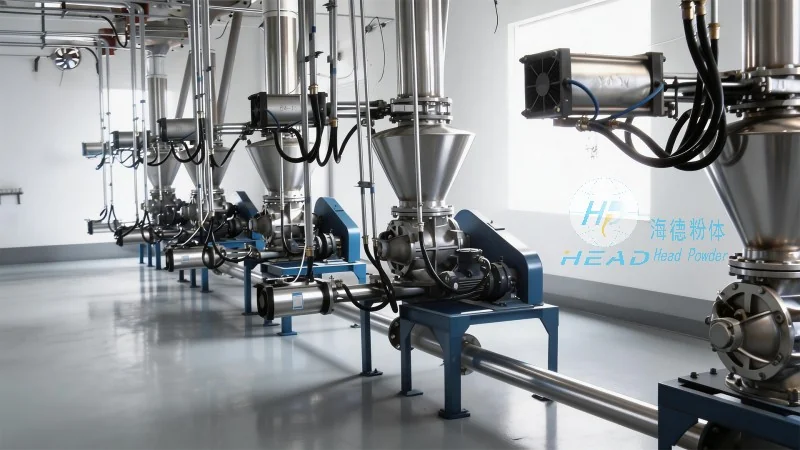
The heptahydrate magnesium sulfate pneumatic conveyor is a system designed to transport bulk materials like heptahydrate magnesium sulfate through a pipeline using air or gas as the conveying medium. This technology offers several advantages over traditional mechanical conveyors, including reduced equipment wear, lower maintenance costs, and the ability to handle materials in a dust-free environment. The conveyor system is particularly suitable for applications where material is transported over short to medium distances within industrial facilities.
The heptahydrate magnesium sulfate pneumatic conveyor consists of several critical components that work in tandem to ensure efficient material transport. The main components include the hopper, feeder, air compressor, pipeline system, and receiver. The hopper is responsible for storing the heptahydrate magnesium sulfate, while the feeder regulates the flow of material into the conveyor. The air compressor generates the necessary air pressure to move the material through the pipeline. The pipeline system, typically made of stainless steel or other corrosion-resistant materials, transports the material and air mixture. The receiver at the end of the pipeline collects the conveyed material as the air pressure decreases, allowing the material to settle and be discharged.
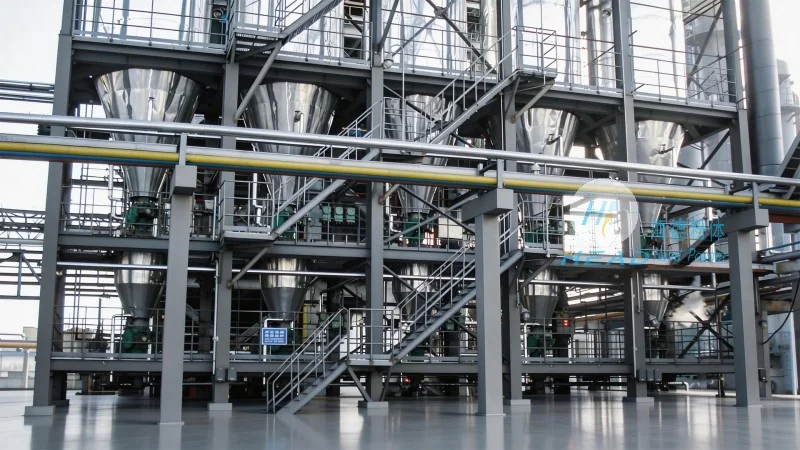
The operation of the heptahydrate magnesium sulfate pneumatic conveyor is based on the principle of air suspension. When the air compressor is activated, it produces a high-pressure air stream that is introduced into the pipeline. The feeder then releases a controlled amount of heptahydrate magnesium sulfate into the pipeline, where the material is suspended and carried by the air flow. The air velocity is carefully controlled to ensure that the material particles are fully entrained and transported without causing excessive wear on the pipeline or other components. The receiver at the end of the pipeline collects the material as the air pressure decreases, allowing the material to settle and be discharged.
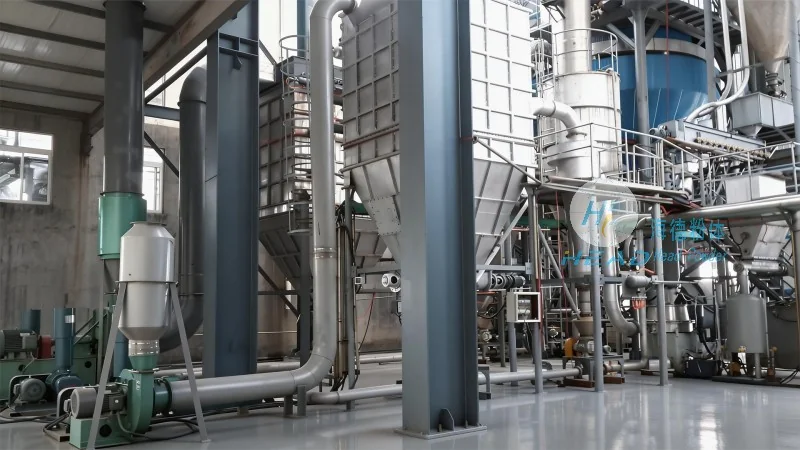
Implementing a pneumatic conveyor for heptahydrate magnesium sulfate offers numerous benefits for industrial operations. One of the primary advantages is the ability to handle the material in a dust-free environment, which enhances workplace safety and reduces the risk of material contamination. Additionally, the system minimizes material degradation and loss during transport, as the material is not subjected to mechanical abrasion or impact. The compact design of the pneumatic conveyor also allows for easier integration into existing industrial layouts, reducing installation costs and space requirements. Furthermore, the system can be easily scaled to accommodate varying material flow rates, making it versatile for different production needs.
The heptahydrate magnesium sulfate pneumatic conveyor is utilized in a wide range of industries that rely on the efficient handling of this chemical compound. In the pharmaceutical industry, the conveyor is used to transport heptahydrate magnesium sulfate to production lines for the manufacturing of various medications. In the agricultural sector, the system is employed to move the material to fertilizer production facilities, where it is incorporated into nutrient blends. The chemical industry also utilizes the conveyor for the transport of heptahydrate magnesium sulfate in the production of other chemical products. Additionally, the material is used in the food industry as a dietary supplement, and the conveyor ensures its safe and hygienic transport to processing facilities.
In summary, the heptahydrate magnesium sulfate pneumatic conveyor is a sophisticated and efficient system for transporting this important chemical compound. Its structure, which includes a hopper, feeder, air compressor, pipeline, and receiver, is designed to handle the material with minimal wear and maximum efficiency. The working principle of air suspension ensures that the material is conveyed smoothly and safely, offering advantages such as dust-free operation and reduced material loss. The system is widely used in various industries, including pharmaceuticals, agriculture, chemicals, and food processing, due to its versatility and effectiveness. For companies in need of reliable material handling solutions, the heptahydrate magnesium sulfate pneumatic conveyor from Shandong HeadPowder Engineering Co., Ltd. provides a robust and efficient option, reflecting the company's commitment to quality and industrial excellence.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top