HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems. This article provides an in-depth overview of the powder bin pneumatic conveyor, focusing on its structure, working principles, and key features that make it an efficient solution for bulk material handling in various industries.
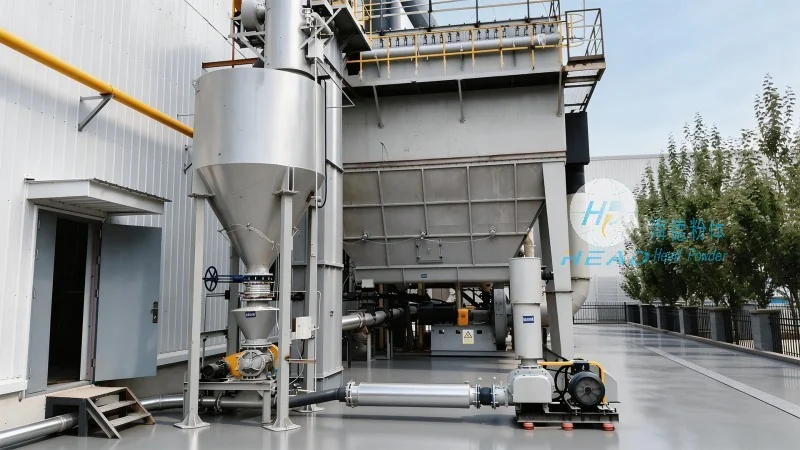
The powder bin pneumatic conveyor is a specialized equipment designed to transport dry powders and granular materials from a storage bin to a processing or packaging unit. It operates on the principle of air flow, utilizing a combination of positive and negative pressure to move materials through a pipeline system. This system is widely used in industries such as pharmaceuticals, food processing, chemical manufacturing, and cement production, where the safe and efficient transfer of powders is critical.
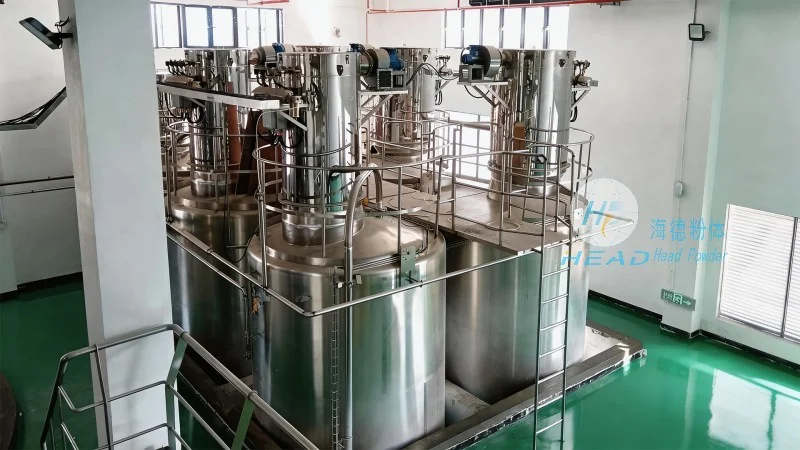
The powder bin pneumatic conveyor consists of several key components that work in tandem to ensure smooth material transfer. The main parts include a storage bin (or hopper), a feeder, a conveying pipeline, a dust collector, and a control system. The storage bin is typically made of stainless steel or other corrosion-resistant materials to accommodate various types of powders and prevent contamination. The feeder, often a rotary valve or a star feeder, regulates the flow of material from the bin into the conveying pipeline. The conveying pipeline is usually made of stainless steel or plastic, depending on the material being transported, and is equipped with pressure vessels or airlocks to maintain consistent air pressure. The dust collector is integrated to capture any airborne particles, ensuring a clean and safe working environment. The control system monitors and regulates the air pressure, flow rate, and material level, providing real-time feedback and adjustments to maintain optimal performance.
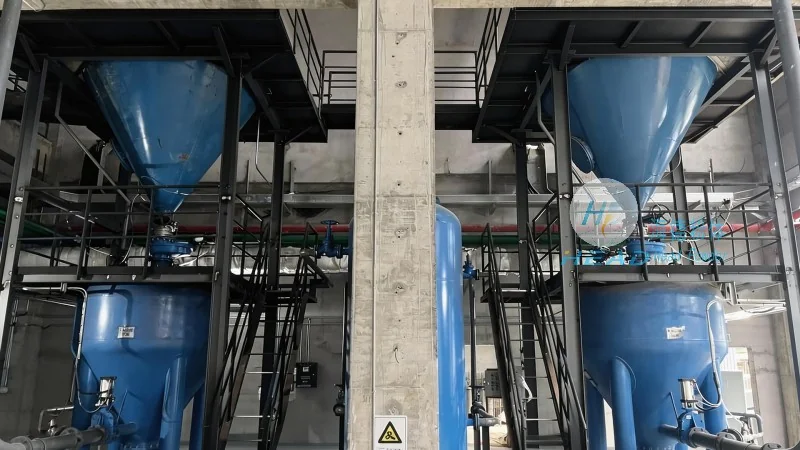
One of the primary advantages of the powder bin pneumatic conveyor is its ability to handle a wide range of materials, from fine powders to coarse granules, without the need for mechanical components that can cause wear and tear or material contamination. The system operates quietly and efficiently, reducing energy consumption compared to traditional mechanical conveyors. Additionally, the design allows for easy integration with existing production lines, minimizing downtime during installation and operation. The stainless steel construction ensures durability and hygiene, making it suitable for applications in the food and pharmaceutical industries where cleanliness is paramount. The system also offers flexibility in terms of layout, as the conveying pipeline can be customized to fit the specific space and workflow requirements of the facility.
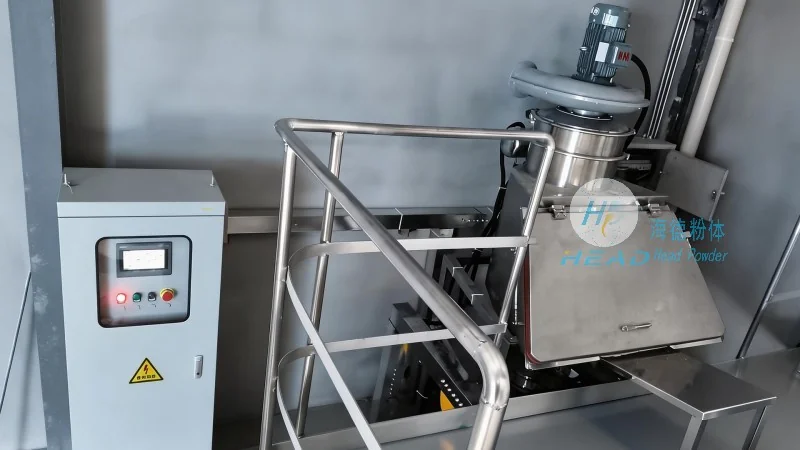
Powder bin pneumatic conveyors are commonly used in applications such as raw material feeding, product transfer between processing stages, and packaging line integration. They are particularly effective in handling materials that are prone to dust, caking, or segregation, as the enclosed system prevents material loss and maintains consistent quality. The system's performance is characterized by high efficiency, low maintenance costs, and reliable operation, which contributes to increased productivity and reduced operational costs for businesses. By utilizing this technology, companies can achieve seamless material flow, improve safety standards, and enhance overall operational efficiency in their production processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top