Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial solutions specializing in cement auxiliary materials handling. Our company, known as headpowder, is dedicated to delivering efficient and reliable pneumatic conveying systems for the cement industry. This article provides an overview of our cement auxiliary materials pneumatic conveying systems, detailing their structure and operational principles to help you understand how these systems enhance material handling efficiency in cement production processes.
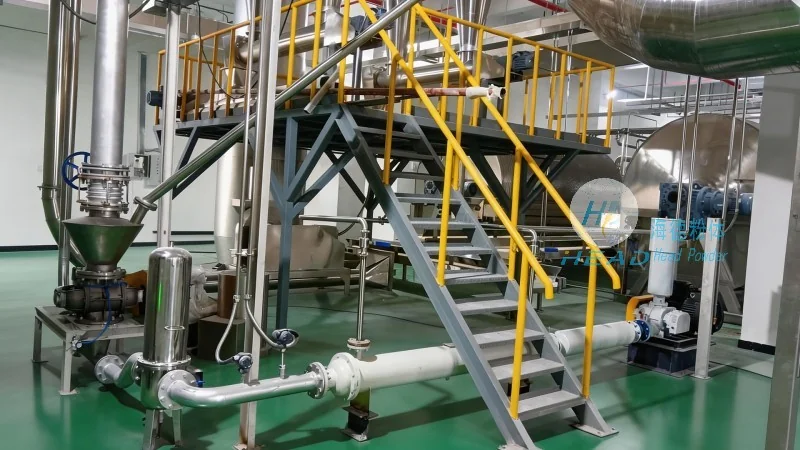
Pneumatic conveying systems are essential for transporting bulk materials like cement additives, fly ash, and other auxiliary components in the cement manufacturing industry. These systems utilize air pressure to move materials from one location to another, offering a flexible and efficient solution compared to traditional methods such as belt conveyors or bucket elevators. The primary goal of these systems is to ensure smooth, continuous material flow while minimizing downtime and maintenance requirements.
The cement auxiliary materials pneumatic conveying system from headpowder consists of several critical components that work in harmony to achieve effective material transport. These components include the material feed hopper, air compressor, conveying pipeline, control valve, and material discharge unit. Each component plays a vital role in the overall operation of the system.
Firstly, the material feed hopper is responsible for storing and feeding the auxiliary materials into the system. It is designed to handle various types of bulk materials, ensuring a consistent flow rate. The hopper is equipped with a feeder mechanism, such as a rotary valve or a screw feeder, which regulates the material discharge into the conveying pipeline. This component is crucial for maintaining a steady supply of materials to the system.
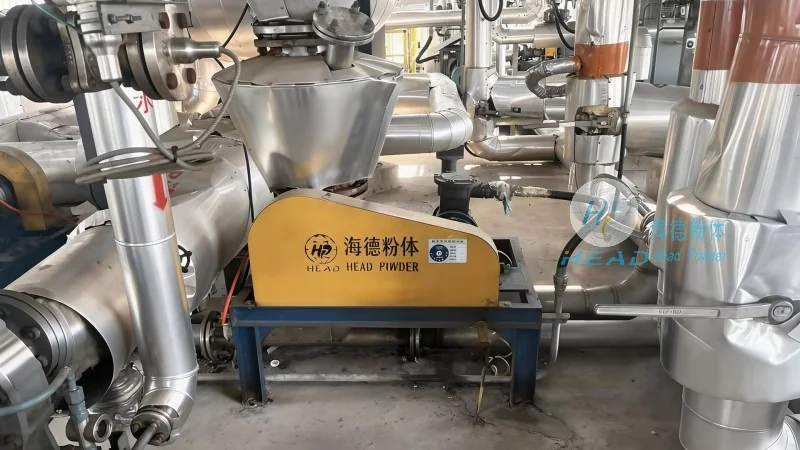
Secondly, the air compressor is the heart of the pneumatic conveying system. It generates the necessary air pressure to move the materials through the pipeline. The compressor is typically a positive displacement type, capable of delivering high-pressure air to ensure efficient material transport. The choice of compressor depends on the material characteristics, conveying distance, and system capacity.
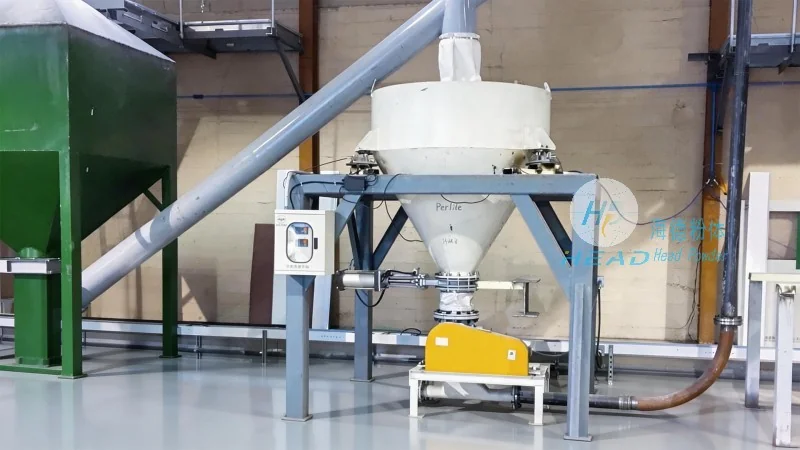
Thirdly, the conveying pipeline is a network of pipes that transports the materials from the feed hopper to the discharge point. The pipeline is made of durable materials like stainless steel or carbon steel, which can withstand the abrasive nature of cement additives. The pipeline design includes bends, elbows, and straight sections, all optimized to minimize pressure loss and ensure smooth material flow. The pipeline is also equipped with check valves and filters to prevent material blockages and maintain system efficiency.
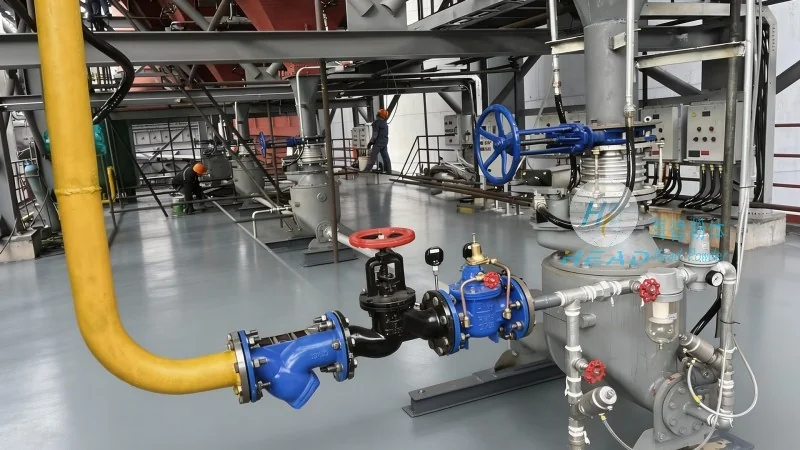
Fourthly, the control valve is a critical component that regulates the air flow and material discharge. It is typically a rotary or slide valve that can be adjusted to control the flow rate and pressure within the system. The control valve allows operators to manage the system's performance, ensuring optimal material transport under varying conditions.
Fifthly, the material discharge unit is responsible for releasing the materials from the pipeline at the destination point. It is designed to handle the final discharge of the auxiliary materials into the cement production process. The discharge unit may include a hopper or a silo, which collects the materials and feeds them into the next stage of the production line.
The operation of the cement auxiliary materials pneumatic conveying system follows a simple yet effective principle. When the system is activated, the air compressor generates high-pressure air, which is introduced into the conveying pipeline. The air flows through the pipeline, creating a low-pressure zone at the feed hopper. This pressure difference causes the auxiliary materials to be drawn into the pipeline and carried along by the air stream. The materials are then transported to the discharge point, where the air is released and the materials are deposited.
The system operates in a continuous mode, ensuring a steady flow of materials. The control valve regulates the air flow and material discharge, maintaining the optimal pressure and flow rate. The system can be adjusted to handle different material types and conveying distances, making it a versatile solution for various cement production applications.
Implementing a pneumatic conveying system for cement auxiliary materials offers several advantages over traditional material handling methods. Firstly, it provides a dust-free and clean operation, reducing the risk of material contamination and improving workplace safety. The enclosed pipeline system prevents dust emissions, which is crucial for maintaining a safe working environment in cement plants.
Secondly, the system offers high efficiency and reliability. The continuous operation and minimal maintenance requirements ensure that the material transport process is smooth and uninterrupted. The system can handle large volumes of materials, reducing the need for manual handling and labor costs.
Thirdly, the pneumatic conveying system is flexible and adaptable. It can be easily integrated into existing cement production lines and can be modified to accommodate changes in material types or production requirements. The system's modular design allows for easy expansion or reconfiguration, making it a cost-effective solution for long-term use.
Fourthly, the system enhances product quality by preventing material degradation and contamination. The enclosed pipeline and controlled environment ensure that the auxiliary materials remain in optimal condition, improving the overall quality of the cement produced.
The cement auxiliary materials pneumatic conveying system from headpowder is widely used in various applications within the cement industry. These systems are commonly employed to transport fly ash, slag, limestone, and other additives from storage silos to the cement grinding mills. The system ensures that these materials are delivered to the grinding mills in a consistent and controlled manner, improving the efficiency of the grinding process.
Additionally, the system is used in the transportation of raw materials from the quarry to the processing plant. The pneumatic conveying system allows for the efficient and safe transport of raw materials, reducing the risk of accidents and improving the overall productivity of the cement production line.
In summary, the cement auxiliary materials pneumatic conveying system is a critical component in modern cement production, providing efficient, reliable, and cost-effective material handling solutions. By understanding the structure and working principles of these systems, cement manufacturers can optimize their production processes and enhance overall operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top