Denitration fly ash, as a byproduct of flue gas desulfurization and denitrification processes in thermal power plants and industrial facilities, requires efficient handling and transportation. The pneumatic conveying line is a critical system designed to transport this ash from the denitration unit to storage or disposal sites. This article provides an overview of the denitration fly ash pneumatic conveying line, detailing its structural components and operational principles.
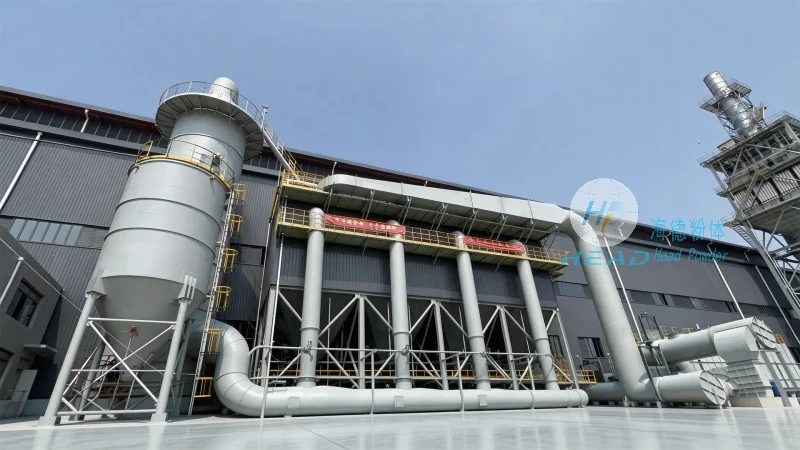
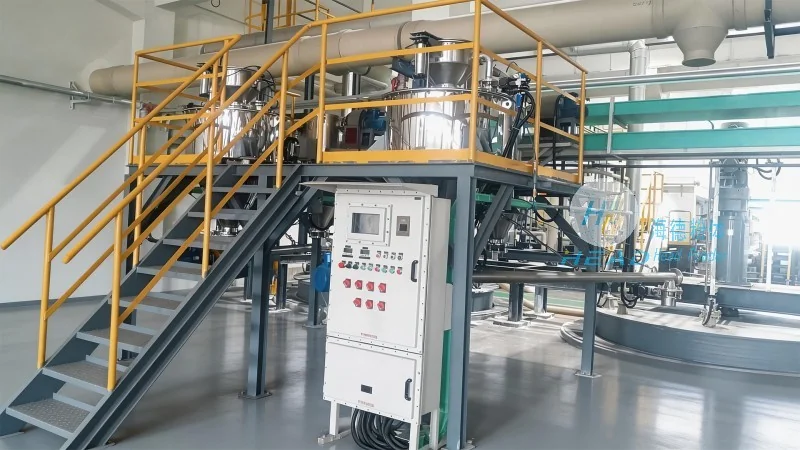
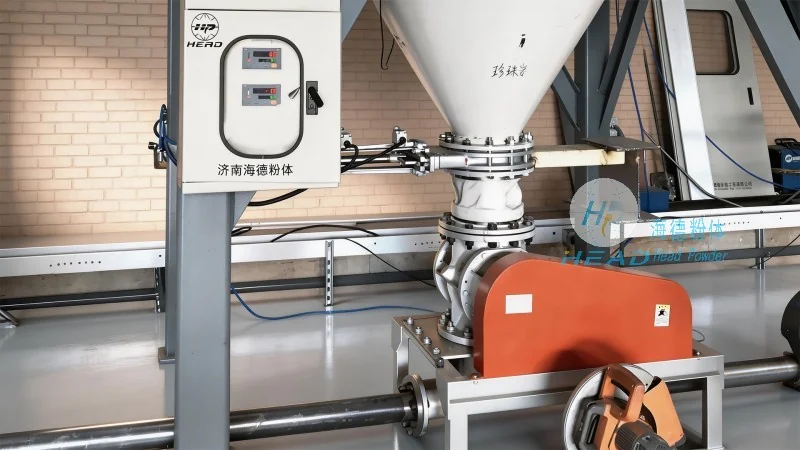
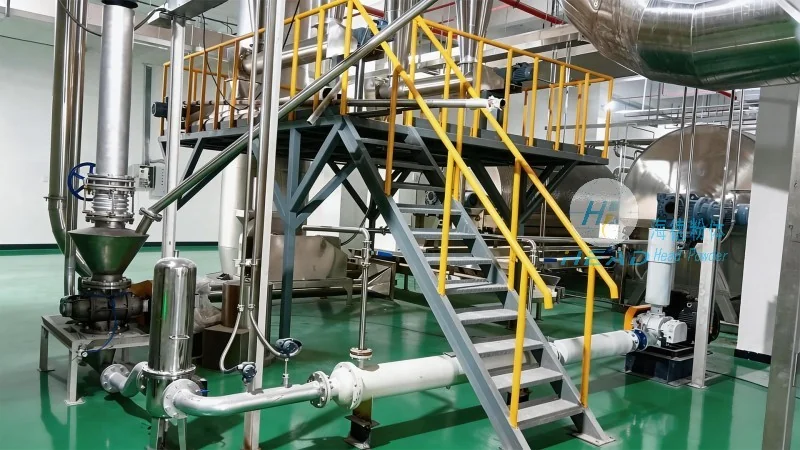
The denitration fly ash pneumatic conveying line is a sophisticated system composed of several critical components that ensure the efficient and reliable transport of denitration fly ash. The primary components include the ash collection hopper, which is typically designed with a conical bottom to facilitate the discharge of ash and prevent clogging. The feeding mechanism, often a rotary valve or a screw conveyor, is responsible for regulating the ash flow into the conveying pipeline, ensuring a consistent feed rate that matches the system's capacity. The pipeline itself is a key element, constructed from high-strength materials such as stainless steel (e.g., 316L) or special alloys to withstand the abrasive and corrosive nature of the fly ash. These materials are chosen to minimize wear and extend the service life of the system. The pipeline may include surge hoppers or pressure vessels to manage fluctuations in ash flow and pressure, preventing surges or drops that could disrupt operation. At the receiving end, the system incorporates a dust separator, commonly a cyclone or bag filter, which separates the ash from the conveying air using centrifugal force or filtration. The separated ash is then collected in a storage silo or hopper, while the clean air is either discharged to the atmosphere or recirculated back into the system to improve energy efficiency. Each component is carefully designed and integrated to handle the specific characteristics of denitration fly ash, including its fine particle size (typically 1-100 microns), high moisture content, and potential for agglomeration.
The operational principle of the denitration fly ash pneumatic conveying line is based on pneumatic transport, where air is used as the conveying medium to move solid particles. The process begins with the ash being discharged from the denitration unit into the collection hopper. The feeding mechanism then introduces the ash into the pipeline at a controlled rate, ensuring that the air-to-solid ratio is maintained within optimal limits. A fan or blower generates a high-velocity airflow within the pipeline, which entrains the ash particles and propels them forward. The air velocity is critical, as it must be sufficient to lift and transport the ash particles without causing excessive wear on the pipeline or components. The system typically operates under positive pressure, where the air pressure is higher than the ambient air pressure, ensuring that the ash is continuously moved through the pipeline. The flow of air and ash mixture travels through the pipeline, passing through any necessary bends, valves, or surge hoppers, until it reaches the receiving end. At the receiving end, the dust separator uses centrifugal force to separate the ash from the air, with the ash being collected in the storage silo and the clean air being discharged or recirculated. The system includes control mechanisms, such as pressure sensors and flow meters, to monitor and adjust the air volume and ash feed rate in real-time, ensuring that the system operates efficiently and safely. This dynamic control helps prevent issues like blockages or excessive pressure buildup, which could lead to system failure or damage.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top