Organic salt pneumatic conveying systems are essential in modern industrial processes, offering efficient and reliable methods for transporting bulk materials. This article provides an overview of the technology, focusing on the structural design and operational principles that enable effective material handling. By understanding these aspects, industries can optimize their material transport operations and enhance overall productivity, with solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
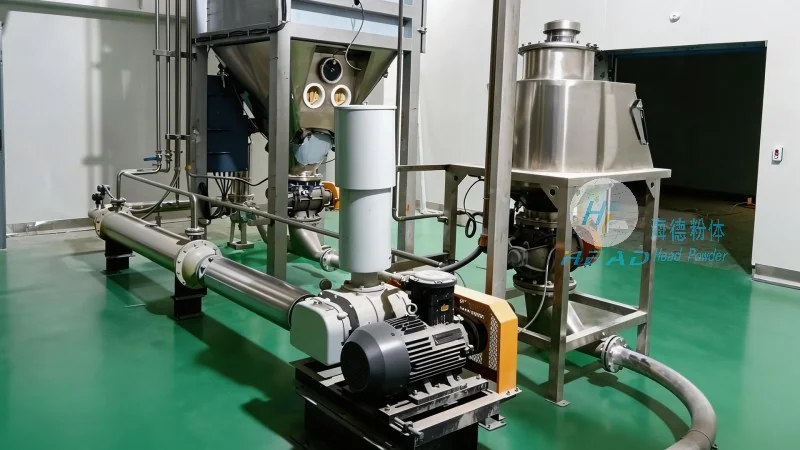
Organic salt, often used in chemical and food processing industries, requires specialized handling due to its unique physical and chemical properties. Pneumatic conveying systems provide a solution by utilizing air pressure to move these materials through pipelines. The system typically consists of a hopper, a blower, and a discharge unit, all working in tandem to ensure smooth material flow. This method is particularly advantageous for organic salts, as it minimizes material degradation and contamination compared to traditional mechanical conveying methods. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems tailored to the specific needs of organic salt applications.
The core components of an organic salt pneumatic conveying system include the material hopper, which stores the organic salt and feeds it into the system; the air blower, which generates the necessary air pressure to move the material; and the pipeline network, which transports the material from the hopper to the discharge point. Additionally, a filter system is integrated to capture any fine particles or dust, ensuring compliance with environmental regulations and maintaining system efficiency. Each component is designed to handle the specific characteristics of organic salts, such as their density, moisture content, and potential for caking. The company’s engineering team ensures that all components are robust and durable, suitable for long-term operation in industrial environments.
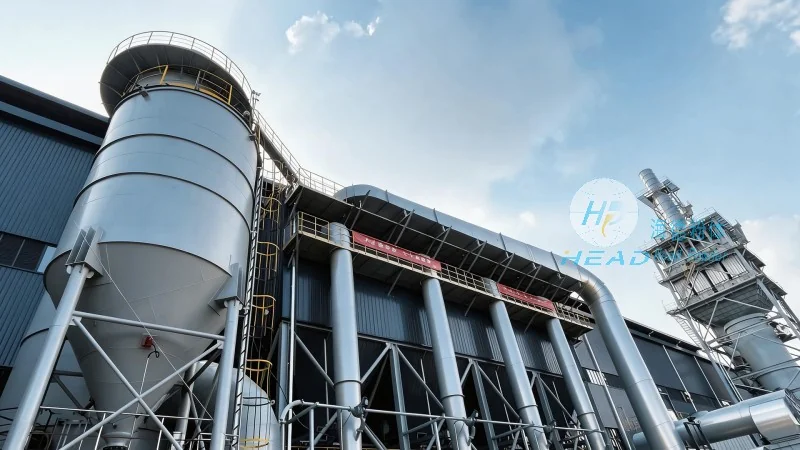
The operation of an organic salt pneumatic conveying system is based on the principle of fluidization and air movement. When the blower operates, it creates a low-pressure zone in the pipeline, which draws air and organic salt particles from the hopper. The material is then carried by the air stream through the pipeline to the discharge point. The system can operate in either positive or negative pressure modes, depending on the application requirements. Positive pressure systems are commonly used for long-distance or high-rise applications, while negative pressure systems are suitable for short-distance or low-level transport. The control system monitors the air pressure, flow rate, and material level, ensuring stable and efficient operation. Shandong HeadPowder Engineering Co., Ltd. offers both positive and negative pressure configurations, allowing customers to choose the most suitable option for their specific operational needs.
Compared to traditional conveying methods, organic salt pneumatic conveying offers several key advantages. First, it reduces material handling costs by eliminating the need for mechanical components like conveyor belts or buckets. Second, it minimizes product contamination and degradation, which is critical for organic salts used in food or pharmaceutical applications. Third, the system is flexible and can be easily integrated into existing production lines. Finally, it provides a safe and dust-free environment, improving workplace safety and reducing the risk of fire or explosion in environments where organic salts are handled. These benefits make pneumatic conveying systems a preferred choice for industries dealing with organic salts.
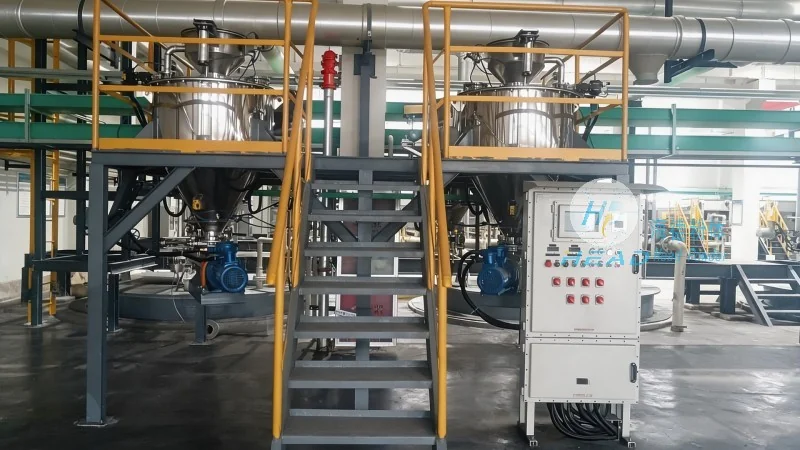
Organic salt pneumatic conveying systems are widely used in multiple industries, including chemical manufacturing, food processing, and pharmaceutical production. In chemical plants, these systems transport organic salts used in the production of fertilizers, detergents, and other chemical products. In food processing, they handle organic salts like sodium bicarbonate or citrates, ensuring hygienic and efficient material transport. In pharmaceutical industries, the systems are used to convey organic salts used in drug formulations, maintaining strict quality control standards. The versatility of the system makes it suitable for a wide range of applications, from small-scale laboratory use to large-scale industrial production. Shandong HeadPowder Engineering Co., Ltd. has successfully implemented these systems in various industries, demonstrating their effectiveness and reliability.
Proper maintenance is crucial to ensure the long-term performance and reliability of organic salt pneumatic conveying systems. Regular cleaning of the hopper, pipeline, and filter system is necessary to prevent clogging and material buildup. The air blower and motor should be inspected regularly for wear and tear, and lubricated as needed. Additionally, the system should be checked for air leaks, as even small leaks can affect the efficiency and effectiveness of the conveying process. Operational considerations include monitoring the material flow rate and pressure, adjusting the system as needed to maintain optimal performance. By following these maintenance and operational guidelines, industries can maximize the lifespan of their pneumatic conveying systems and minimize downtime. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive maintenance services to ensure that their systems operate at peak efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top