Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design, production, and installation of advanced pneumatic conveying systems for various bulk materials, including wheat and other grain products. The company's core focus is on providing efficient, reliable, and cost-effective solutions that meet the specific demands of the grain processing industry.
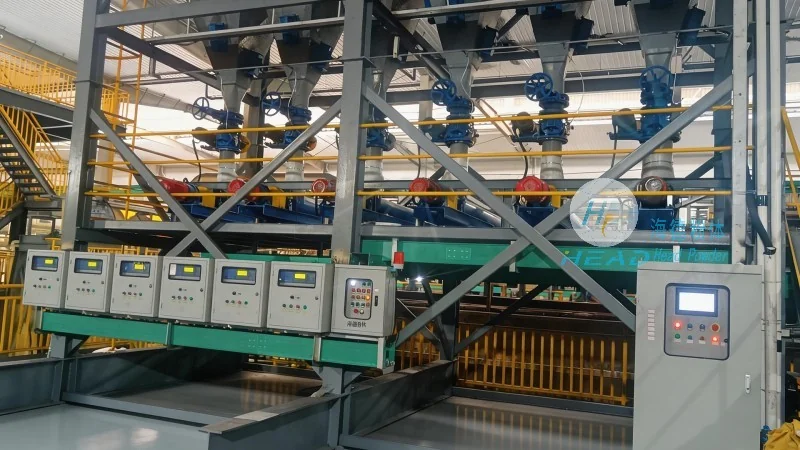
At HeadPowder, our pneumatic conveying systems are engineered to handle wheat and similar bulk materials with precision and efficiency. These systems utilize air as the primary medium to transport materials from one location to another, eliminating the need for mechanical components like belts or buckets that are common in traditional conveyor systems. The technology offers several advantages, including reduced maintenance costs, improved hygiene, and the ability to handle materials in a dust-free environment, which is crucial for maintaining the quality of wheat and other food products.
The operation of a wheat material pneumatic conveying system involves several key steps that ensure smooth and continuous material transport. First, the wheat is fed into the system through a hopper or a feeding device, which regulates the flow rate to maintain consistent pressure and flow. The material then enters the conveying line, where it is mixed with air under controlled conditions. The air, often supplied by a high-pressure blower or a vacuum pump, propels the wheat particles through the pipeline. The system typically includes a series of components such as a day tank, a filter, and a discharge valve, which work together to manage the air and material mixture. The process continues until the wheat reaches its destination, such as a storage silo or a processing unit. Throughout the operation, the system monitors pressure, flow rate, and other parameters to ensure optimal performance and prevent blockages or other issues.
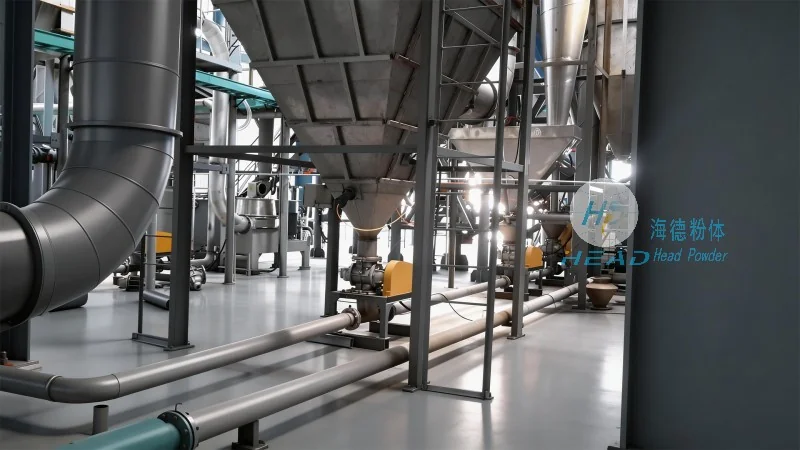
The working principle of a wheat material pneumatic conveying system is based on the principles of fluid dynamics and particle transport. The system operates by creating a pressure differential between the inlet and outlet of the conveying line. In a pressure system, a blower generates high-pressure air that pushes the wheat particles through the pipeline. The air velocity is carefully controlled to ensure that the wheat particles are suspended and transported without causing excessive wear on the system components. In a vacuum system, a vacuum pump creates a low-pressure environment that draws the wheat particles into the pipeline. The choice between pressure and vacuum systems depends on the distance, height, and material characteristics. For wheat, which is relatively light and has a low density, a pressure system is often preferred as it provides better control over the flow and reduces the risk of material degradation. The system also includes a filter to remove any dust or debris from the air, ensuring that the wheat remains clean and free from contaminants. The discharge valve at the end of the line controls the release of the wheat, allowing for precise control over the delivery rate.
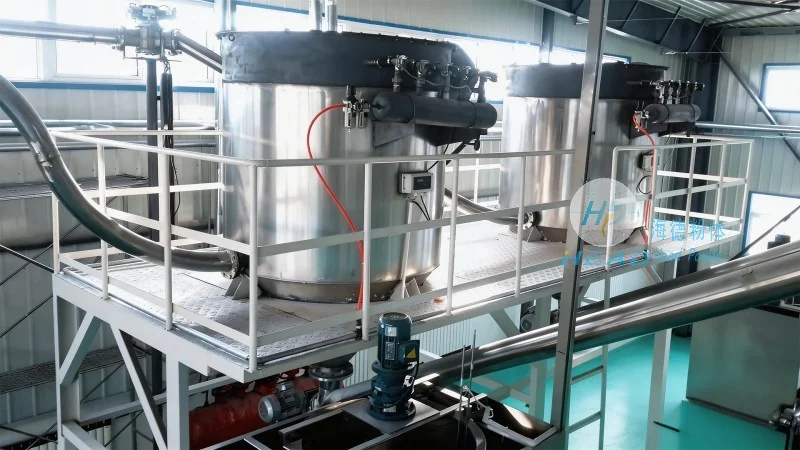
Wheat material pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. One of the primary benefits is the reduction in maintenance costs, as there are fewer moving parts and less wear on components. This leads to lower operational expenses and longer system life. Another advantage is improved hygiene, as the system operates in a closed environment, preventing dust and contaminants from entering the material. This is particularly important for wheat, which is a food product and must meet strict quality and safety standards. The system also allows for easy integration with other processing equipment, such as grain cleaners or storage silos, enabling a seamless flow of materials throughout the production process. Additionally, pneumatic conveying systems can handle a wide range of material sizes and densities, making them versatile for different applications in the grain industry.
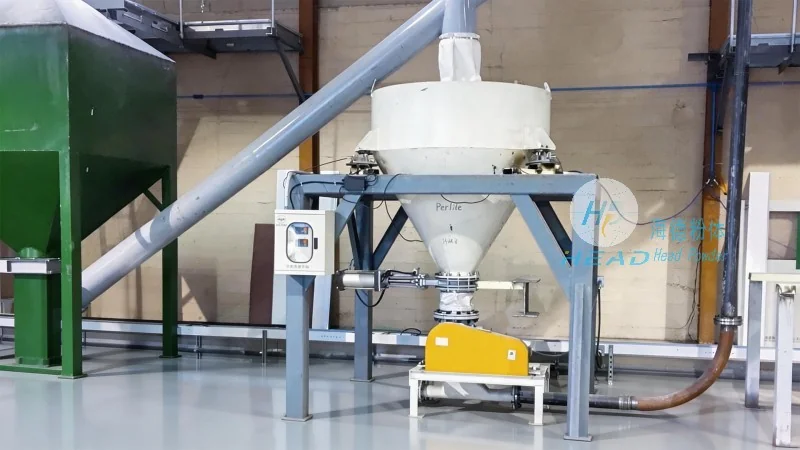
Wheat material pneumatic conveying systems are widely used in various stages of wheat processing, from storage and handling to processing and packaging. In storage facilities, the systems are used to transfer wheat from silos to processing units, ensuring a continuous supply of raw material. During processing, the systems can transport wheat to cleaning equipment, where it is sorted and cleaned before further processing. The systems are also used in the milling process to move wheat from the milling machine to the storage bins, where it is stored for later use. In addition, pneumatic conveying systems are used in the packaging stage to transfer wheat from storage to packaging machines, where it is packaged into bags or other containers. The versatility of the system makes it suitable for a wide range of applications, from small-scale farms to large-scale grain processing plants.
Proper maintenance is essential to ensure the long-term performance and reliability of a wheat material pneumatic conveying system. Regular maintenance includes checking the condition of the air filter, cleaning the conveying line, and inspecting the blower or vacuum pump for any signs of wear or damage. The system should also be checked for any blockages or leaks, which can cause a decrease in performance or even system failure. If a blockage occurs, the system should be shut down immediately and the blockage removed before resuming operation. The filter should be replaced regularly to prevent clogging, which can reduce the air flow and cause the system to work less efficiently. Additionally, the system should be inspected for any signs of corrosion or wear on the components, which can lead to leaks or other issues. By following a regular maintenance schedule, the system can operate at optimal performance and provide reliable service for many years.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top