HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer based in Shandong, China, specializing in the design, development, and production of advanced conveying equipment for bulk materials. The company focuses on providing reliable and efficient solutions for transporting stone aggregates and powder materials in various industrial applications.
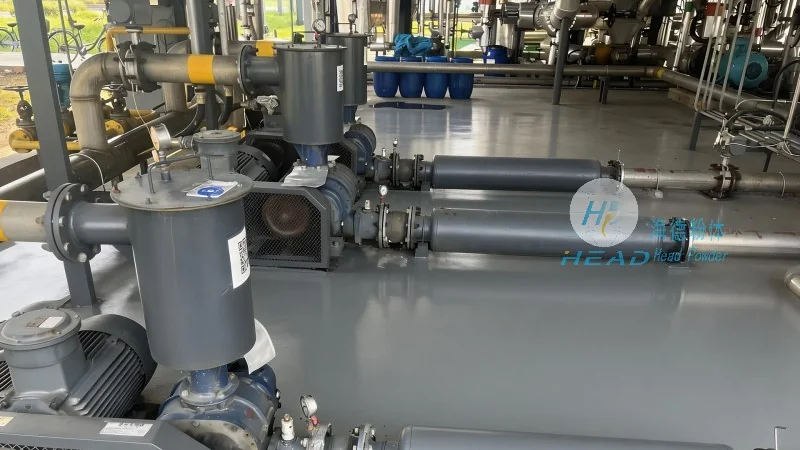
The operation of a stone aggregate powder conveyor typically begins with the loading of material into the hopper or feeding mechanism. The material is then fed into the conveyor system, which may include a screw conveyor, belt conveyor, or pneumatic conveyor depending on the specific design. The conveyor's motor drives the rotating components, such as screws or belts, to move the material forward. A control system monitors the flow rate and pressure, ensuring smooth and consistent transport. The material is discharged at the end of the conveyor, where it can be further processed or stored. The process starts with the preparation of the material and the setup of the conveyor system. The hopper or feeding hopper is filled with the stone aggregates or powder, ensuring a consistent supply. The control panel is then activated, which starts the motor and initiates the conveyor's movement. The material is fed into the conveyor's inlet, where it is transported along the conveyor path. The speed of the conveyor can be adjusted to control the flow rate, preventing overloading or underloading. The material is discharged at the outlet, where it is collected in a storage bin or transferred to the next processing stage. The entire process is monitored by the control system, which provides real-time data on the flow rate, pressure, and temperature. Any deviations from the set parameters are automatically adjusted to maintain optimal operation.
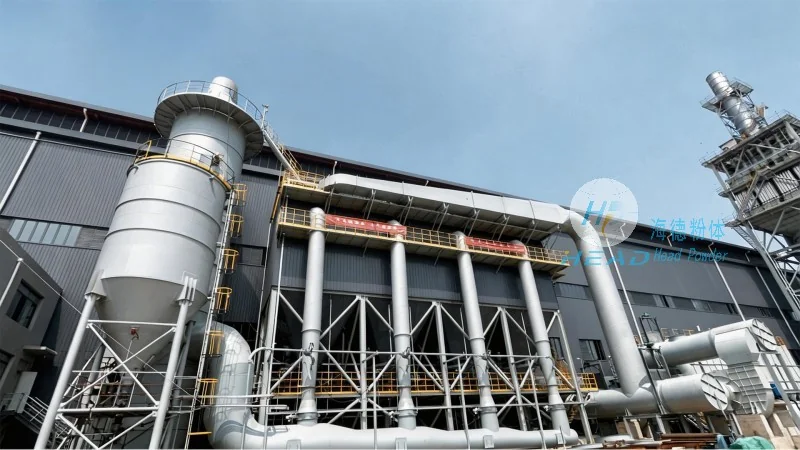
The working principle of stone aggregate powder conveyors relies on mechanical or pneumatic forces to transport bulk materials. Mechanical conveyors, like screw or belt conveyors, use rotating parts to push or pull the material along the conveyor path. The screw conveyor, for example, features a helical screw inside a tube, which rotates to move the material forward. The speed and pitch of the screw can be adjusted to control the flow rate. Belt conveyors use a continuous belt that moves over rollers, carrying the material from the inlet to the outlet. Pneumatic conveyors, on the other hand, use air pressure to transport the material through a pipeline. The material is suspended in the air stream and carried to the destination. The choice of conveyor type depends on factors such as material characteristics, distance, and required capacity. The mechanical design ensures that the material is moved efficiently and without excessive wear, making it suitable for handling abrasive stone aggregates. The control system plays a crucial role in maintaining the stability of the transport process, ensuring that the material flows consistently and safely.
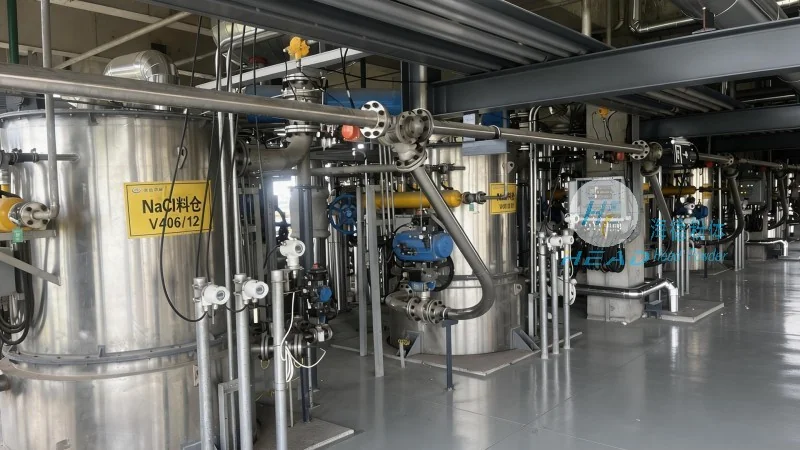
Stone aggregate powder conveyors consist of several key components that work together to ensure efficient operation. The hopper or feeder is responsible for receiving and storing the material before it is fed into the conveyor. The drive system, including the motor and gearbox, provides the necessary power to move the conveyor components. The conveyor itself, whether screw, belt, or pneumatic, is the main transport mechanism. The control system monitors and adjusts the operation, ensuring safety and optimal performance. The discharge mechanism allows the material to be released at the end of the conveyor. The hopper is designed to prevent material spillage and to provide a uniform feed to the conveyor. The drive system uses high-efficiency motors and gearboxes to ensure smooth and reliable operation. The conveyor components are made of durable materials, such as stainless steel or wear-resistant alloys, to withstand the abrasive nature of stone aggregates. The control system includes sensors and controllers that monitor the flow rate, pressure, and temperature, and can automatically adjust the conveyor speed or stop the system if an abnormal condition is detected.
Stone aggregate powder conveyors offer several advantages in industrial material handling. They provide a continuous and reliable transport of bulk materials, reducing the need for manual handling and improving safety. The equipment is designed to handle various material types, including abrasive and heavy aggregates, without causing wear or damage. The conveyors are also energy-efficient, with adjustable speed and capacity to match production needs. Additionally, they can be integrated into existing production lines, minimizing downtime and increasing overall productivity. The compact design of some models allows for installation in limited spaces, making them suitable for various industrial environments. The use of advanced materials and design ensures long service life and low maintenance costs, which contributes to the overall cost-effectiveness of the system.
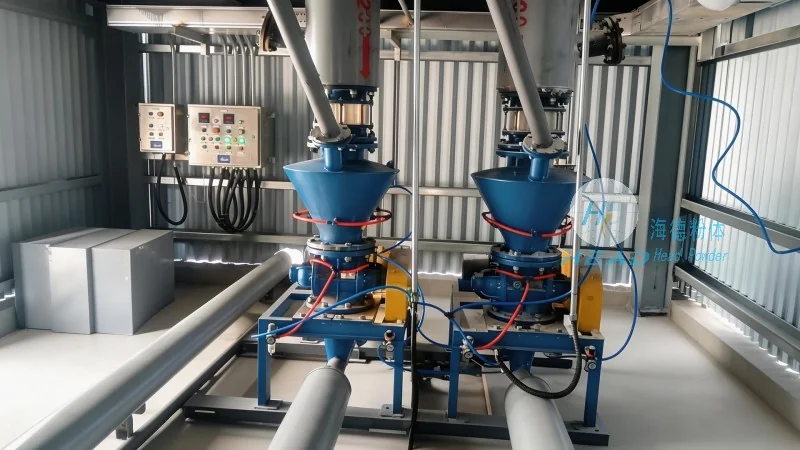
Stone aggregate powder conveyors are widely used in various industries due to their versatility and efficiency. In the construction industry, they are used to transport aggregates and cement for concrete production. The mining industry utilizes them to move crushed stone and ore from processing plants to storage or transportation facilities. The chemical industry uses conveyors to transport powders and granules in manufacturing processes. The food industry also employs them for handling bulk food products, ensuring hygiene and safety. Each application benefits from the consistent and controlled transport of materials, which improves product quality and reduces waste. The conveyors can be customized to meet specific industry requirements, such as handling hazardous materials or meeting strict hygiene standards. This flexibility makes them a preferred choice for many industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top