Cocoa powder is a vital component in the food and beverage sector, widely utilized in chocolate manufacturing, confectionery, and various baked goods. Efficient material handling is crucial to preserve product quality and operational efficiency. Pneumatic conveying systems, specifically designed for cocoa powder, offer a solution that minimizes contamination, reduces labor costs, and enhances process control. This article provides a comprehensive overview of the operation process and working principle of a cocoa powder pneumatic conveying machine, detailing key components, operational steps, and technical advantages.
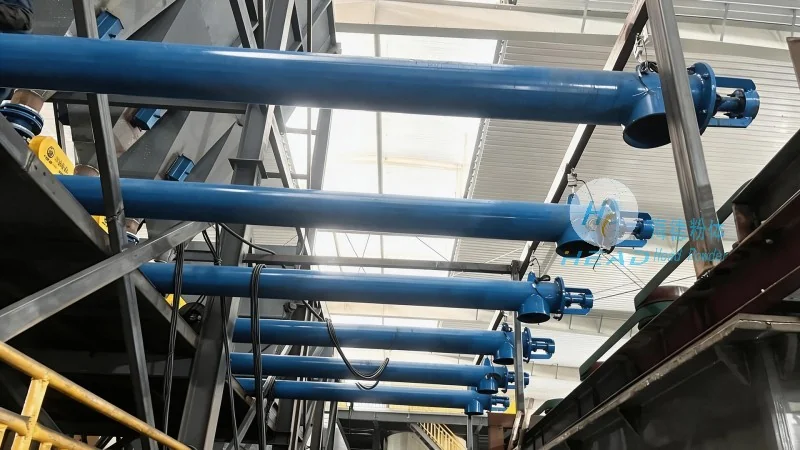
The fundamental components of a cocoa powder pneumatic conveying system include the hopper, feeder, air compressor, conveying line, and receiver. The hopper acts as the storage vessel for cocoa powder, ensuring a consistent feed to the system. The feeder, typically a rotary valve or screw feeder, regulates the powder flow into the conveying line. The air compressor generates the necessary pressure or vacuum to move the powder. The conveying line, usually constructed from stainless steel or other corrosion-resistant materials, transports the powder from the hopper to the receiver. The receiver is the final storage or processing container where the cocoa powder is deposited after air separation.
The operation process of a cocoa powder pneumatic conveying machine involves sequential steps for smooth material transfer. First, cocoa powder is loaded into the hopper. The feeder then discharges the powder at a controlled rate, ensuring steady flow into the conveying line. Simultaneously, the air compressor activates, producing compressed air that flows through the line. The compressed air creates a pressure differential, propelling the powder particles along the line. As the powder travels, it mixes with air, forming a slurry-like mixture. This mixture moves through the line until it reaches the receiver, where air is separated from the powder (via a cyclone or filter). The separated powder is collected in the receiver, while air is either vented or recycled to improve energy efficiency.
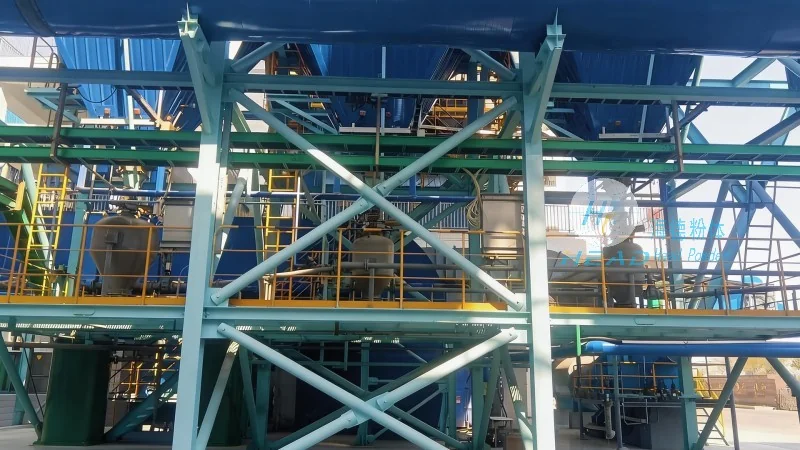
The working principle of a cocoa powder pneumatic conveying system is based on fluid dynamics and particle transport. Two primary modes exist: pressure and vacuum. In pressure conveying, the air compressor supplies compressed air to the hopper, creating positive pressure that forces powder through the line. This is suitable for short to medium distances and high flow rates. In vacuum conveying, a vacuum pump creates negative pressure at the receiver end, drawing powder from the hopper. Vacuum conveying is ideal for longer distances and fine powders prone to clogging. The choice depends on application requirements like distance, material characteristics, and desired flow rate.
Pneumatic conveying systems offer several benefits for cocoa powder handling. Firstly, they provide a closed system that prevents contamination from external sources, maintaining product purity and quality. Secondly, the system minimizes degradation by reducing exposure to air and mechanical stress—unlike mechanical conveyors, which can cause friction and particle breakage. Thirdly, automated feeding and conveying reduce labor costs and downtime, eliminating human error risks. Additionally, the system integrates seamlessly with other processing equipment, creating a cohesive production line.
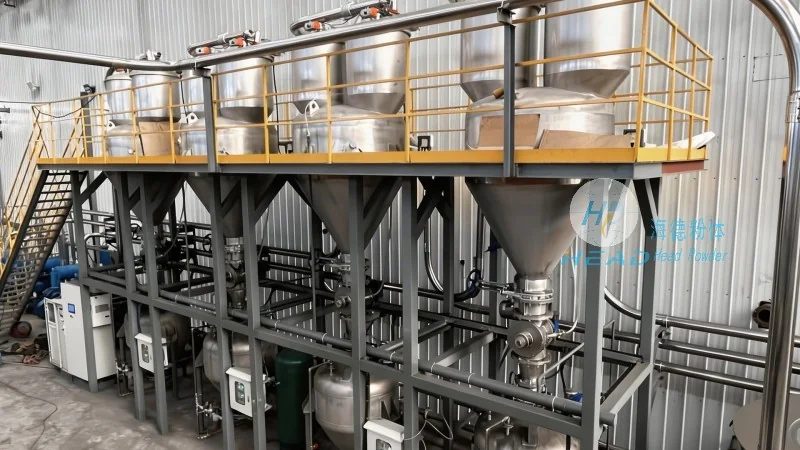
Cocoa powder pneumatic conveying systems are widely used in industries reliant on cocoa. The food and beverage industry, particularly chocolate manufacturers, heavily utilize these systems for transporting cocoa powder to production lines. Confectionery companies use them to move powder into mixers and blenders. Baked goods manufacturers also benefit for handling cocoa powder in products like brownies and cookies. The pharmaceutical and cosmetic industries may use similar systems for cocoa-based formulations, though primary applications remain in food processing.
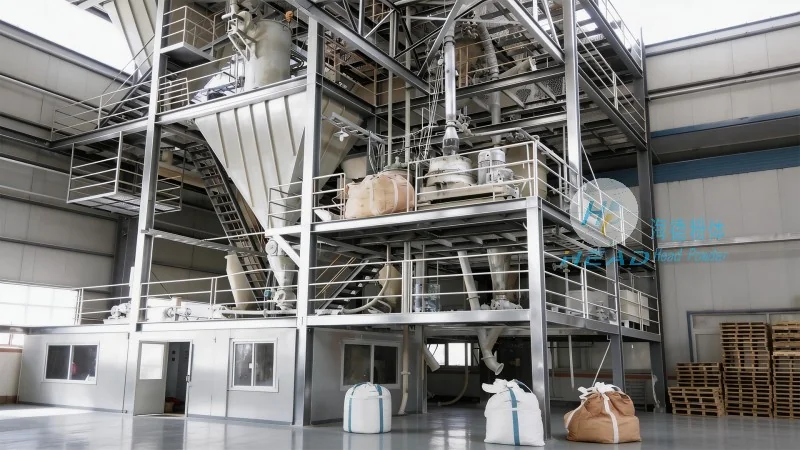
Proper maintenance and operational practices are essential for system longevity and efficiency. Regular cleaning of the hopper, feeder, and conveying line prevents residue buildup and clogging. The air compressor and vacuum pump must be checked for proper function, including pressure levels and air quality. Filters and cyclones should be inspected and replaced as needed. The system should operate within recommended flow rates and pressure ranges to avoid component wear. Operator training on system operation and maintenance is crucial to prevent accidents and ensure consistent performance.
In summary, the operation process and working principle of a cocoa powder pneumatic conveying machine are critical to efficient and reliable material handling. The system’s closed, contamination-free environment, combined with automated operation and energy efficiency, makes it ideal for the food and beverage industry. Understanding components, operational steps, and maintenance ensures optimized processes, preserving product quality, reducing costs, and enhancing performance. As demand for high-quality cocoa products grows, advanced pneumatic conveying systems remain essential for maintaining competitive advantages and meeting market demands.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top