Soil pneumatic conveyors are essential equipment in various industries, particularly in construction, mining, and environmental remediation, where the efficient and safe transportation of soil and other granular materials is critical. These systems utilize compressed air to move materials through a sealed pipeline, offering advantages such as minimal dust generation, flexibility in layout, and the ability to transport materials over long distances without the need for mechanical components like belts or buckets. The operation and working principles of soil pneumatic conveyors are designed to ensure reliable performance and optimal material handling.
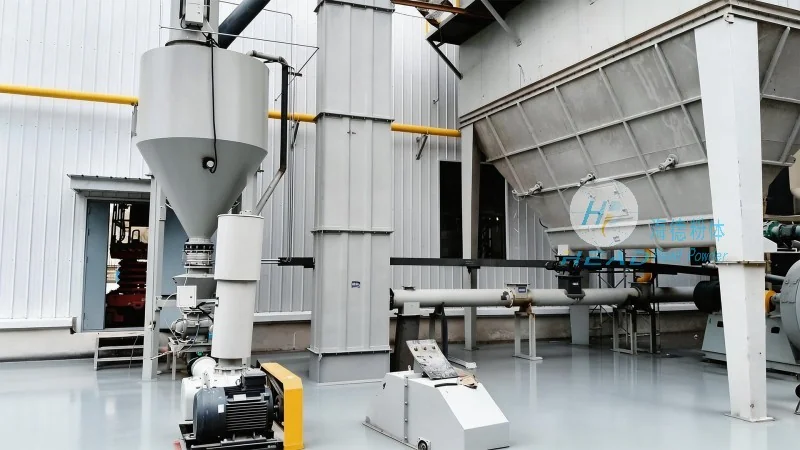
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of high-quality soil pneumatic conveyors. With a strong commitment to engineering excellence and customer satisfaction, HeadPowder has established itself as a trusted partner for businesses requiring robust and efficient material handling solutions. The company’s headquarters and manufacturing facilities are located in Shandong, China, providing a solid foundation for delivering products that meet international standards and client-specific requirements.
A soil pneumatic conveyor typically consists of several key components that work in concert to facilitate material transport. The primary components include a hopper or feeder for material intake, a blower or compressor to generate the necessary air pressure, a pipeline system for conveying the material-air mixture, a separation or cyclone unit to separate the material from the air, and a discharge outlet for the processed material. The working principle revolves around the use of compressed air to create a flow that entrains the soil particles, propelling them through the pipeline. As the material-air mixture travels through the system, the separation unit removes the air, allowing the soil to be discharged at the destination.
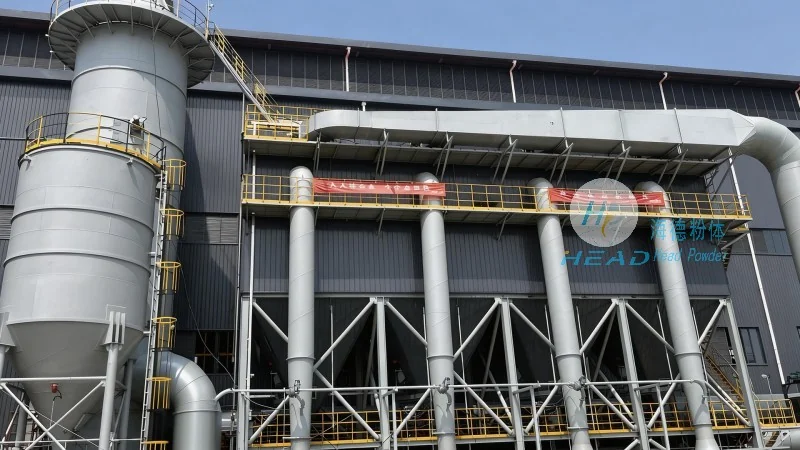
The operation of a soil pneumatic conveyor involves a systematic sequence of steps to ensure smooth and efficient material handling. The process begins with the loading of soil or other granular materials into the hopper or feeder. Once the hopper is filled, the feeder mechanism starts to discharge the material into the pipeline. Simultaneously, the blower or compressor is activated to generate compressed air, which is introduced into the pipeline at a controlled pressure. The compressed air creates a negative pressure or positive pressure environment within the pipeline, depending on the system design, to draw the material into the air stream. As the material-air mixture moves through the pipeline, it travels to the separation unit, where the air is separated from the soil particles. The separated soil is then discharged through the outlet, while the air is either recirculated back to the blower or released into the atmosphere, depending on the system configuration. Throughout the operation, the system monitors pressure, flow, and other parameters to ensure optimal performance and prevent any potential issues such as blockages or excessive pressure.
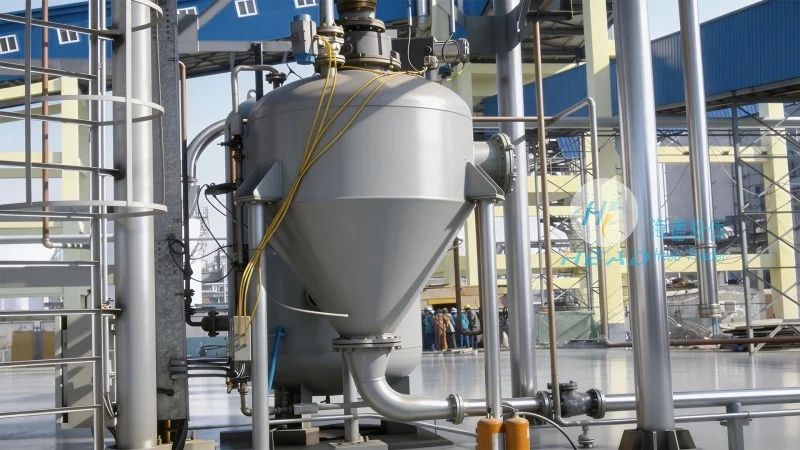
Soil pneumatic conveyors offer several advantages that make them a preferred choice for material handling applications. These include minimal dust generation, which enhances workplace safety and reduces environmental impact; flexibility in layout, as the pipeline can be arranged in various configurations to suit the site conditions; and the ability to transport materials over long distances without the need for mechanical components, which reduces maintenance requirements and operational costs. The equipment is widely used in construction sites for transporting excavated soil from excavation areas to disposal or processing sites, in mining operations for moving ore or tailings, and in environmental remediation projects for handling contaminated soil. The versatility of soil pneumatic conveyors makes them suitable for a wide range of applications where efficient and reliable material transport is essential.
To ensure the longevity and reliable operation of soil pneumatic conveyors, regular maintenance and adherence to safety guidelines are crucial. Maintenance tasks typically include checking the condition of the hopper and feeder, inspecting the blower or compressor for wear and tear, cleaning the separation unit to prevent clogging, and monitoring the pipeline for any signs of damage or leaks. It is also important to perform routine checks on the air pressure and flow rates to ensure they are within the recommended operating parameters. Safety considerations are paramount when operating soil pneumatic conveyors, as the equipment involves compressed air and moving parts. Operators should follow all safety protocols, including wearing appropriate personal protective equipment (PPE), ensuring proper ventilation to prevent the accumulation of dust or fumes, and conducting regular safety training to ensure all personnel are aware of the potential hazards. By adhering to these maintenance and safety practices, users can maximize the lifespan of their soil pneumatic conveyors and minimize the risk of accidents or equipment failure.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top