For industrial applications involving the transport of corn flour, efficient and reliable material handling systems are crucial. The pneumatic conveying system, specifically designed for corn flour, offers a solution that combines performance with operational simplicity. This article, presented by Shandong HeadPowder Engineering Co., Ltd. (headpowder), delves into the operation process and working principles of such a system, highlighting its benefits and practical implementation in industrial settings.
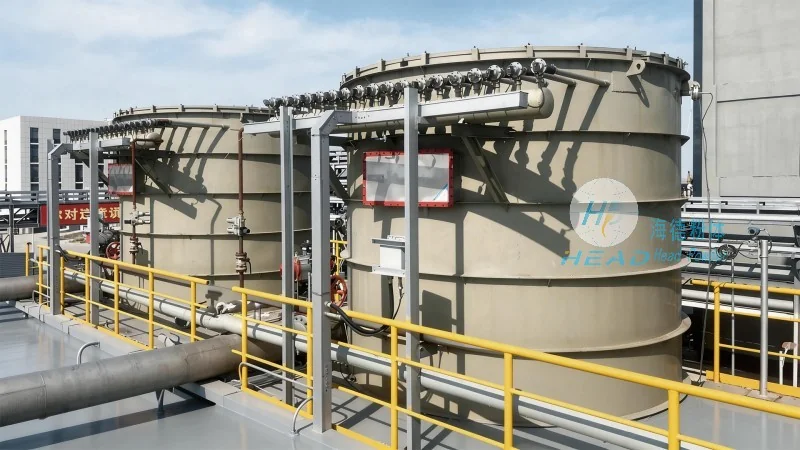
Corn flour, a fine powder with a high moisture content and potential for dust generation, requires specialized handling to ensure safety and efficiency. Traditional methods like belt conveyors or bucket elevators may not be suitable due to the risk of dust explosion and material degradation. Pneumatic conveying systems provide an enclosed, dust-free environment that minimizes these risks while maintaining high throughput. The system is particularly effective for transporting corn flour over short to medium distances, making it ideal for processing plants, storage facilities, and packaging lines.
The corn flour pneumatic conveying system consists of several critical components that work in tandem to achieve efficient material transport. These include the hopper, which stores the corn flour and feeds it into the system; the feeder, which controls the flow rate of the material; the air compressor or blower, which generates the air pressure needed to move the powder; the pipeline system, which transports the corn flour and air mixture; and the receiver, which collects the conveyed material at the destination. Each component plays a vital role in maintaining the system's performance and ensuring consistent operation.
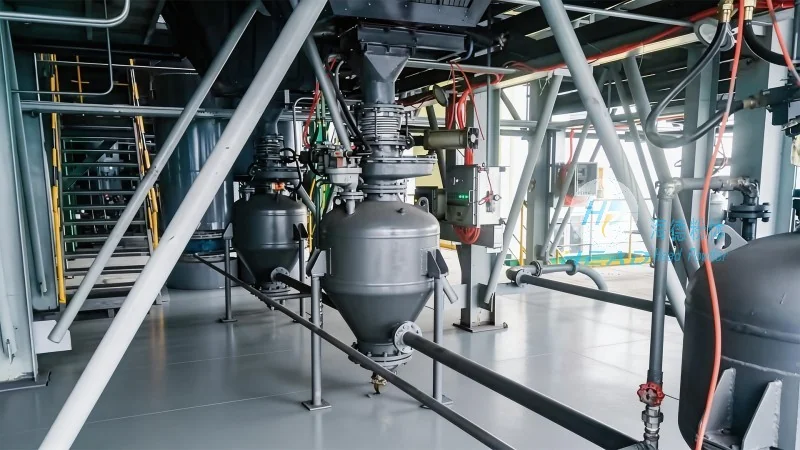
The operation of the corn flour pneumatic conveying system follows a systematic process. Initially, the corn flour is fed from the hopper into the feeder, which regulates the flow rate to match the system's capacity. Simultaneously, the air compressor supplies compressed air to the pipeline. The feeder then introduces the corn flour into the air stream, creating a mixture of powder and air. This mixture is then transported through the pipeline to the receiver, where the air is separated from the corn flour, typically using a cyclone or filter system. The separated air is then discharged, while the corn flour is collected in the receiver for further processing or storage. The system operates continuously, with the air pressure and flow rate adjusted to maintain optimal performance and prevent material blockages or degradation.
The operation process of the corn flour pneumatic conveying system can be broken down into several key steps to ensure smooth and efficient material transport. First, the system is started by activating the air compressor and feeder. The hopper is filled with corn flour, and the feeder is set to the desired flow rate. The air compressor then generates the necessary pressure, and the feeder introduces the corn flour into the air stream. The mixture travels through the pipeline to the receiver, where the air is separated and the corn flour is collected. The system is monitored continuously for pressure, flow rate, and material level to ensure optimal performance. Any adjustments to the flow rate or air pressure are made as needed to maintain consistent operation. The process continues until the material is fully conveyed to the receiver, after which the system can be shut down and the receiver emptied for further use.
Implementing a pneumatic conveying system for corn flour offers numerous benefits that enhance operational efficiency and safety. One of the primary advantages is the enclosed, dust-free environment, which significantly reduces the risk of dust explosions and improves workplace safety. The system also minimizes material degradation by preventing exposure to air and moisture, which can affect the quality of the corn flour. Additionally, the system provides high throughput and can transport corn flour over longer distances compared to traditional methods, making it suitable for larger processing facilities. The continuous operation of the system also reduces labor costs and increases productivity, as it eliminates the need for manual handling and reduces downtime. Furthermore, the system is easy to maintain and clean, as the enclosed design prevents material buildup and simplifies maintenance procedures.
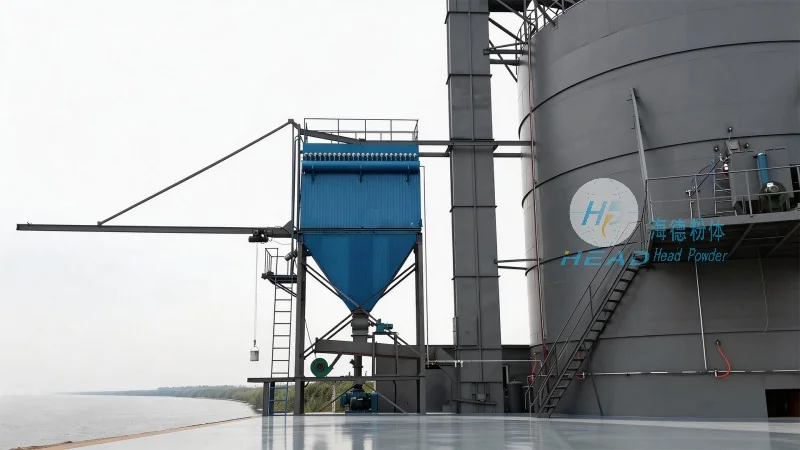
The corn flour pneumatic conveying system is widely used in various industrial applications, including food processing, pharmaceuticals, and chemical manufacturing. In food processing plants, the system is used to transport corn flour from storage silos to mixing and packaging lines, ensuring a consistent supply of material. In pharmaceutical facilities, the system is used to transport corn flour for the production of tablets and capsules, where dust control and material purity are critical. In chemical manufacturing, the system is used to transport corn flour as a raw material for the production of starch-based products, such as adhesives and coatings. The system can be customized to meet specific application requirements, including different flow rates, pipeline lengths, and material handling capacities. Implementation typically involves a professional installation and commissioning process to ensure the system operates efficiently and safely.
In conclusion, the pneumatic conveying system for corn flour is a highly effective solution for industrial material handling. By understanding the operation process and working principles of the system, businesses can optimize their material transport processes, improve safety, and enhance overall efficiency. The system's enclosed design, high throughput, and minimal material degradation make it an ideal choice for handling corn flour in various industrial settings. With proper installation and maintenance, the system can provide long-term benefits, reducing operational costs and improving product quality. As industrial processes continue to evolve, the use of advanced material handling systems like pneumatic conveying will remain critical in ensuring efficient and safe operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top