HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for micropowder materials. This article delves into the fundamental principles behind micropowder material pneumatic conveying equipment and explores the key characteristics of its operational scenarios.
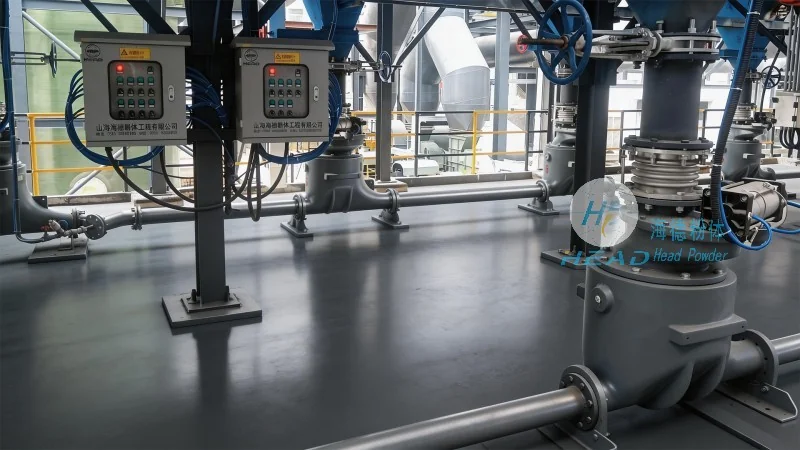
Micropowder materials, characterized by their fine particle size and often high moisture content or chemical reactivity, present unique challenges in material handling. Traditional methods like belt conveyors or bucket elevators may not be suitable due to issues such as dust generation, material segregation, or equipment wear. Pneumatic conveying offers a solution by utilizing air as the medium to transport these powders through a pipeline system. The core principle involves creating a pressure differential—either positive (pressure) or negative (vacuum)—to move the material from the source to the destination. For micropowders, the choice of conveying system (e.g., pressure or vacuum) depends on factors like material properties, distance, and process requirements.
The operation of micropowder pneumatic conveying systems is governed by several critical principles. First, the air velocity within the pipeline must be sufficient to overcome the gravitational and frictional forces acting on the particles, ensuring stable suspension. This is often referred to as the "minimum conveying velocity," which varies based on particle size, density, and shape. Second, the system must maintain a consistent air flow rate to prevent particle deposition or blockages. Third, the design of the conveying line, including bends, elbows, and expansion chambers, is crucial to minimize pressure drop and maintain material flow. For micropowders, which are prone to agglomeration or caking, additional features like in-line mixers or vibrators may be incorporated to maintain particle integrity during transport.
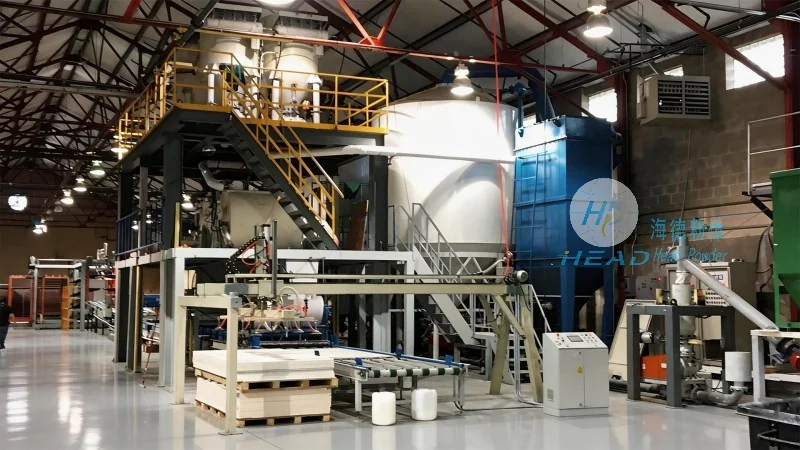
The operational scenarios for micropowder pneumatic conveying equipment are diverse and tailored to specific industrial applications. In the chemical industry, these systems are widely used to transport powders such as pigments, catalysts, and fine chemicals between reactors, storage silos, and processing units. The ability to handle high-purity materials without contamination is a key advantage. In the pharmaceutical sector, micropowder pneumatic conveyors are employed for the transfer of active pharmaceutical ingredients (APIs) and excipients, where strict hygiene and dust control are mandatory. The equipment is typically designed with stainless steel components and HEPA filters to meet GMP (Good Manufacturing Practice) standards. In the food and beverage industry, systems are used for conveying spices, flour, and other food-grade powders, ensuring compliance with food safety regulations. The working scene characteristics also include the need for flexibility in handling varying material flow rates, as production demands may fluctuate. Additionally, the equipment must be capable of integrating with existing process lines, allowing for seamless material transfer without disrupting production cycles.
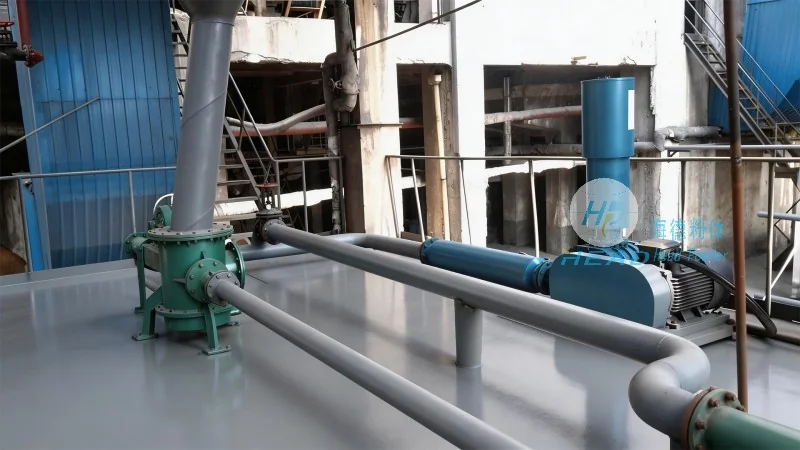
HeadPowder's micropowder pneumatic conveying equipment offers several technical advantages that make it suitable for demanding applications. The systems are engineered to handle a wide range of particle sizes, from sub-micron to several hundred microns, with minimal pressure loss. This efficiency reduces energy consumption and operational costs. The modular design allows for easy installation and maintenance, with components that can be replaced or upgraded as needed. For applications involving hazardous or reactive materials, the equipment is equipped with safety features such as pressure relief valves and explosion-proof designs. When selecting a micropowder pneumatic conveying system, several factors must be considered. The material's flowability, density, and moisture content influence the choice of conveying method (pressure or vacuum). The distance between the source and destination, as well as the number of transfer points, affects the system's layout and capacity. The required flow rate and the need for dust control or environmental compliance also play a role in the design. HeadPowder provides customized solutions based on these considerations, ensuring optimal performance and reliability for each application.
Micropowder material pneumatic conveying equipment, as exemplified by the solutions from HeadPowder, represents a sophisticated approach to material handling in industries where fine powders are prevalent. By understanding the fundamental principles of pneumatic transport and the specific characteristics of micropowders, these systems can effectively address the challenges of dust control, material integrity, and efficient transfer. The working scene characteristics highlight the versatility and adaptability of the technology, making it a critical component in modern industrial processes. With a focus on innovation and customer-centric design, HeadPowder continues to advance the capabilities of micropowder pneumatic conveying, supporting industries in achieving higher productivity and operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top