HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in the design, development, and production of pneumatic conveying equipment tailored for the petrochemical industry. This article delves into the fundamental principles of pneumatic conveying systems and highlights the key characteristics of their working scenarios, providing a comprehensive understanding of how these advanced technologies enhance operational efficiency in industrial settings.
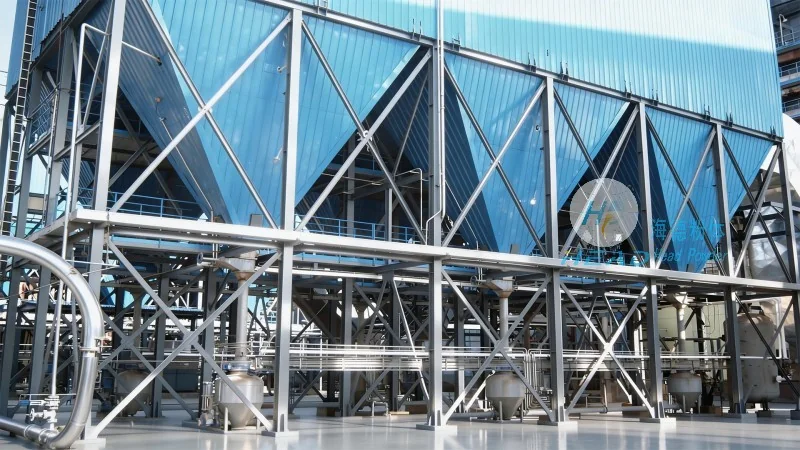
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using a stream of pressurized or vacuum air. The technology is widely adopted in the petrochemical sector due to its ability to handle a diverse range of materials, from fine powders to granules, with minimal product degradation. The fundamental principle revolves around creating a flow of air that moves the material through the system, either by creating a vacuum (suction) or by pressurizing the pipeline (pressure). This approach eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and increasing safety in hazardous environments typical of petrochemical operations.
There are two primary types of pneumatic conveying systems: suction (or negative pressure) and pressure (or positive pressure) systems. Suction systems operate by creating a vacuum at the material inlet, drawing the material into the pipeline along with the air. This method is ideal for applications requiring gentle handling of delicate materials, as it minimizes particle breakage and agglomeration. Conversely, pressure systems use compressed air to push the material through the pipeline, making them suitable for longer distances and higher material loads. Both systems rely on precise control of air flow and pressure to ensure consistent and reliable material transport.
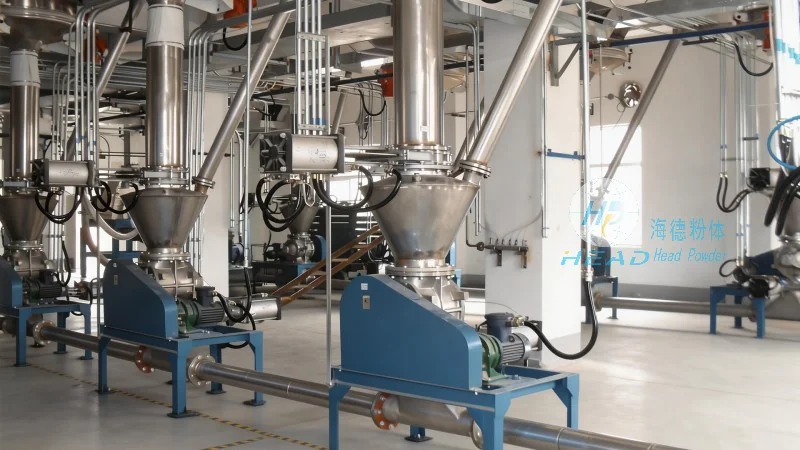
The working scenarios for pneumatic conveying equipment in the petrochemical industry are characterized by several critical factors that influence system design and performance. First, the materials being transported often include hazardous substances, such as chemicals, powders, or granules that may be flammable, toxic, or reactive. Therefore, the equipment must be constructed from materials resistant to corrosion and chemical exposure, ensuring long-term durability and safety. Additionally, the systems are designed to operate in environments with strict regulatory compliance, adhering to industry standards like ATEX for explosion-proofing and fire safety.
Another key characteristic is the need for high efficiency and low maintenance. Petrochemical plants operate on tight schedules, and downtime can lead to significant financial losses. Pneumatic conveying systems, with their minimal moving parts and automated control systems, reduce the risk of mechanical failure and simplify routine maintenance. This reliability is further enhanced by advanced monitoring technologies, such as pressure sensors and flow meters, which provide real-time data on system performance and alert operators to potential issues before they escalate.
Furthermore, the working scenarios often involve complex material handling processes, where multiple materials may need to be transported to different destinations or blended together. HeadPowder’s equipment is designed with flexibility in mind, allowing for the integration of multiple conveying lines, material separation systems, and storage tanks. This modular approach enables petrochemical facilities to adapt to changing production demands without significant infrastructure modifications.
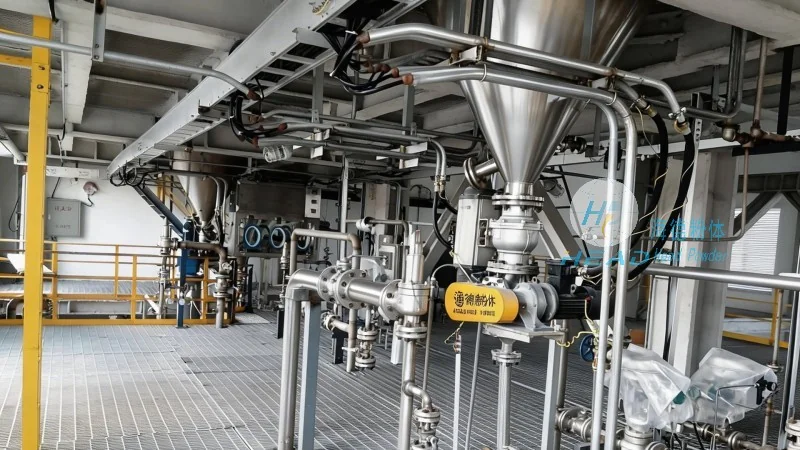
Pneumatic conveying equipment from HeadPowder is widely utilized in various petrochemical applications, including the transport of raw materials like limestone, clay, or coal, as well as finished products such as polymers, resins, and chemical powders. The technology’s ability to handle fine powders without clogging or degradation makes it particularly suitable for processes like polymerization and chemical synthesis, where material quality is paramount. Additionally, the systems contribute to improved workplace safety by eliminating the need for manual handling of bulk materials, reducing the risk of accidents and exposure to hazardous substances.
The advantages of pneumatic conveying in petrochemical operations extend beyond efficiency and safety. The systems offer cost savings through reduced energy consumption compared to traditional methods like belt conveyors, as well as lower labor costs due to automated operation. Moreover, the compact design of the equipment allows for installation in confined spaces, a common constraint in existing petrochemical facilities. These benefits make pneumatic conveying an attractive solution for both new plant constructions and retrofits in the petrochemical industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top