HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced pneumatic conveying systems. Our fully automatic bulk material pneumatic conveying machines represent the pinnacle of industrial automation, offering efficient, reliable, and safe solutions for material handling across various industries.
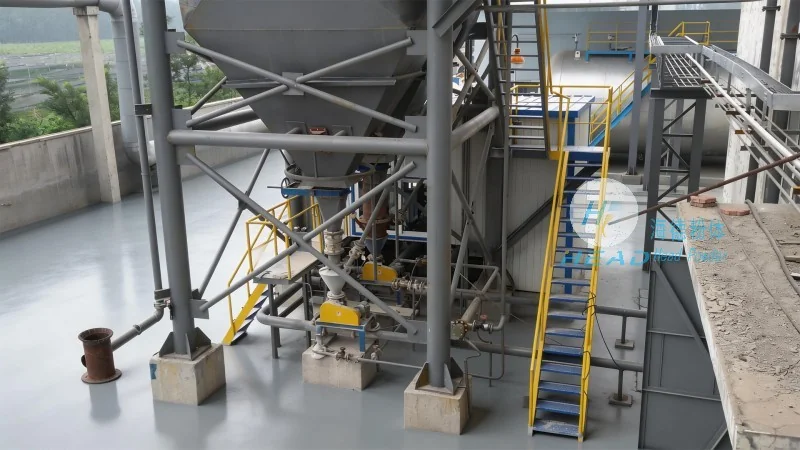
At the core of our product line is the fully automatic bulk material pneumatic conveying system, engineered to streamline the transport of bulk materials such as powders, granules, and fine particles. These systems integrate cutting-edge technology with robust engineering to ensure seamless operation, minimal downtime, and optimal performance in demanding industrial environments. HeadPowder's commitment to innovation ensures that each system is tailored to meet the specific needs of our clients, providing a customized solution that enhances productivity and operational efficiency.
The fundamental principle behind fully automatic bulk material pneumatic conveying involves the use of air pressure to move materials through a pipeline. The system typically operates by creating a pressure differential between the inlet and outlet, where compressed air or suction forces the material to travel from the source to the destination. Key components include the material hopper, air compressor, conveying line, and control system. The control system monitors and adjusts the air pressure and flow rate in real-time, ensuring precise material delivery and preventing blockages or overloading. This automated control mechanism eliminates the need for manual intervention, reducing human error and enhancing safety in the workplace.
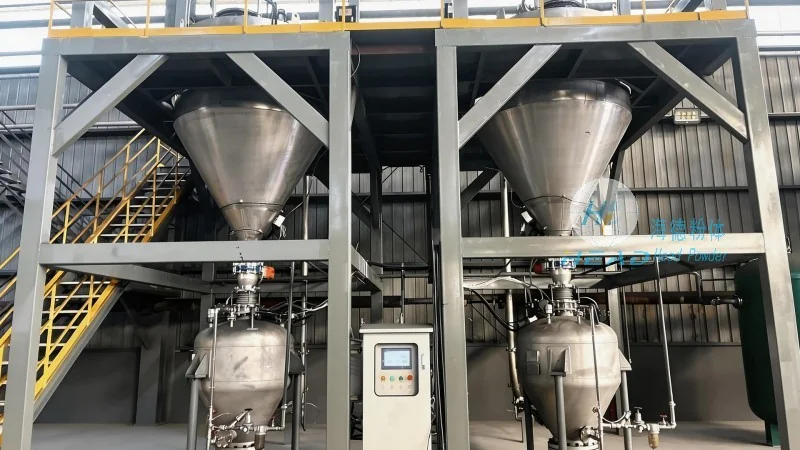
One of the most notable characteristics of fully automatic pneumatic conveying systems is their adaptability to diverse working environments. These systems are designed to operate in both indoor and outdoor settings, with options for horizontal, vertical, or mixed conveying paths. The flexibility in system configuration allows for integration into existing production lines or new facility setups, making them suitable for a wide range of applications. Additionally, the systems are equipped with advanced sensors and monitoring tools that provide real-time data on material flow, pressure, and system health. This data-driven approach enables proactive maintenance and troubleshooting, minimizing unexpected breakdowns and maximizing system uptime. The automated nature of the system also contributes to improved safety, as it reduces the risk of manual handling of materials and eliminates the need for operators to be in close proximity to the conveying equipment.
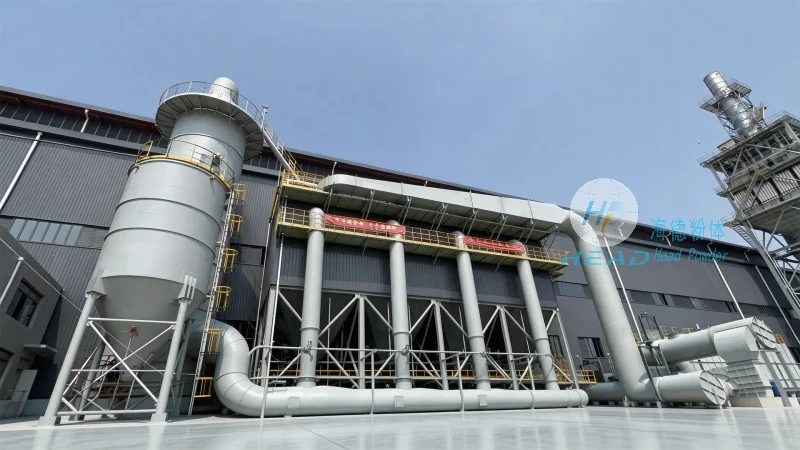
Fully automatic bulk material pneumatic conveying systems find extensive application across multiple industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, for example, these systems are used to transport ingredients like flour, sugar, and spices, ensuring hygienic and efficient handling that complies with strict regulatory standards. The pharmaceutical sector benefits from the system's ability to handle sensitive materials with minimal contamination risk, thanks to its sealed and controlled environment. In the chemical industry, the systems are employed to transport powders and granules safely, preventing dust explosions and ensuring compliance with safety protocols. The mining industry utilizes these systems for transporting raw materials from storage to processing units, enhancing operational efficiency and reducing labor costs. The versatility of the system makes it a valuable asset in any industrial setting where bulk material handling is critical.
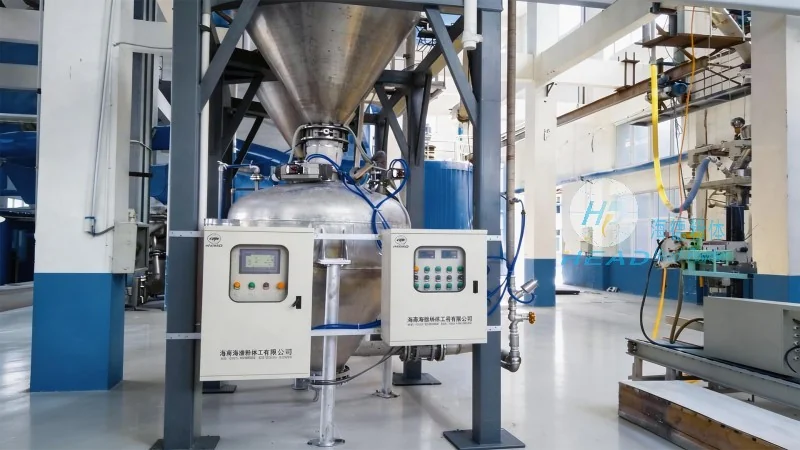
Implementing a fully automatic bulk material pneumatic conveying system offers numerous advantages over traditional manual or semi-automatic methods. The primary benefit is the significant reduction in labor costs, as the system operates with minimal human intervention. This not only lowers operational expenses but also improves safety by eliminating the need for manual material handling. Additionally, the automated control system ensures consistent and precise material delivery, reducing waste and improving product quality. The systems are also designed for easy integration with existing production lines, minimizing the need for major facility modifications. Furthermore, the advanced monitoring and diagnostic features allow for predictive maintenance, reducing downtime and extending the lifespan of the equipment. The reliability and efficiency of these systems make them a worthwhile investment for any business looking to enhance its material handling capabilities.
HeadPowder's fully automatic bulk material pneumatic conveying systems represent a sophisticated solution for modern industrial material handling challenges. By combining advanced technology with robust engineering, these systems provide efficient, reliable, and safe operation across various industries. The adaptability and automation features make them an ideal choice for businesses seeking to improve productivity, reduce costs, and enhance safety in their material handling processes. With a strong presence in Shandong, China, HeadPowder continues to lead the way in developing innovative solutions that meet the evolving needs of the industrial sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top