Guar gum powder, a critical industrial ingredient widely utilized in food, pharmaceutical, and chemical sectors, requires efficient and reliable handling systems to ensure consistent quality and process efficiency. The pneumatic conveying system for guar gum powder offers a solution that combines advanced technology with practical application, addressing the unique challenges of transporting fine powders like guar gum. This article explores the fundamental principles behind such systems and highlights the specific characteristics of working scenarios where they are most effectively utilized, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd.
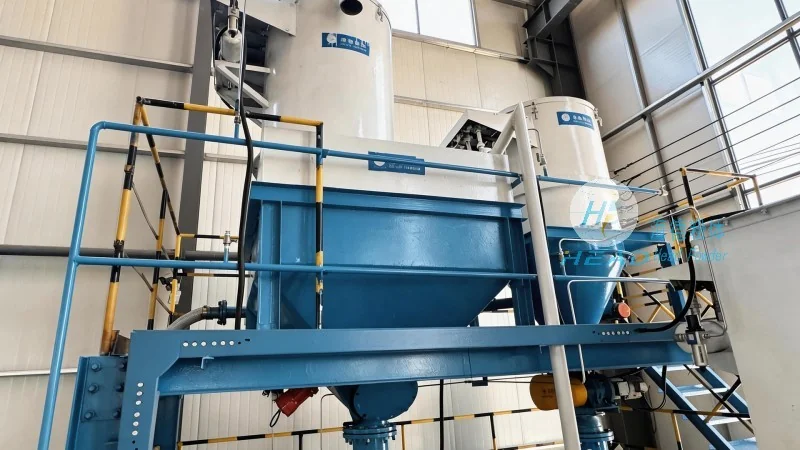
The core principle of a pneumatic conveying system involves the use of compressed air or gas to transport solid materials through a pipeline. In the case of guar gum powder, the system typically operates under positive pressure, where air is forced through the material to create a fluidized or suspended state. This process allows the powder to be moved from the source to the destination without the need for mechanical components like belts or buckets, reducing friction and wear. The system's efficiency depends on factors such as air velocity, material density, and pipeline design, all of which are optimized to maintain the powder's integrity and prevent caking or agglomeration.
At the heart of a guar gum powder pneumatic conveying system are several critical components that work in tandem to ensure smooth operation. The primary components include the material hopper, which stores the guar gum powder and feeds it into the system; the air compressor or blower, which generates the necessary pressure to move the material; the conveying line, which transports the powder from the hopper to the discharge point; and the dust collector or filter, which captures any fine particles and maintains air quality. Each component plays a vital role in maintaining the system's performance and ensuring the safe handling of the powder. For instance, the material hopper is designed with a low-angle or vibratory mechanism to prevent material bridging, while the air compressor is selected based on the required air volume and pressure to handle the specific characteristics of guar gum powder.
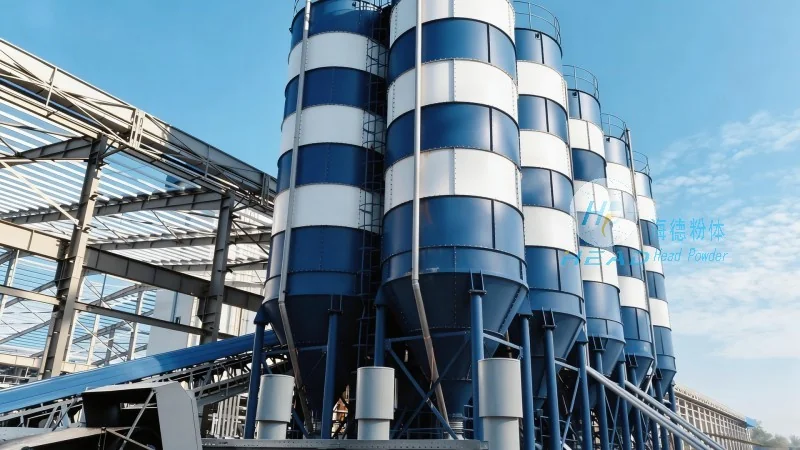
The pneumatic conveying system for guar gum powder is particularly well-suited for industrial environments where large volumes of fine powder need to be transported over short to medium distances. Common applications include the food processing industry, where guar gum is used as a thickening agent in beverages and dairy products; the pharmaceutical industry, where it serves as a binder or filler in tablet formulations; and the chemical industry, where it is used in water treatment and drilling fluids. In these scenarios, the system's ability to handle high volumes of material with minimal downtime and maintenance makes it an attractive solution. For example, in a food processing plant, the system can efficiently transport guar gum from storage silos to mixing tanks, ensuring consistent product quality and reducing the risk of contamination. Similarly, in a pharmaceutical manufacturing facility, the system can safely convey guar gum to blending equipment, maintaining the purity and integrity of the final product.
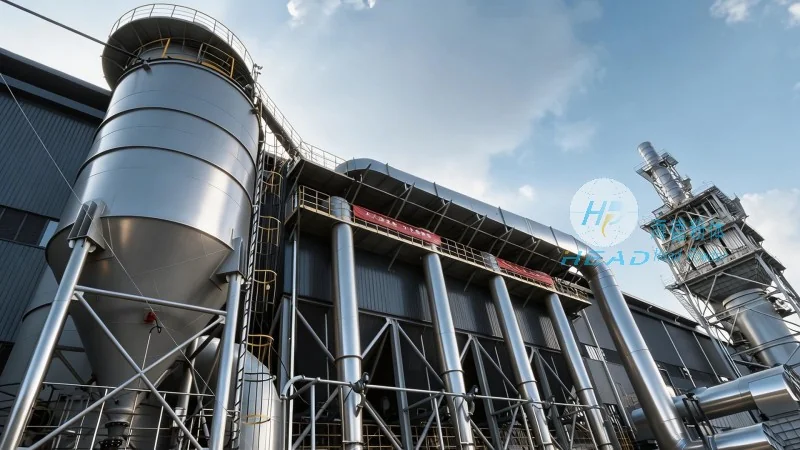
Compared to traditional mechanical conveying methods, the pneumatic system offers several advantages that are particularly beneficial for handling guar gum powder. One of the most significant advantages is the reduced risk of material degradation due to less contact with mechanical parts. This is crucial for guar gum, as it is sensitive to moisture and temperature changes, which can affect its viscosity and performance. Additionally, the system provides better control over the powder's flow and dispersion, ensuring uniform distribution in the final product. Another advantage is the ability to handle multiple materials or vary the conveying rate without significant modifications to the system. This flexibility makes the pneumatic conveying system a versatile solution for various industrial applications. Furthermore, the system's compact design and minimal space requirements make it suitable for facilities with limited floor space, such as urban manufacturing plants.
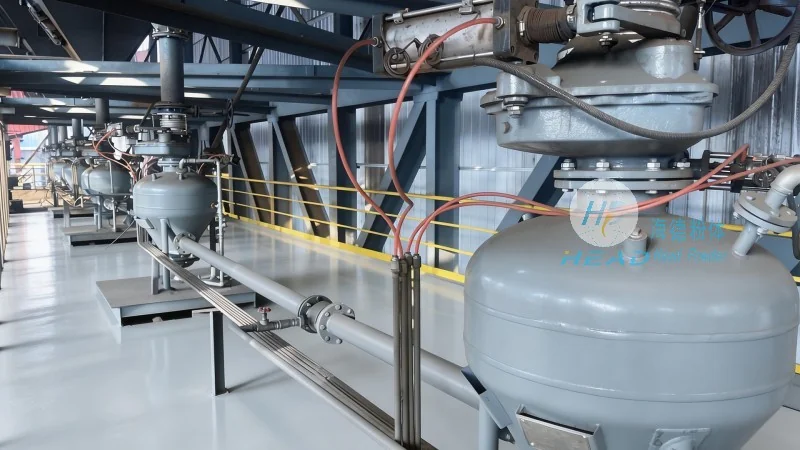
When designing a pneumatic conveying system for guar gum powder, several factors must be carefully considered to ensure optimal performance and reliability. The first consideration is the material's properties, including its particle size, density, and moisture content. Guar gum powder typically has a fine particle size, which can lead to high pressure drop and increased energy consumption if not properly managed. Therefore, the pipeline diameter and air velocity must be carefully selected to maintain a stable flow and prevent blockages. Another important consideration is the system's pressure and air volume requirements, which are determined by the distance to be covered and the volume of material to be transported. The choice of air compressor or blower also plays a critical role, as it must be capable of delivering the required pressure and volume while maintaining energy efficiency. Additionally, the system's integration with existing infrastructure, such as storage silos and processing equipment, must be considered to ensure seamless operation. Proper maintenance and regular inspections are also essential to prevent system failures and ensure long-term reliability.
In conclusion, the pneumatic conveying system for guar gum powder represents an advanced and efficient solution for handling fine powders in industrial applications. By leveraging the principles of fluidization and compressed air, the system provides a reliable and flexible method for transporting guar gum powder from storage to processing equipment. The key advantages, including reduced material degradation, better flow control, and compact design, make it an attractive option for various industries. However, successful implementation requires careful consideration of the material's properties, system design, and maintenance to ensure optimal performance. As the demand for guar gum powder continues to grow in industries such as food and pharmaceuticals, the pneumatic conveying system will remain a critical component in maintaining process efficiency and product quality. With proper design and operation, this system can effectively meet the challenges of handling guar gum powder, ensuring consistent performance and reliability in industrial settings.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top