For industrial applications involving the handling of magnesium sulfate, efficient material transport is crucial to ensure smooth production processes and maintain operational efficiency. Pneumatic conveying systems have emerged as a reliable solution for transporting magnesium sulfate materials, offering advantages such as reduced dust generation, improved safety, and enhanced process control. This article explores the fundamental principles behind magnesium sulfate material pneumatic conveying and highlights the key characteristics of its working scenes, providing insights into how these systems operate in practical industrial settings.
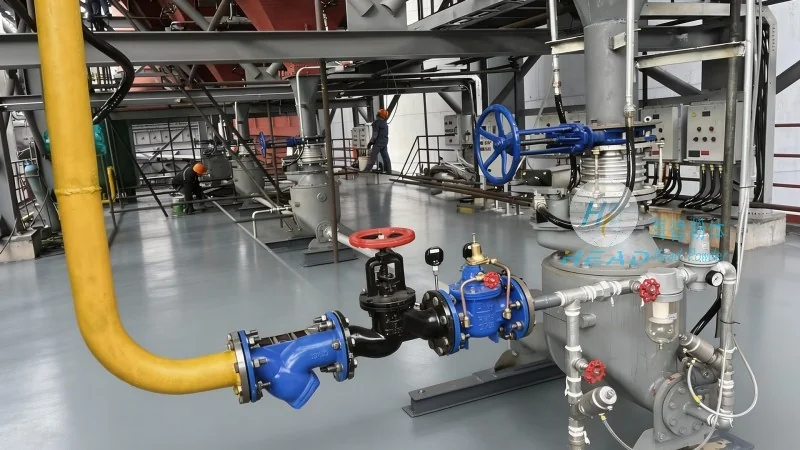
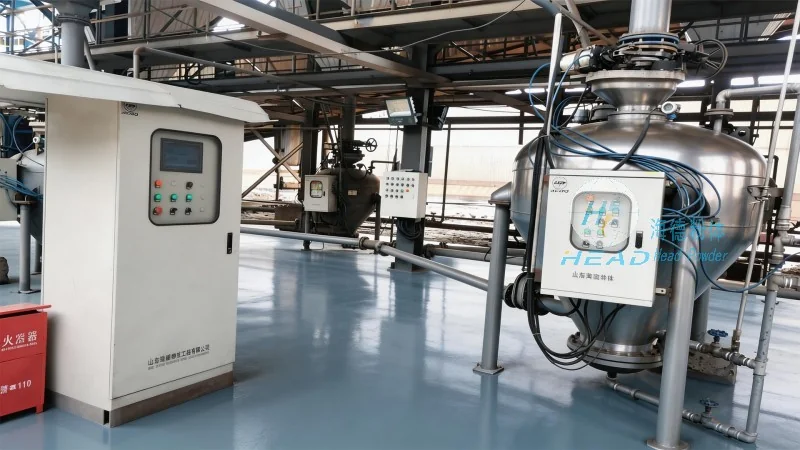
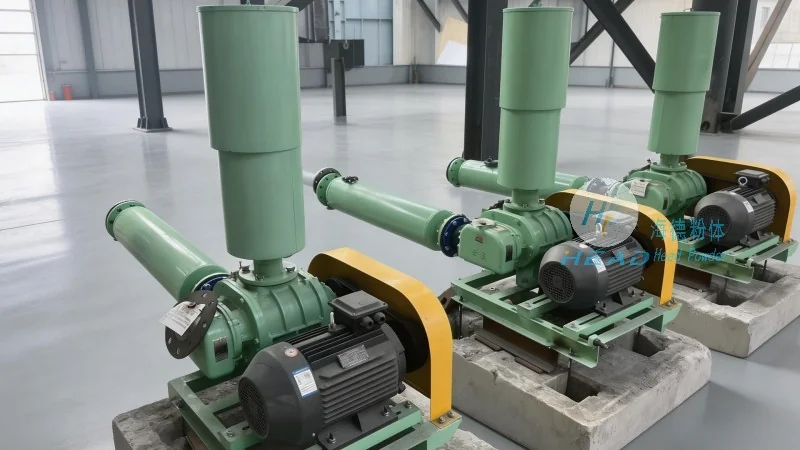
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using a stream of air. In the context of magnesium sulfate, this technology involves the use of compressed air or suction to move the material from a source to a destination. The core principle revolves around creating a flow of air that entrains the magnesium sulfate particles, allowing them to be carried through the pipeline. There are two primary types of pneumatic conveying systems: pressure and vacuum. Pressure systems use compressed air to push the material forward, while vacuum systems employ a suction mechanism to draw the material into the pipeline. The choice between these systems depends on factors such as the distance to be covered, the material's properties, and the required flow rate. For magnesium sulfate, which is typically a fine powder or granular material, pressure systems are often preferred due to their ability to handle higher flow rates and longer distances with less pressure drop. The conveying process begins with the material being fed into the conveying line, where it is mixed with the air stream. The air velocity must be sufficient to overcome the gravitational forces acting on the particles and to maintain the material in suspension. This requires careful design of the system, including the selection of appropriate air velocities, pipe diameters, and the use of components like feeders and separators to ensure consistent and efficient transport. The principle of pneumatic conveying for magnesium sulfate also involves considerations of material properties, such as particle size, density, and moisture content. These factors influence the air velocity required for successful conveying and can impact the system's overall efficiency. For example, finer magnesium sulfate particles may require higher air velocities to remain in suspension, while larger particles may need lower velocities to avoid excessive wear on the system components. Additionally, the moisture content of the material can affect its flowability and the risk of caking, which may necessitate adjustments to the conveying system, such as the use of drying equipment or the incorporation of anti-caking agents. The design of a magnesium sulfate pneumatic conveying system must account for these variables to ensure optimal performance and minimize operational issues. The system typically includes components such as a material feeder, a conveying line, a separator, and a receiver. The feeder is responsible for delivering the magnesium sulfate to the conveying line at a consistent rate, while the separator separates the material from the air stream at the end of the line. The receiver collects the material and may include features like a dust collector to prevent environmental contamination. The air stream is managed by a blower or compressor, which provides the necessary pressure or vacuum to drive the conveying process. The selection of these components is critical to the system's effectiveness, as they must be matched to the specific requirements of the magnesium sulfate material being transported. Overall, the principle of pneumatic conveying for magnesium sulfate is based on the efficient use of air to transport the material through a pipeline, with careful consideration of material properties and system design to ensure reliable and efficient operation.
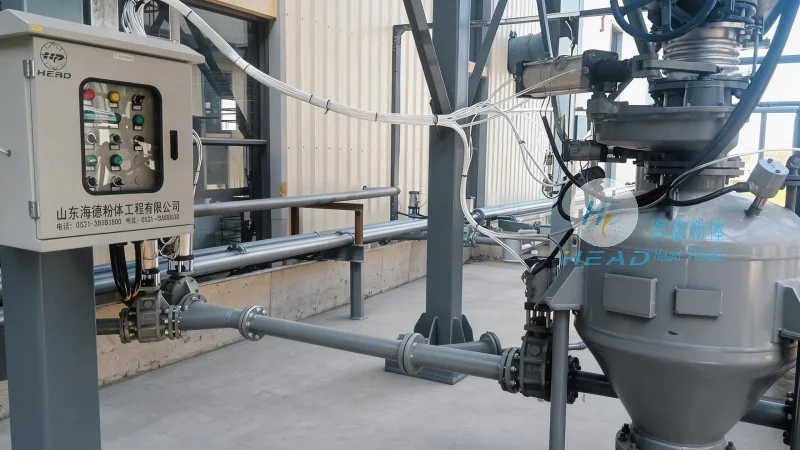
The working scene characteristics of magnesium sulfate pneumatic conveying systems vary depending on the specific industrial application and the environment in which they are used. These characteristics are crucial for understanding how the systems perform in real-world settings and for identifying the most suitable applications for pneumatic conveying technology. One of the primary working scene characteristics is the scale of operation. Pneumatic conveying systems can be designed for small-scale applications, such as laboratory or pilot plant operations, where the material flow rates are low and the distances to be covered are short. In these cases, the system may use a vacuum or low-pressure pressure system, with smaller pipe diameters and simpler components. For large-scale industrial operations, such as in the production of magnesium sulfate from natural sources or in the processing of magnesium sulfate for use in fertilizers or pharmaceuticals, the systems are typically designed for high flow rates and long distances. These large-scale systems often use high-pressure pressure systems with larger pipe diameters and more robust components to handle the increased material volume and pressure requirements. Another important working scene characteristic is the environment in which the system operates. Pneumatic conveying systems for magnesium sulfate are commonly used in indoor or semi-indoor industrial settings, such as factories or processing plants. In these environments, the systems are designed to minimize dust emissions and ensure compliance with environmental regulations. This may involve the use of enclosed conveying lines, dust collection systems, and filtration equipment to prevent the release of magnesium sulfate particles into the air. The working scene may also include considerations of space constraints, as the systems must be installed in the available space without interfering with other equipment or processes. For example, in a compact production facility, the system may use vertical or inclined pipelines to save space, while still maintaining the required air velocity for efficient conveying. The working scene characteristics also include the type of material being transported. Magnesium sulfate can exist in various forms, including fine powders, granules, or crystals, each with different properties that affect the conveying process. Fine powders, for example, are more prone to caking and require higher air velocities to remain in suspension, while granules may be more resistant to caking and can be conveyed at lower velocities. The system design must account for these differences to ensure that the material is transported without blockages or damage. Additionally, the working scene may involve the integration of the pneumatic conveying system with other equipment, such as mixers, crushers, or storage silos. The system must be compatible with these other components to ensure smooth material flow and prevent disruptions in the production process. This integration requires careful planning and coordination to ensure that the conveying system operates in harmony with the rest of the industrial setup. The working scene characteristics also include the operational conditions, such as temperature and humidity, which can affect the performance of the pneumatic conveying system. High temperatures may cause the magnesium sulfate to degrade or change its physical properties, while high humidity may lead to moisture absorption and caking. The system must be designed to handle these conditions, possibly through the use of temperature control or moisture removal equipment. Overall, the key working scene characteristics of magnesium sulfate pneumatic conveying systems are determined by the specific industrial application, the material properties, and the environmental and operational constraints. By understanding these characteristics, industrial operators can select and implement the most appropriate pneumatic conveying system to meet their material transport needs efficiently and reliably.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier of pneumatic conveying systems and related equipment. The company is headquartered in Shandong, China, and has established itself as a leading provider of industrial material handling solutions. HeadPowder specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to the specific needs of various industries, including chemical, pharmaceutical, food, and mining. The company's products are known for their high quality, reliability, and efficiency, and are widely used in the transportation of bulk materials such as magnesium sulfate, powders, and granules. HeadPowder's team of experienced engineers and technicians is dedicated to providing innovative solutions that meet the evolving demands of the industrial sector. The company adheres to strict quality control standards and uses advanced manufacturing techniques to ensure that its products meet or exceed industry specifications. HeadPowder also offers comprehensive after-sales services, including installation, maintenance, and technical support, to ensure that its customers can operate their pneumatic conveying systems effectively and efficiently. With a strong commitment to customer satisfaction and technological advancement, HeadPowder continues to be a trusted partner for industrial material handling needs. The company's presence in Shandong, China, allows it to leverage local resources and expertise while serving clients globally. HeadPowder's focus on pneumatic conveying systems for magnesium sulfate and other materials reflects its expertise in the field and its ability to deliver tailored solutions that address the unique challenges of each application. By combining technical knowledge with practical experience, HeadPowder provides reliable and efficient material transport solutions that contribute to the success of its clients' operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top