HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dust-free automatic powder pneumatic conveying systems. These systems are engineered to handle various powder materials with precision and efficiency, ensuring minimal contamination and optimal performance in industrial applications.
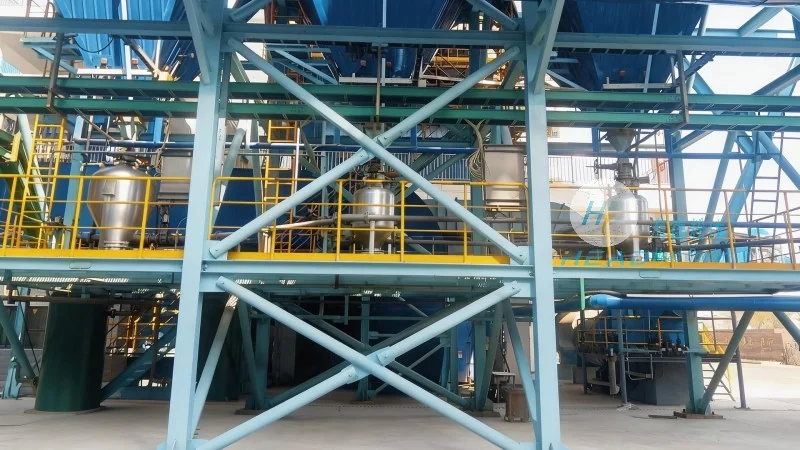
The fundamental principle of a dust-free automatic powder pneumatic conveying system lies in the use of compressed air to transport powder materials through a sealed pipeline network. Unlike traditional methods that rely on gravity or mechanical conveyors, pneumatic systems offer a more flexible and controlled approach to material handling. The system typically consists of a blower, a hopper for material storage, a conveying line, and a discharge point. Compressed air is introduced into the hopper, creating a low-pressure zone that draws the powder into the pipeline. As the air flows through the system, it carries the powder particles, maintaining a consistent flow rate and preventing dust dispersion. This method ensures that the powder remains contained within the system, reducing environmental contamination and improving workplace safety.
HeadPowder's dust-free automatic powder pneumatic conveying systems are equipped with several advanced features that enhance their performance and reliability. One of the primary advantages is the sealed, airtight design, which eliminates the risk of dust leakage and cross-contamination. This is particularly critical in industries such as pharmaceuticals, food processing, and chemical manufacturing, where product purity and regulatory compliance are paramount. The systems also incorporate adjustable air pressure and flow rate controls, allowing operators to customize the conveying process based on the specific characteristics of the powder being handled. Additionally, the use of high-quality materials, such as stainless steel for the pipeline and components, ensures durability and resistance to corrosion, extending the system's service life.
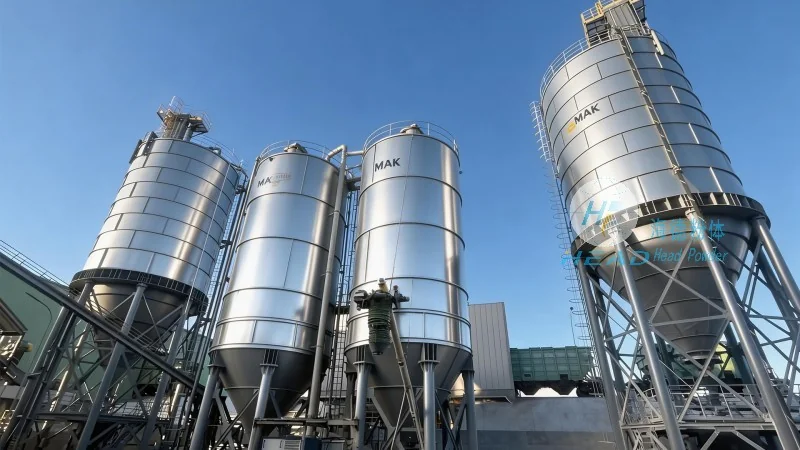
The versatility of dust-free automatic powder pneumatic conveying systems makes them suitable for a wide range of industrial applications. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with strict purity requirements, ensuring that the final product meets regulatory standards. In the food processing sector, they are employed to handle powdered ingredients like sugar, flour, and spices, maintaining hygiene and preventing contamination from external sources. The chemical industry also benefits from these systems, as they can handle corrosive or hazardous powders while protecting the environment and personnel. Furthermore, in the agricultural sector, pneumatic conveyors are used to transport fertilizers and other agricultural powders, improving efficiency and reducing handling time. Each application leverages the system's ability to maintain a dust-free environment and ensure precise material control.
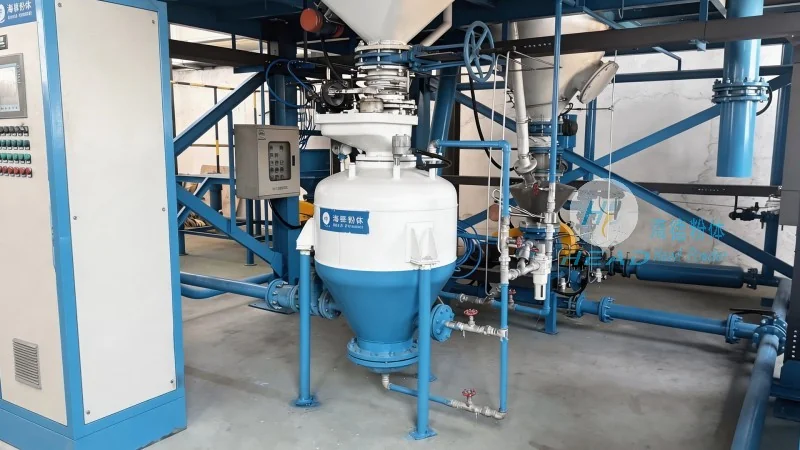
Operational efficiency is a key factor in the success of dust-free automatic powder pneumatic conveying systems. The systems are designed to minimize downtime and maximize throughput, with features such as automatic cleaning cycles and real-time monitoring of air pressure and flow rates. These capabilities allow for proactive maintenance, reducing the risk of system failures and ensuring consistent performance. Regular maintenance, including filter replacement and component inspection, is essential to maintain the system's efficiency and longevity. HeadPowder provides comprehensive maintenance services and spare parts support to ensure that customers can keep their systems running smoothly. The company's expertise in pneumatic conveying technology ensures that customers receive tailored solutions that meet their specific operational needs.
HeadPowder's dust-free automatic powder pneumatic conveying systems represent a significant advancement in material handling technology. By combining advanced engineering with rigorous quality control, these systems offer a reliable and efficient solution for industries requiring precise and contamination-free powder transport. With a strong presence in Shandong, China, HeadPowder continues to innovate and provide customized solutions that meet the evolving needs of its global customer base. The company's commitment to excellence and customer satisfaction ensures that its products remain at the forefront of the industry, delivering value and performance in diverse industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top