HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced material conveying systems tailored for recycled powder applications. This article delves into the core principles of their conveying equipment and highlights the key working scene characteristics that make these systems effective in industrial settings.
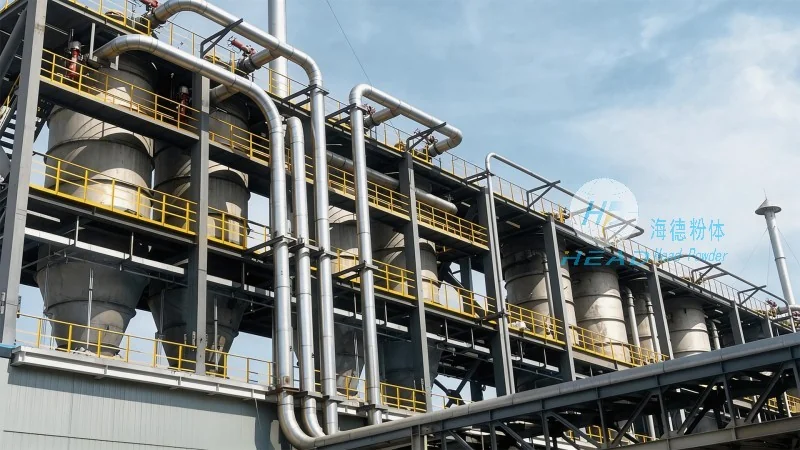
The fundamental principle behind HeadPowder's recycled powder material conveying systems revolves around efficient, low-loss transportation of fine powders. These systems are engineered to handle materials such as recycled powder, which often presents challenges like static electricity, dust explosion risks, and the need for gentle handling to prevent product degradation. The equipment typically incorporates components like screw conveyors, pneumatic conveyors, or a combination of both, depending on the specific material properties and process requirements. The screw conveyor, for instance, uses a rotating helical screw to move material along a closed tube, ensuring consistent flow and minimal product degradation. Pneumatic conveyors, on the other hand, utilize air pressure to transport powders through a pipeline, offering flexibility in layout and the ability to handle materials with higher moisture content or larger particle sizes. The integration of these technologies allows for a customized solution that optimizes both efficiency and safety.
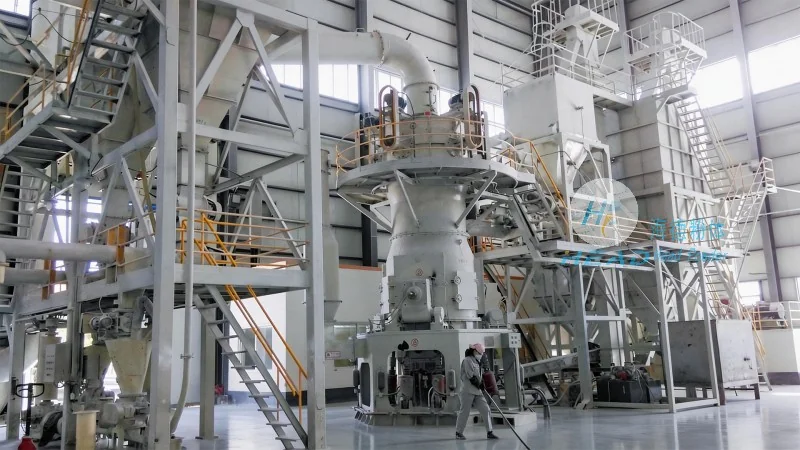
HeadPowder's recycled powder conveying systems are designed to operate effectively in diverse industrial environments, each with unique characteristics that influence system performance. One of the primary working scene characteristics is the need for dust control and explosion prevention. In many recycling facilities, the presence of fine powders poses a significant fire and explosion risk. Therefore, the conveying equipment is equipped with features such as explosion-proof motors, sealed housing, and anti-static measures to mitigate these hazards. This ensures compliance with safety regulations and protects personnel and equipment. Another critical characteristic is the requirement for gentle material handling. Recycled powders, especially those derived from post-consumer waste, may contain contaminants or be more sensitive to mechanical stress. The systems are designed with smooth surfaces and low shear components to minimize product damage, preserving the quality of the recycled material for subsequent processing steps. Additionally, the systems are built for durability and ease of maintenance. Heavy-duty construction and accessible components allow for quick repairs and cleaning, reducing downtime and operational costs. The modular design of the equipment also enables easy integration into existing production lines, making it a versatile solution for various industrial applications.
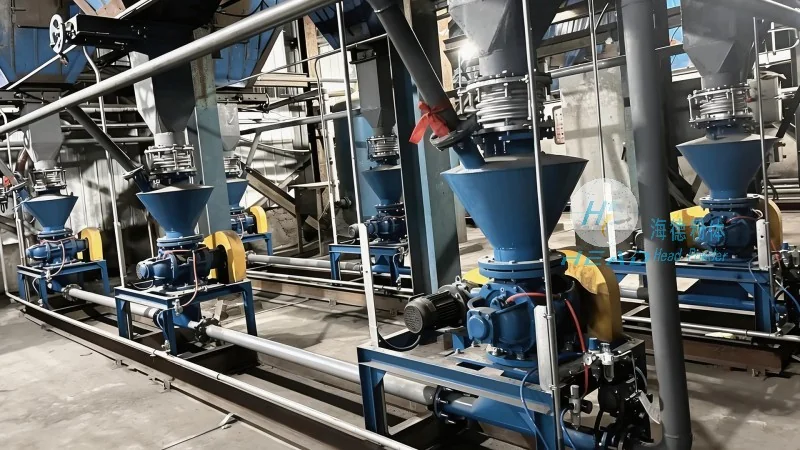
The working scene characteristics of HeadPowder's recycled powder conveying systems are directly linked to their application scenarios. These systems are commonly used in industries such as plastic recycling, metal recycling, and waste management, where the efficient transport of recycled powders is essential for maintaining production throughput. In plastic recycling plants, for example, the system can convey recycled plastic pellets from storage silos to processing machines, ensuring a continuous supply of material. The gentle handling feature is particularly important here, as the pellets need to be preserved in their original form to avoid degradation during transport. In metal recycling facilities, the equipment transports recycled metal powders from collection points to smelting or sintering processes. The dust control and explosion prevention features are critical in these environments, as metal powders can be highly combustible. The operational efficiency of the system is enhanced by its ability to handle high volumes of material with minimal energy consumption. The screw and pneumatic components are optimized for low power usage while maintaining high throughput, contributing to cost savings and environmental sustainability. Furthermore, the systems are designed for scalability, allowing them to be adapted to different production scales, from small-scale recycling operations to large industrial facilities. This flexibility makes them suitable for a wide range of applications, from local recycling plants to global manufacturing facilities.
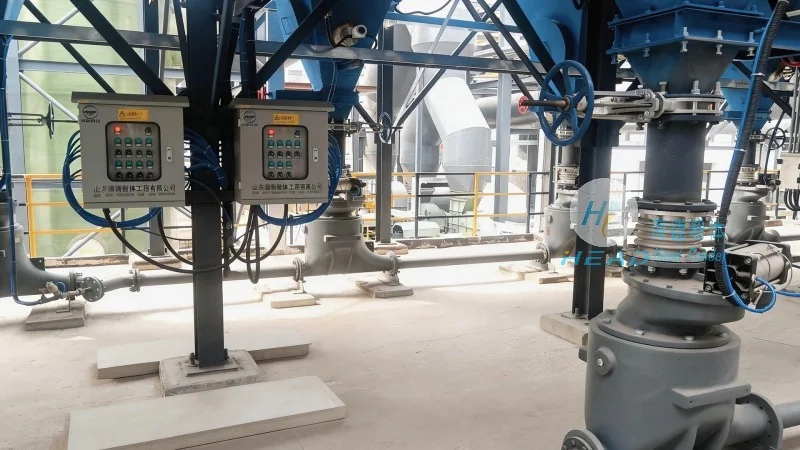
HeadPowder's recycled powder material conveying systems exemplify the company's commitment to providing innovative, reliable, and safe solutions for industrial material handling. By understanding the core principles of efficient powder transport and addressing the unique working scene characteristics of recycled materials, these systems offer significant advantages in terms of operational efficiency, product quality, and safety. Based in Shandong, China, HeadPowder leverages its expertise in engineering and manufacturing to deliver customized solutions that meet the specific needs of each client. The company's focus on durability, maintenance ease, and environmental considerations ensures that its conveying equipment not only performs effectively but also contributes to the long-term success of industrial operations. As the demand for sustainable recycling practices grows, the importance of efficient material conveying systems becomes increasingly evident, and HeadPowder's products are well-positioned to meet these evolving industry needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top