Silo material handling equipment plays a crucial role in modern industrial operations, particularly in sectors that rely on bulk material storage and transportation. These systems are designed to efficiently move materials such as grains, powders, and other bulk commodities from storage silos to processing or distribution points. The effectiveness of these systems depends on a combination of mechanical design, operational logic, and the specific requirements of the industrial environment. Understanding the underlying principles and the diverse working scenarios where these devices are applied is essential for optimizing material flow and enhancing overall operational efficiency.
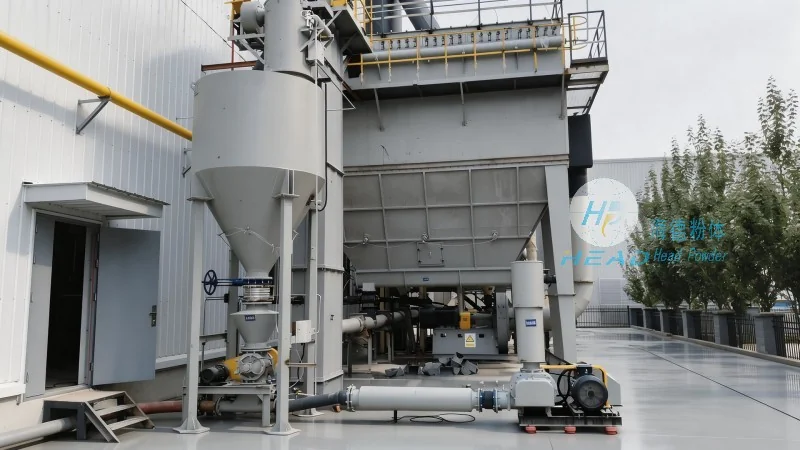
The fundamental principle of silo material handling equipment revolves around the use of mechanical components to manipulate bulk materials within a silo structure. Key components typically include hoppers, conveyors, and control systems. The hoppers serve as the initial point of material collection, where bulk materials are deposited from external sources or from other processing stages. From the hopper, materials are then transferred to the conveyor system, which can be either a screw conveyor, belt conveyor, or pneumatic conveyor, depending on the material characteristics and the desired transport method. The control system, often integrated with sensors and automation technology, regulates the flow rate, direction, and timing of material movement, ensuring precise and safe operation.
For example, in a grain storage facility, the equipment might start with a large hopper that collects harvested grains from a combine harvester or a grain cart. The hopper then feeds a screw conveyor that transports the grains to a processing unit or a loading area. The control system monitors the hopper level and adjusts the conveyor speed to prevent overfilling or underfilling, maintaining a steady flow of material. This principle of material transfer from a storage vessel to a transport system is consistent across various applications, though the specific components and configurations may vary based on the material's properties and the operational scale.
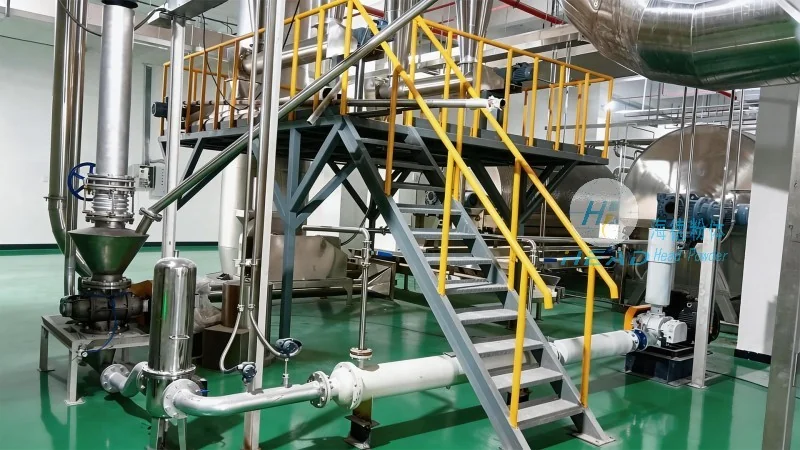
The working scenarios where silo material handling equipment is deployed vary widely, reflecting the diverse needs of different industries. One common scenario is in agricultural processing facilities, where these systems are used to move harvested crops from storage silos to milling or packaging operations. In such settings, the equipment must handle large volumes of granular materials, often with varying moisture content and particle sizes, requiring robust and adaptable design features. The working environment is typically characterized by high throughput requirements and the need for continuous operation, which demands reliable and low-maintenance equipment.
In the chemical and pharmaceutical industries, silo material handling equipment is used to transport powders and granules that require strict contamination control and precise dosing. Here, the equipment may incorporate sanitary design elements, such as stainless steel components and sealed conveyor systems, to prevent material contamination and ensure product purity. The working scenario is often characterized by the need for accurate measurement and control, as these industries rely on consistent material quantities for manufacturing processes. Additionally, the equipment may be integrated with batching systems to control the amount of material transferred at each step, ensuring compliance with production specifications.
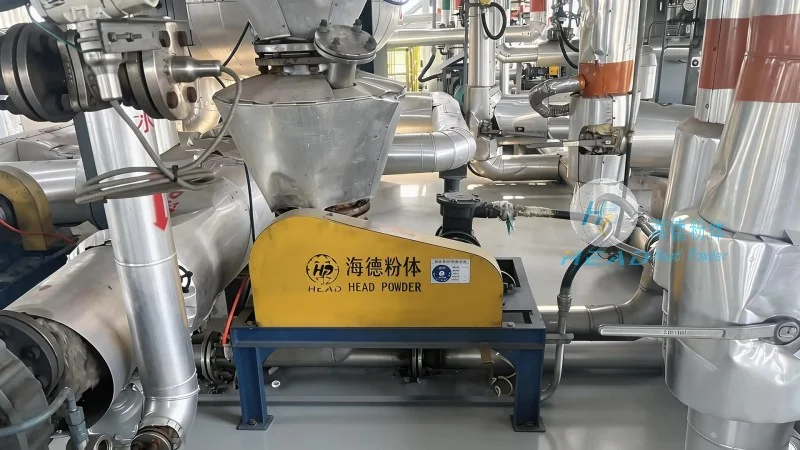
In the mining and minerals processing sector, silo material handling equipment is used to transport raw ores and processed minerals from storage silos to crushing or grinding units. The working scenario in this industry is often characterized by the handling of abrasive and heavy materials, which places significant stress on the equipment components. The equipment must be designed to withstand high impact loads and wear, with features such as reinforced hoppers and durable conveyor belts. The control system in this scenario may also include sensors to monitor material density and flow rate, optimizing the processing efficiency of downstream equipment.
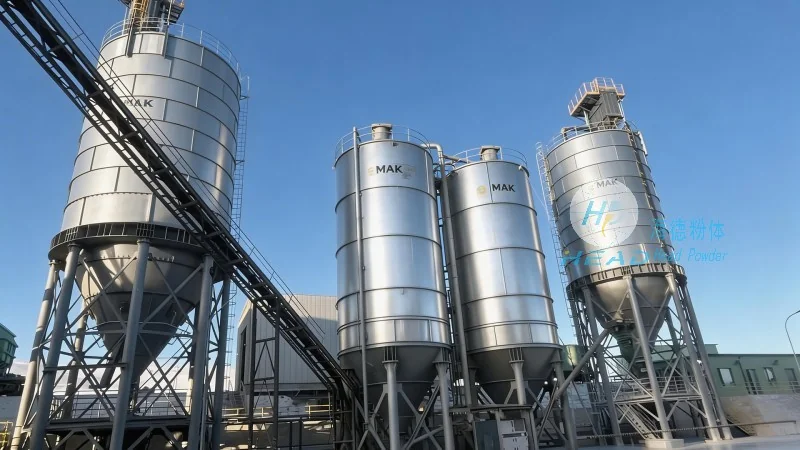
In the food and beverage industry, silo material handling equipment is used to transport ingredients such as flour, sugar, and other dry components from storage silos to production lines. The working scenario here emphasizes hygiene and safety, with equipment constructed from food-grade materials and equipped with cleaning mechanisms. The control system may include features like automatic cleaning cycles and material flow monitoring to ensure compliance with food safety regulations. The equipment is designed to handle materials with varying particle sizes and moisture content, ensuring consistent quality in the final product.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of silo material handling equipment. With a focus on innovation and quality, the company has developed a range of products tailored to meet the diverse needs of industrial sectors. HeadPowder's equipment is designed to enhance operational efficiency, reduce downtime, and ensure safe material handling in various working scenarios. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the bulk material handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top